The core problem factories actually face
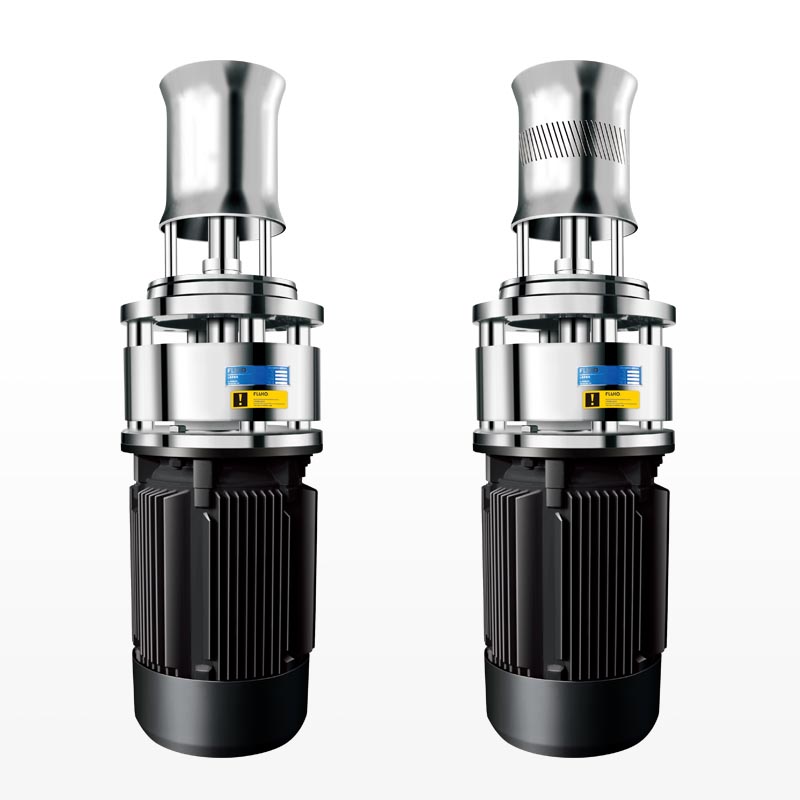
You want uniform particle size, fast throughput, and less downtime, but old gear gives you streaks, long cleaning cycles, and batches that fail QC. Too many teams try to crank up speed and call it fixed—what changes is the approach. Swapping a line or adding pockets of shear often helps, and sometimes the simplest move is integrating an inline high shear mixer right where the feed meets the main stream so you stop creating problems later in the process.
Why standard mixers don’t cut it for modern specs
Traditional agitators mix bulk, but they don’t control droplet or particle distribution at scale. That matters when particle size affects stability, bioavailability, or texture. People assume run time and speed solve everything; they don’t. The mismatch is usually about how and where energy is applied. Too little localized shear leaves agglomerates. Too much upstream turbulence creates entrained air and foaming. Fixing that requires targeted shear and predictable residence time, not brute force.
What really works — proven approaches and a high-level anchor
I’ve spent over a decade helping plants replace guesswork with repeatable setups, and I’ve seen pharma and specialty-chemicals plants in Basel, Switzerland, standardize on point-of-use homogenization to meet tight particle specs. For many of those installs, an inline high shear homogenizer became the predictable element that removed batch-to-batch variation. The lesson: place focused energy where the feed is most variable, measure outcome, and iterate—don’t just add more impeller power to a tank and hope for the best.
Alternatives and common mistakes to avoid
Options include high-torque slow-rotor agitators, ultrasonic processors, static mixers, and rotor-stator in-line units. Each has strengths: ultrasonics for nanoemulsions, static mixers for simple blending, and rotor-stator units for fast droplet break-up. Common mistakes are oversizing equipment (which kills shear intensity), ignoring tip speed, and underestimating sealing and cleanability needs. Another frequent error: moving the homogenizer too far from the feed point—delay kills repeatability.
Practical setup tips you can use tomorrow
Match tip speed to viscosity rather than horsepower. Keep the homogenizer as close to the feed junction as possible. Validate with simple sampling at three points: immediately after the unit, mid-process, and at fill—don’t rely on visual checks. Choose materials and seals that withstand your solvents and CIP cycles. Plan maintenance intervals by cumulative run-hours, not calendar dates; wear predicts performance drift.

Where this leads the operation
Fix the point problems first, validate results, then scale. That disciplined, problem-first method consistently reduces rejects and simplifies validation. For teams looking for that kind of predictable, point-of-use control, the work tends to converge on proven inline solutions like those offered by FLUKO, which integrate shear, cleaning, and serviceability into the run sequence without adding guesswork.