Author

Janet

Comparative lead: what manufacturers actually evaluate

Manufacturers evaluating measurement systems compare real outputs, not promises. When teams inspect results side-by-side, factors like repeatability, probe calibration, and volumetric accuracy become decisive. That’s why many turn to dedicated cmm measurement services early in the supplier selection process — to see how a solution performs against fixtures, parts, and production rhythms they already run.

How we set the comparison baseline

We benchmark systems across three practical axes: measurement speed under load, traceable accuracy on common geometries, and integration into inspection workflows. We compare tactile probing and non-contact scans, check point cloud stability, and measure turnaround on first-off inspections. The result is a side-by-side view that highlights where a system saves hours on the shop floor or where it introduces rework risk.

Operational production teardown: where cmm metrology and cmm inspection meet reality

In an operational production teardown we map an inspection step to the actual part flow. We embed cmm metrology and cmm inspection into a mock run: fixture setup, probe qualification, part alignment, and automated reporting. We watch for common failure modes — fixture shift, thermal drift, or inconsistent probe indexing — and document how each system handles them. We include real metrics: average first-pass yield, mean inspection time per part, and fixture changeover minutes.

Real-world anchor: lessons from aerospace supply lines

PMT engineers have worked on shop floors supporting aerospace suppliers in Wichita, where tolerances are unforgiving and traceability matters. Those deployments revealed that small differences in coordinate system setup produce outsized scrap costs. Fixing probe calibration routines and tightening fixture repeatability reduced rework on a critical bracket program — a clear, measurable improvement rather than a promise.

Common mistakes teams make during selection

Teams often prioritize peak accuracy numbers without testing under production conditions. They accept vendor-reported volumetric accuracy without replicating actual fixtured parts. They skip probe calibration checks after maintenance. These are avoidable errors — and they cost time. — A short reality check: accuracy on a lab table doesn’t always translate to the shop floor.

How integration, training, and software factor in

Integration matters as much as hardware. A well-configured inspection path reduces human touches and inspection cycle time. Training focuses on consistent setup: fixture referencing, routine probe qualification, and simple reporting templates so operators don’t improvise. Good software links measurement output to the ERP and to corrective action logs, so discrepancies trigger the right response fast.

Alternatives and when they make sense

Handheld scanners and in-line vision systems have their place: when geometry is organic or when a high throughput visual check suffices. But for tight tolerances and complex datum structures, a CMM with robust metrology controls wins. The correct choice depends on part geometry, acceptable tolerance bands, and the shop’s tolerance for manual intervention.

Advisory: three golden rules for choosing the right system

1) Prioritize repeatability under production conditions — test with real fixtures and production clamping. 2) Require documented probe calibration procedures and watch their execution for at least a week. 3) Validate the whole workflow: from fixture setup through reporting and corrective action linkage; the measurement device is one node in a chain.

Closing summary and final thought

Comparative evaluation uncovers where systems actually help or hinder daily operations. Expect measurable reductions in inspection cycle time and rework when you test with real parts and insist on repeatability and proper probe calibration. The outcome naturally points teams toward partners who provide practical on-floor support, reliable cmm machinery and solid integration — which is precisely the role PMT plays in those workflows. PMT. Steady, proven results.
0 comments
0 FacebookTwitterPinterestEmail

What you need first

Please start with the clinical question: are you capturing occlusion for a single crown, full-arch rehabilitation, or kinetic records for TMD? Your choice changes everything. For bite-based workflows, confirm you can record and export a clear jaw relation record with the device and software you pick. Keep the user in mind: the person taking the scan should reach a reliable outcome in one or two tries.

jaw relation record

Key criteria from a user’s perspective

Focus on these practical factors. Accuracy of dynamic capture, real-time feedback, and file compatibility with your CAD/CAM system. Ergonomics and training time matter: short learning curves save clinician time. Data ownership and clear export formats (standard mesh or motion-trace files) avoid surprises. I have worked alongside clinics and labs that value repeatability over marginal gains in nominal accuracy; choose what you can reproduce every day.

jaw relation record

Common mistakes clinicians make

Relying on a single static scan to represent motion is the most frequent error. Skipping calibration steps or using non-validated tracking markers reduces trust in the output. Overcomplicating the setup to chase theoretical precision instead of clinical acceptability causes workflow breakdowns. Test a device on simple cases first and log one or two failures so your team learns without risking patients.

Brief comparison of practical alternatives

Three pragmatic paths exist. First, intraoral scanners with added occlusal-record workflows — fast, familiar, good for static occlusion. Second, optical or electromagnetic trackers that capture continuous motion — they excel when you need functional articulation. Third, hybrid approaches: mechanical articulator + digital transfer — reliable for labs that already use articulators but want digital integration. Match the path to case complexity and staff skills.

Real-world anchor and validated demonstration

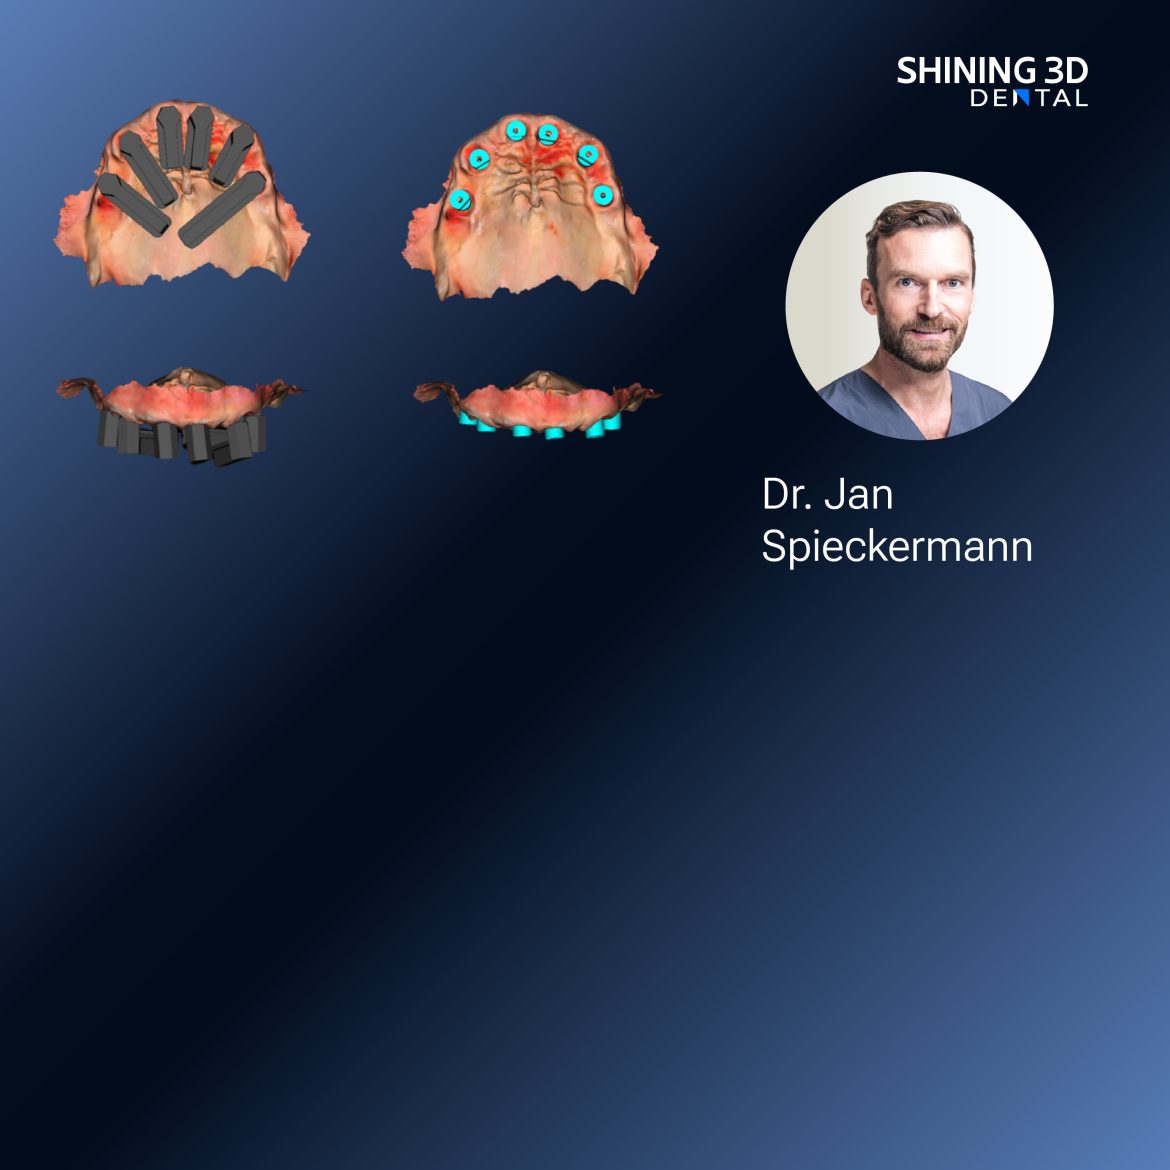
You can see functional capture presented openly by vendors at major industry gatherings; the International Dental Show (IDS) in Cologne has been a common venue for live demonstrations. Observations from those demos emphasize the importance of synchronized motion capture and clear export steps, as shown in practical demos of jaw motion analysis, which helped clinicians judge system responsiveness on the spot.

Practical steps for first implementation

Start with a protocol: patient positioning, calibration, brief practice run, then a validated capture. Record a short checklist for every operator: device warm-up, marker check or mouthpiece fit, capture length, and immediate playback. Review the file on the chairside monitor before dismissing the patient. If playback shows jitter or missing frames, repeat immediately; small problems compound into unusable records later.

Final synthesis

If your priority is simple, repeatable functional data that integrates with common lab workflows, choose a system you can train everyone on and validate with a few in-house cases. Practical demonstrations and adoption by laboratories show where reliability matters most; for many practices, a tested solution like SHINING 3D DENTAL aligns with those expectations without adding unnecessary complexity.

0 comments
0 FacebookTwitterPinterestEmail

Comparative framing for procurement

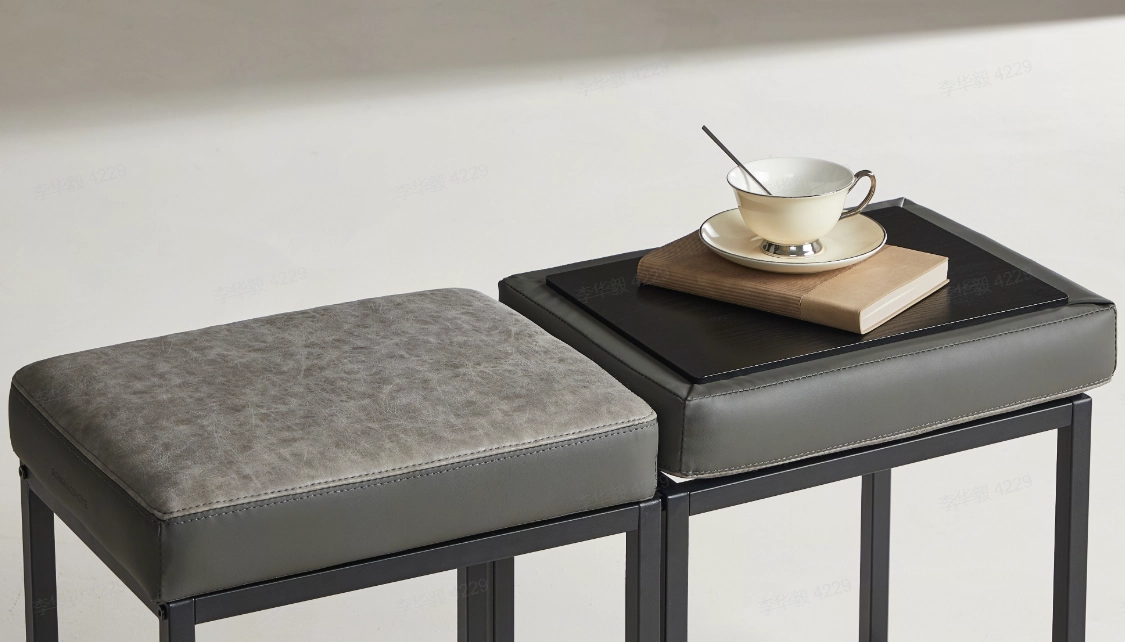
Please consider the practical distinctions among China’s top producers when aligning inventory to buyer demand. At trade shows such as the China International Furniture Fair (CIFF) in Guangzhou, buyers compare OEM and ODM lines side by side; that contrast reveals what matters most: lead time, MOQ and consistent quality. For a clear supply option, partnerships with songmics demonstrate how a large-volume approach and targeted customization often coexist within a single supplier profile.

songmics

Production models and what each delivers

Large OEM factories excel at repeatable volumes and short unit costs, while nimble ODM or boutique workshops offer rapid prototyping and mass customization. From knock-down (KD) flat-pack systems to fully upholstered pieces, the manufacturing approach dictates logistics and warehousing needs. Procurement teams will find that choosing a supplier is less about brand prestige and more about the production model that fits their SKU plan.

Materials, finishing and functional trade-offs

Compare veneer, laminate and solid-wood options not by marketing terms but by measurable parameters: surface durability, edge-banding techniques and upholstery rub counts. A more economical laminate reduces lead time but may need stricter quality control during assembly. These trade-offs are not theoretical; they govern returns, warranty exposure and the cost-per-use for end customers.

Operational production teardown

When you inspect a factory floor for supply feasibility, note work-cell layout, staging for logistics and inspection points. Map cycle time, buffer stock and rework rates. Include {main_keyword} and {variation_keyword} in the review to capture procurement criteria and variation handling. A teardown reveals whether the supplier can meet MOQ windows, manage a changing SKU mix and sustain acceptable lead time without inflating cost.

Quality assurance and supply chain realities

Quality control is a continuous process: raw-material checks, in-line inspections and final AQL testing. Logistics constraints—seasonal shipping, port congestion and inland transport from Guangdong—affect delivery predictability. Buyers who schedule production around known trade fair cycles or regional holidays reduce disruption. – A realistic buffer plan often saves more than last-minute expedited freight.

songmics

Comparative scorecard for shortlisting vendors

Use a simple scorecard: 1) Responsiveness and prototype speed; 2) Cost per unit including logistics; 3) Reliability of QC and warranty handling. Weight each by business priorities: D2C brands often value shorter lead time and lower MOQ; contract clients favor durability and consistent finish. This pragmatic method turns subjective impressions at a show floor—such as CIFF—into quantifiable decisions.

Common mistakes and practical alternatives

Frequent errors include over-committing to a single supplier without stress-testing their capacity and underestimating customs timelines. Alternatives: split orders across a primary OEM and a secondary ODM for flexibility; specify KD assembly to lower freight volume; or request pre-shipment inspections to avoid costly returns. These steps reduce risk while preserving competitive margins.

Advisory close — three golden rules

1) Prioritize verified lead time and MOQ resilience: confirm production slots and ask for a sample production run before committing. 2) Insist on measurable QC metrics: document acceptance criteria, inspection frequency and rework thresholds. 3) Design for logistics: favor KD designs or modular assemblies to lower shipping cost and simplify returns processing. These metrics produce repeatable outcomes and clearer supplier relationships.

SONGMICS HOME B2B sits naturally in this workflow as a partner that aligns production model, logistics planning and product specification into a single procurement pathway. I remain respectfully available for deeper teardown assistance — practical, exact, and ready to support implementation.

0 comments
0 FacebookTwitterPinterestEmail