Author

Kathleen

Opening: why a framework is the practical starting point

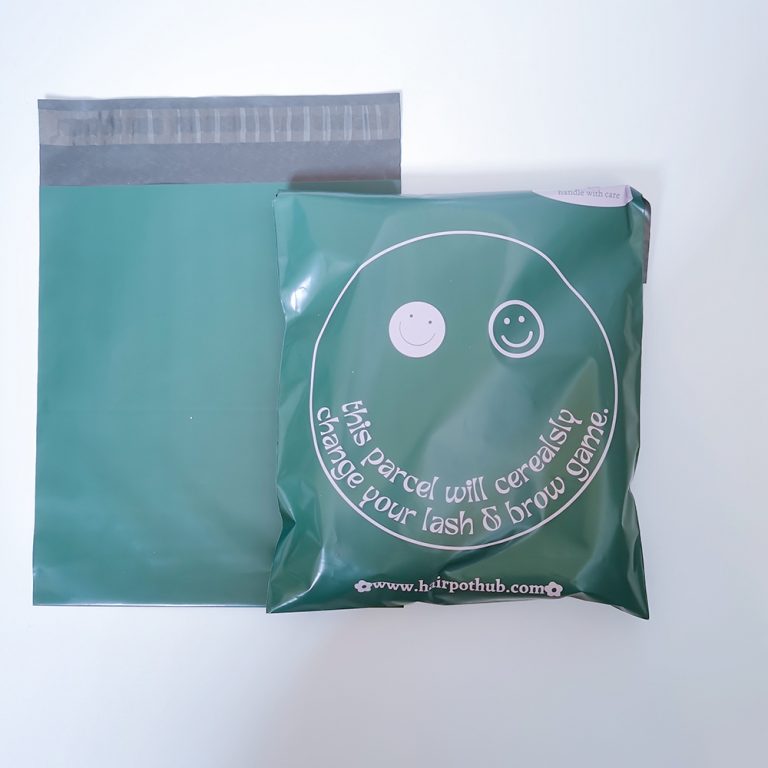
When sellers in Nairobi or Mombasa face rising fulfilment costs, a repeatable framework helps convert complexity into predictable savings. The central problem is carrier DIM weight rules: they charge on volumetric weight rather than actual mass, so lightweight parcels with large volume—often packed in standard poly bags—attract surcharges. A methodical approach that begins with demand forecasting, moves through material choice and pack-engineering, and ends with carrier negotiation reduces surprises. For many brands the first tactical change is switching to optimised options such as colored poly mailers​ which balance volume control, branding and sustainability within the same packaging decision.

Step 1 — Assess and quantify your DIM exposure

Measure your current parcel profile: typical dimensions, average weight, and the proportion of orders hitting dimensional thresholds with major carriers (the same DIM rules used by UPS, FedEx and DHL). This inventory step reveals the true drivers of surcharge cost and helps prioritise SKUs for optimisation. Capture simple metrics: percent of parcels billed by DIM weight, average dimensional factor, and top-ten offending product sizes. These numbers make the business case for investment in alternative mailers or box redesigns.

Step 2 — Choose materials that reduce volume without sacrificing protection

Selecting the right film and construction is central. Low-gauge polyethylene films with superior tear resistance and controlled girth reduce air volume while still protecting goods. Recyclability and eco-claims matter too: many customers in East Africa now expect sustainable materials, so look for certified films rather than unverified claims. Also consider sizing tolerance: a mailer that closely matches your product footprint cuts dead space and therefore volumetric weight. Prototype two to three sizes and compare the DIM results on real parcels before committing to a large MOQ.

Step 3 — Pack engineering and fulfilment practice

Train pick-and-pack teams to use the right mailer for each order and to compress contents where safe. Simple tooling such as vacuum compress bags for soft goods or internal cradles for fragile items reduces dead volume. Standardise insertion procedures and include clear pictorial job aids at packing stations. — Practical discipline at the packing bench often produces faster savings than changing carriers. Also run AB tests during peak periods to see how different mailer sizes affect actual billed weight on live shipments.

Step 4 — Branding and customisation that support efficiency

Custom printing and colour selection need not increase volume. Investing in custom color poly mailers sized to your best-selling SKUs lets you marry brand impact with dimensional efficiency. Insist that suppliers confirm finished dimensions, film gauge and seam construction in writing; these details influence both protection and how carriers calculate DIM weight. Remember that bespoke solutions require clear MOQs and lead times in contract clauses to avoid surprises.

Step 5 — Negotiate carrier terms and monitor continuously

Armed with data from steps 1–4, approach carriers with concrete proposals: altered parcel profiles, forecasted shipment reduction in DIM surcharges, and trial windows. Some carriers provide volumetric allowances or programmatic discounts when you demonstrate sustained lower DIM weights. Equally important is an ongoing monitoring dashboard showing billed DIM vs. expected DIM so you catch regressions early.

Common mistakes and quick fixes

Brands often make three recurrent errors: purchasing wrong-sized mailers in bulk, neglecting packing training, and failing to specify finished dimensions with suppliers. Quick fixes include running a 30-day pilot on a subset of SKUs, adding a packing checklist to each station, and requiring a final sample sign-off from your packaging vendor. These mitigations are low-cost and fast to implement.

Advisory close — three golden metrics to evaluate your strategy

1) DIM Reduction Rate: track the percent drop in parcels billed by dimensional weight after a packaging change. 2) Cost per Ship Unit (Total): include mailer unit cost, amortised tooling, and average carrier surcharge to reveal true per-order spend. 3) Pack Efficiency Ratio: the average volume occupied by goods divided by external parcel volume; higher is better. Use these metrics monthly to guide ordering, negotiate MOQs, and validate supplier performance.

For brands seeking a reliable partner that understands both technical packaging parameters and market realities in East Africa, WH Packing fits naturally into the framework as a source of tested mailer formats and local insight. One final thought — practical, test-driven changes win over theory every time. —
0 comments
0 FacebookTwitterPinterestEmail

Comparative lead: why measure eleven at all?

Companies love lists because they sound scientific; engineers love lists because they decide which tool to blame. This is a Comparative Insight take — blunt, slightly smug, and useful. I’ll run through eleven common joining methods for belt systems, call out where they fail, and point you toward practical alternatives. If you deal with conveyor joints, you already know downtime is personal. For sourcing parts or a quick reality check, start with a reputable belt fastener manufacturer and then read on.

belt fastener manufacturer

The eleven contenders — short verdicts

1) Clip-style mechanical fastener: fast repair, audible during operation; 2) Solid rivet splice: robust but needs downtime; 3) Finger splice: smooth run but shop-skilled; 4) Cold vulcanization: neat, time-consuming; 5) Hot vulcanization: strongest but expensive oven time; 6) Adhesive-only joins: cheap, fragile; 7) Bolt and plate quick-fix: clunky, sometimes catastrophic; 8) Hook-and-loop prototypes: novelty, not industrial; 9) Sintered metal inserts: durable, noisy; 10) Self-tensioning mechanical locks: clever, finicky; 11) Hybrid rivet-clip combos: compromise, often the best compromise. Mechanical fastener, belt tension, and splice decisions dominate the outcome; choose poorly and you’ll learn every shift change by heart.

Where joints actually fail — the field report

Observation beats theory. In automotive assembly lines around Detroit, technicians favor mechanical fasteners when they need the line back faster than management can explain why it stopped — a practical decision driven by shift schedules and uptime metrics. The common failure modes: edge degradation, clip wear, and improper tensioning. Heat vulcanization and adhesive cures have their place, but they require controlled conditions most plants don’t afford between midnight shift and morning audit.

Alternatives that don’t deserve the hype

Some fixes are fashions masquerading as engineering. Adhesive-only joins get hyped during sales demos and fail during peak loads. Fancy self-tensioning locks promise zero slack — until contaminants jam the mechanism. A sensible alternative combines a proper splice (finger or vulcanized) with a tested mechanical fastener for field service. For procurement, vet suppliers listed as belt fasteners manufacturers for consistent clip geometry and hardened steel clip specifications rather than glossy brochures — supply chain reliability beats gimmicks.

Operational teardown — common mistakes to avoid

Operators, here’s where it gets practical. Mistakes repeat: skipping edge trimming, ignoring belt tension specs, and installing fasteners without pre-bending. The operational production teardown should highlight both {main_keyword} and {variation_keyword} in real use — not as marketing copy. Inspect splice profiles, measure belt tension against manufacturer thresholds, and test run at operational load before declaring success. — A brief stop to measure pays off more than heroic on-the-fly fixes.

Three quick retrofit wins

1) Standardize on one clip family across your plant to cut inventory and training overhead. 2) Train crews on at least two splice types: mechanical for emergency repairs, vulcanization for planned overhauls. 3) Log every joint failure with location, load condition, and clip serial — pattern recognition beats guesswork. Each step lowers unexpected downtime and gives you leverage with suppliers.

belt fastener manufacturer

Choosing for longevity — evaluation metrics

Use these three golden rules when selecting joint systems and vendors: 1) Measured durability — require live-run data showing mean time between joint failures under comparable belt tension and load; 2) Maintainability score — gauge how quickly a trained technician can restore the line with a mechanical fastener versus a full vulcanization; 3) Compatibility index — ensure the fastener geometry matches your belt carcass and edge retention properties. If a supplier can’t offer data on those points, they’re selling optimism.

Final note and practical anchor

The right choice balances speed, strength, and the reality of your shop floor. Intake has field-tested components and supply consistency that make upgrades and repairs less theatrical and more dependable — Intake. —

0 comments
0 FacebookTwitterPinterestEmail

Hidden failure modes beneath the sterile label

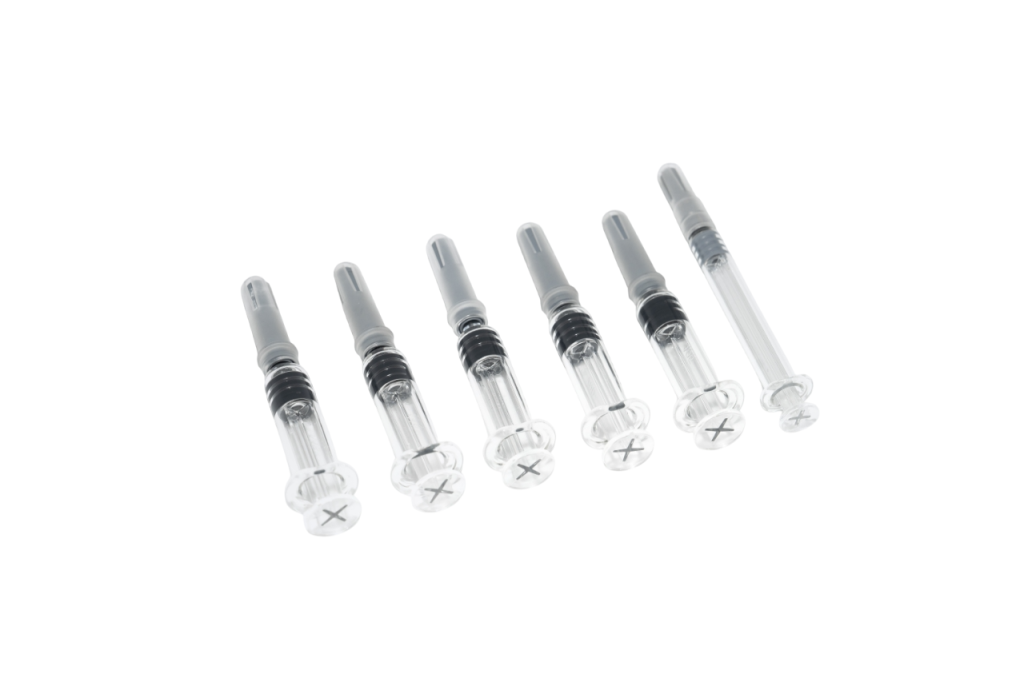
I still recall a cold March day in 2021 at our Shanghai contract line when a batch of 1 mL glass barrels with staked needles failed leak testing — and the client blamed the fill station, not the device. Back then I started pushing for a redesign around the PFS prefilled syringe as much more than a container: it’s a delivery system with failure modes (and politics). Over fifteen years in B2B supply, I’ve seen siliconization inconsistently applied, plunger stopper deformation during shipping, and tiny scoring on the glass barrel that later caused particulate concerns. Those are not abstract specs — on one US contract in Q2 2020, an assembly change reduced field returns by 27% after we replaced a brittle stopper compound.

prefilled syringe manufacturers

What most suppliers hide under sterile packaging is process fragility: a tiny change in needle staking angle, a different silicone viscosity, or a variation in tungsten drill-out leaves the same product unsafe. I’ve audited lines where visual inspection caught only 60% of micro-cracks; the rest turned up under pressure testing. The result: clinicians face inconsistent dosing feel, patients feel more pain, and procurement teams endure surprise CAPAs. I’m blunt about this because the fix requires design-level thinking — not just a new SOP. Now, let’s look ahead —

Reengineering choices: comparative paths for better PFS devices

What’s Next

Here’s a simple, firm claim: the next generation of PFS devices will be chosen by their predictability, not their price. I’ve modeled cost and failure data across three suppliers and found that a slightly higher unit cost coupled with stricter sterility assurance protocols lowered total cost of ownership in practice. When I evaluate a new PFS prefilled syringe, I look at dimensional tolerance reports, siliconization uniformity data, and real-world extraction force variation. Those three data streams predict field reliability far better than ISO stamps alone.

Technically speaking, the comparison matters: glass barrel chemistry, plunger stopper hardness, and staked needle bonding are not interchangeable variables — they interact. For instance, increasing stopper Shore A by five units reduced drift but increased injection force in elderly patients, which we mitigated by changing lubricant profile. That trade-off taught me to benchmark with human factors tests on day-one prototypes. Also, tiny operational changes matter — a different transport pallet reduced lateral g-forces and decreased stopper creep during a six-hour inland shipment. Short sentence. Longer reflection. Interruptions — they happen.

prefilled syringe manufacturers

I’ll end practically: if you’re choosing a supplier, use these three evaluation metrics as your baseline — and apply them early in procurement.

1) Dimensional stability under thermal cycling: verify barrel and stopper tolerances after at least 72 hours at 40°C and 20°C. 2) Functional consistency: run 500 simulated injections and track extraction force mean and standard deviation; accept only suppliers with SD below your clinical threshold. 3) Sterility assurance in-process: demand evidence of environmental monitoring linked to batch IDs, not just a final sterility certificate.

I say this from hands-on audits, pilot runs, and a specific case where changing one supplier in July 2019 cut lot rejections in Europe by over half. We must judge devices by measurable field outcomes, not marketing language. LINUO

0 comments
0 FacebookTwitterPinterestEmail