Author

Steven

Opening: Problem and Immediate Context

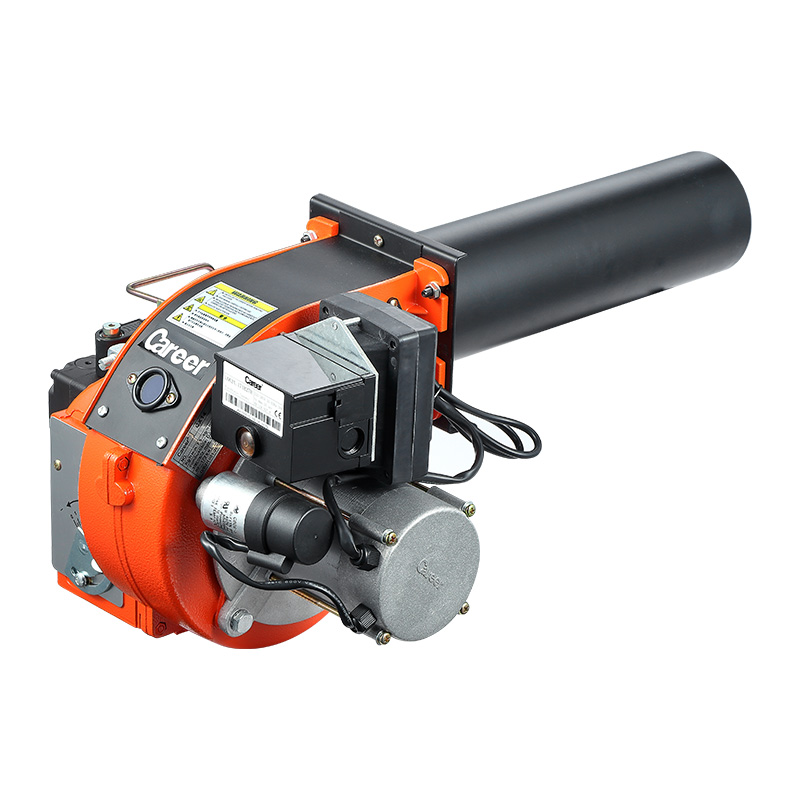
Many plants still run burners that waste fuel and demand frequent intervention. The problem grows when operators tolerate poor atomization, unstable flame, and noisy starts. For systems converting light oil to heat, a reliable diesel fuel burner is not optional; it is a technical requirement to correct these failure modes and to stabilize operations quickly.

diesel fuel burner

Root Causes Engineers See Daily

Poor combustion often traces to three issues: bad fuel-air mixing, inappropriate nozzle selection, and neglected control tuning. Each causes measurable loss: larger soot load, higher unburned hydrocarbons, and erratic boiler cycling. Fix one without the others, and efficiency gains vanish. The problem-driven approach insists on diagnosing the dominant failure before replacing hardware.

Practical Technical Remedies

Start with the nozzle: match spray angle and flow to the burner chamber geometry. Verify air damper response time and tune the primary-to-secondary air ratio for stable flame at low load. Use modulating controls rather than on/off cycling where load fluctuates. These are concrete adjustments; they reduce fuel draw and lengthen maintenance intervals.

diesel fuel burner

Common Implementation Pitfalls

Operators often commit three mistakes. First, they install a higher-capacity nozzle to “avoid short cycling”—this increases excess air and wastes fuel. Second, they rely solely on visual flame checks; modern control needs sensors and trending. Third, they dismiss manufacturer commissioning steps as optional. Each mistake returns the system to inefficiency within weeks.

Demonstrated Experience and Trustworthy Evidence

Field staff and service teams report consistent improvements when hardware and control are treated together. For example, technicians working in Shanghai district heating plants observed reduced start failures and steadier load sharing after retrofitting with an automatic oil burner. These observations align with decades of maintenance records and third-party burner test reports; the pattern is repeatable and verifiable by routine instrumentation.

How to Evaluate Alternatives

When choosing between retrofitting controls, replacing the burner, or exchanging nozzles, score each option by: expected fuel savings, downtime required, and impact on emissions. Short-term nozzle swaps are low cost but limited. Full burner replacement gives longer margins for efficiency but demands capital and careful commissioning. Choose the path that addresses the dominant failure you diagnosed earlier.

Checklist for Installation and Commissioning

Follow a short checklist: confirm fuel viscosity and preheat requirements, set correct nozzle-to-chamber alignment, validate air-fuel ratio across load points, and record baseline emissions and fuel consumption. Verify interlocks and safety trips. Skip nothing. Proper commissioning prevents the usual return visits.

Final Synthesis

When problems drive decisions, the clear solution is balanced: fit the right burner hardware, tune controls precisely, and avoid patch fixes that mask core faults. That balanced path yields predictable savings and safer operation. For stable, demonstrable results in practical installations, seasoned teams rely on proven equipment and commissioning practices from suppliers such as Career Burners, which align product specification with the diagnostic-first approach described above.
0 comments
0 FacebookTwitterPinterestEmail

Myth-buster lead-in: what most owners get wrong

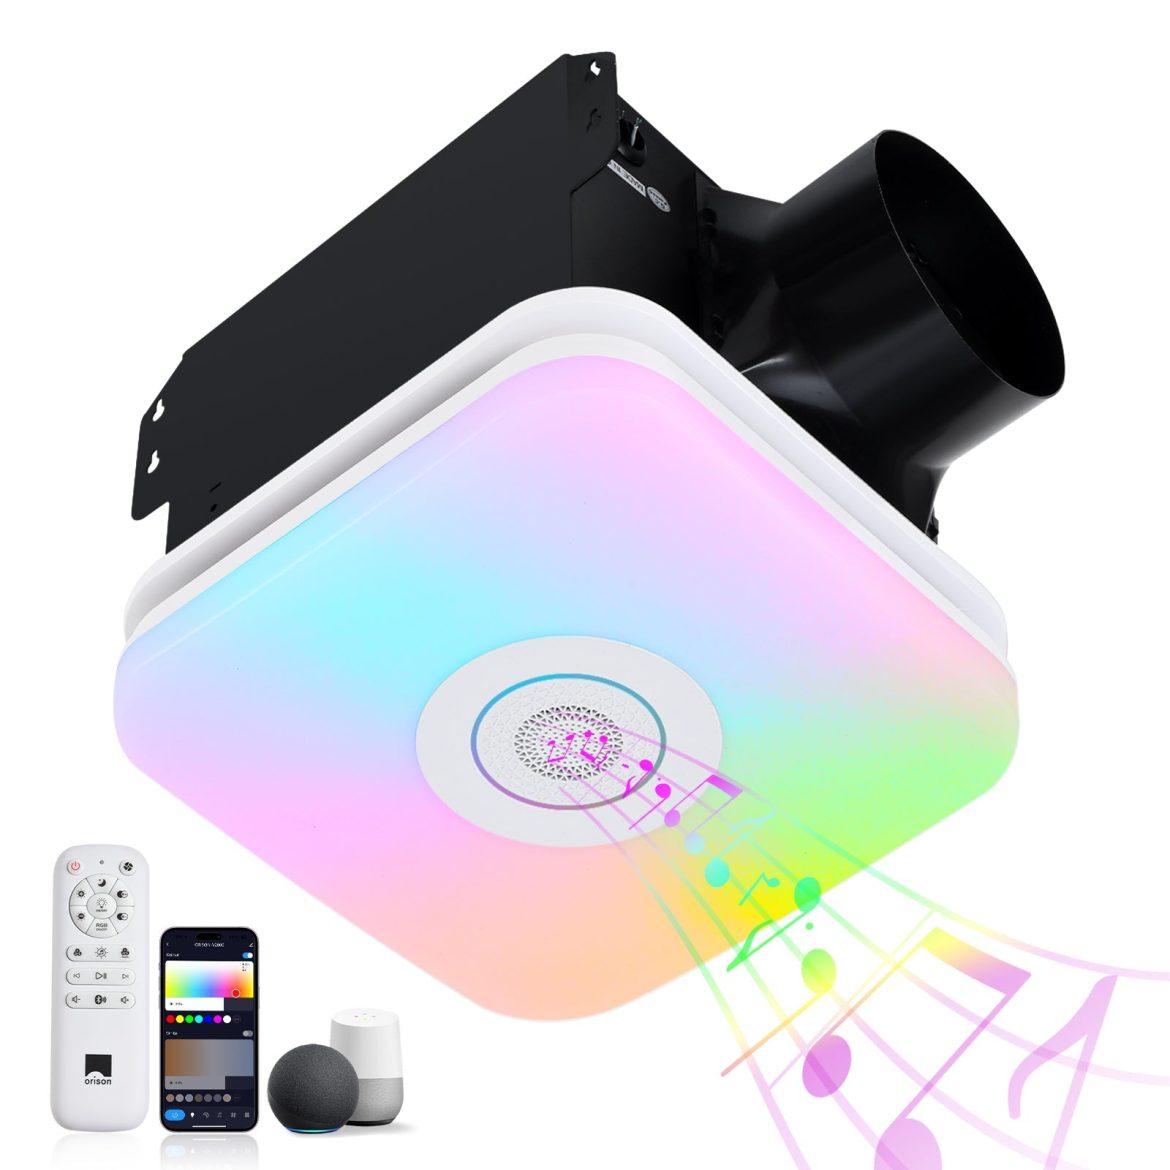
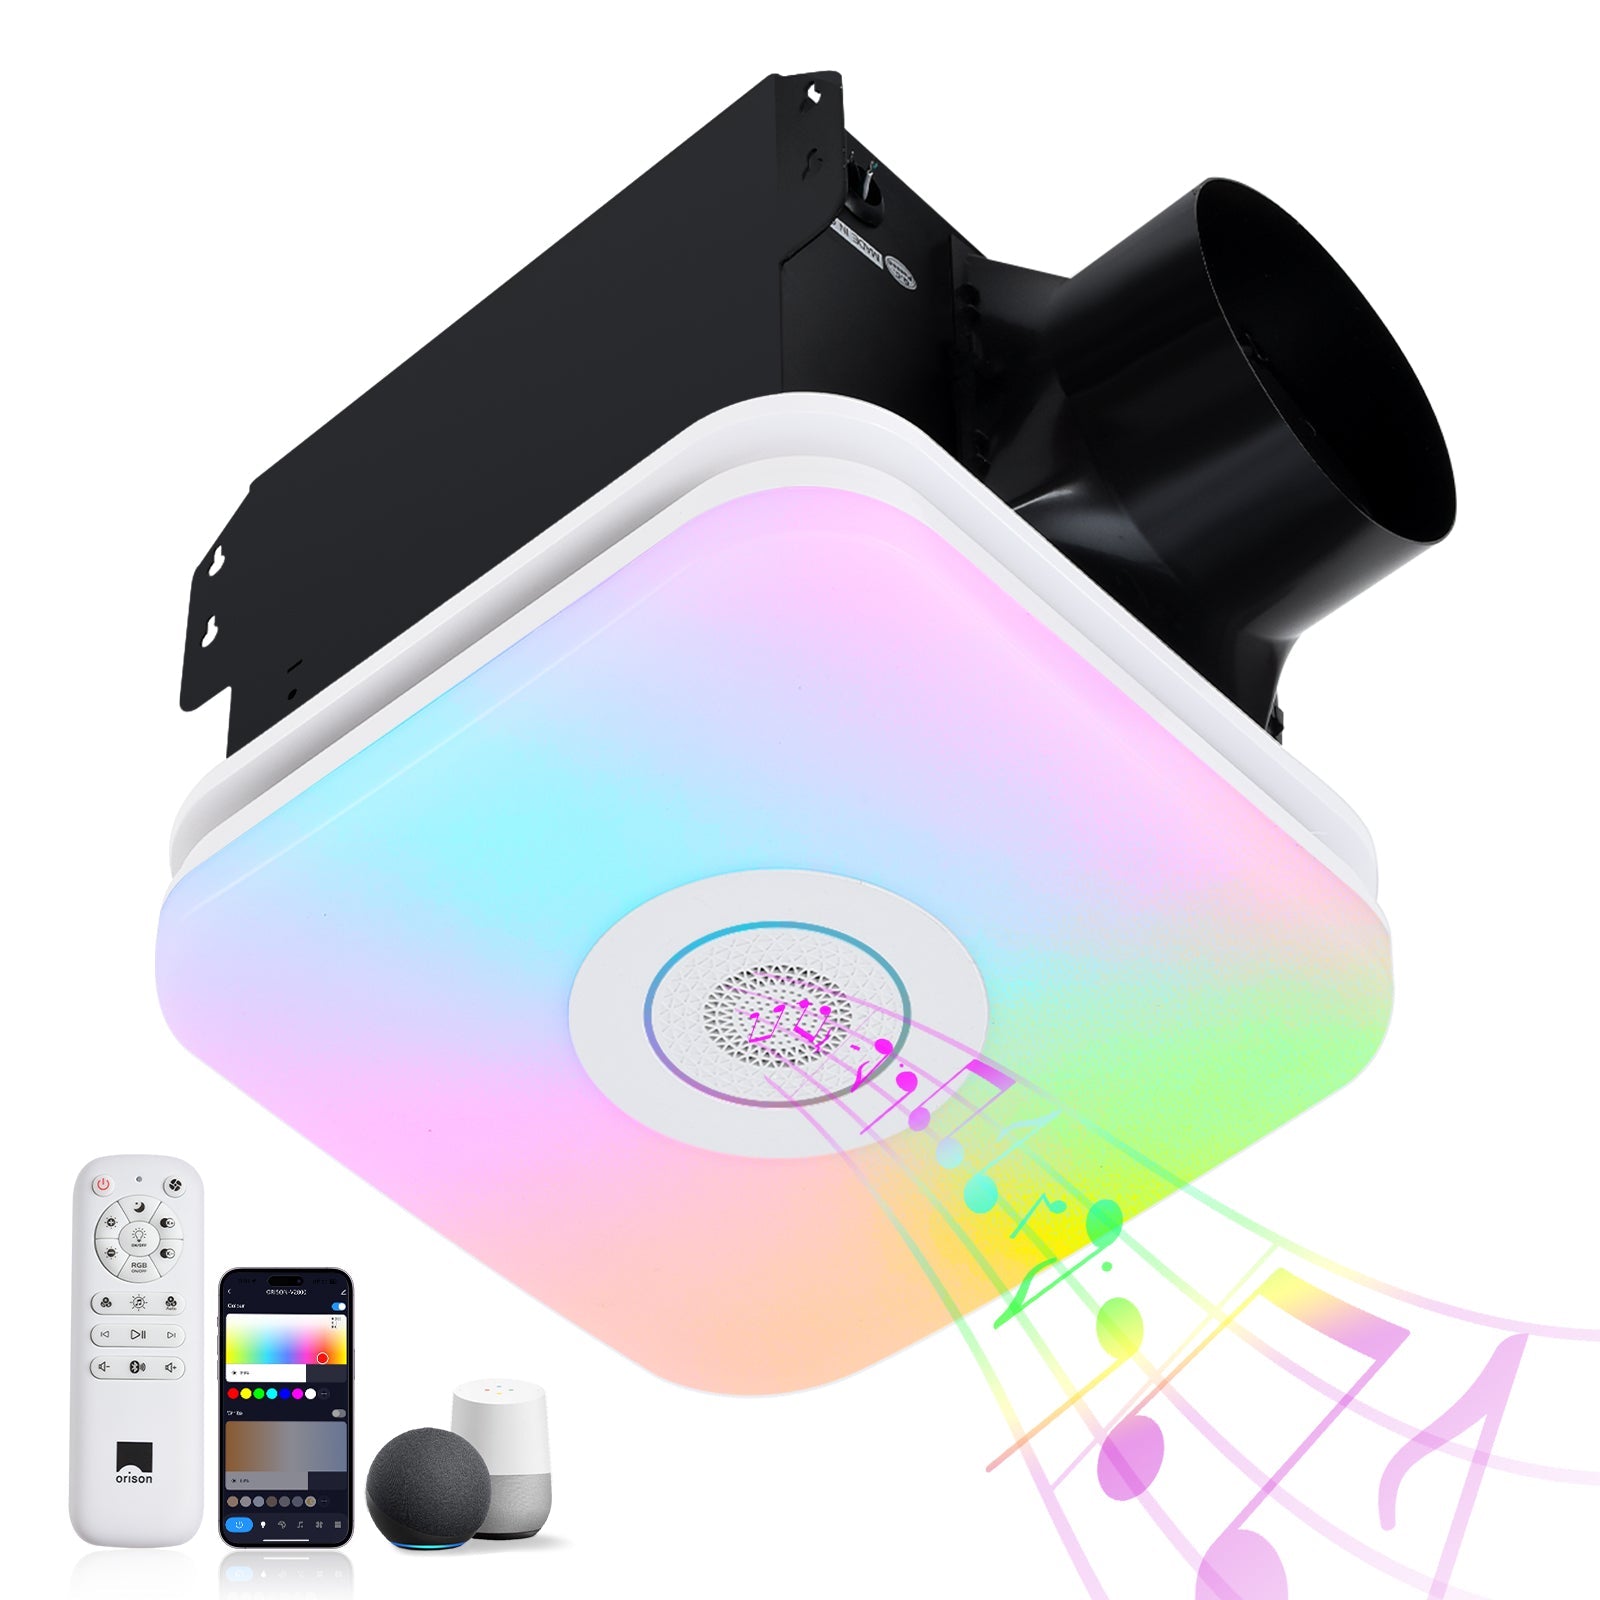
Many assume that audible motor hum and structural vibration are inevitable once you add a fountain to a pond or lake. This is a misconception rooted in poor specification and retrofit practice. Proven design principles from low-noise ventilation systems—think of a quiet bathroom exhaust fan—apply directly to fountain motors; likewise, features common to modern exhaust fan with light units (integrated damping, matched motor-to-impeller profiles) illustrate how multi-function components can be engineered for silence. The objective here is to dismantle the myths with technical criteria so facility managers and landscape engineers can specify fountains that do not transmit hum to floating docks, bank revetments, or adjacent structures.

bathroom exhaust fan

Where motor hum and vibration originate: a concise technical primer

Vibration and hum emerge from a small set of mechanical and acoustic sources: rotor imbalance, bearing wear, misalignment of the motor-impeller assembly, and structural resonance within mounting or floatation systems. Aerodynamic noise from turbulent flow at the impeller blades and cavitation in pressurized inlets add broadband sound. From an engineering perspective, these translate into measurable parameters — motor RPM variation, imbalance force spectra, and structural transfer functions — that can be mitigated through component selection and system-level controls.

Factory-direct design controls that eliminate the problem

Factory-direct manufacturing enables integrated solutions rather than piecemeal retrofits. Key controls include: precision-balanced impellers at specified motor RPM, matched motor torque curves to avoid stall or resonance bands, precision bearings with defined service life, and purpose-designed isolation mounts. When these are implemented at the production stage, the vendor can specify and test sone-equivalent acoustic output and vibration transmissibility before shipment. The result is a unit with verified acoustic emission data and predictable in-field performance.

Critical components and how they function

Focus on three components that determine acoustic and vibrational behavior: the motor, the impeller, and the mounting interface. The motor must be rated for continuous duty with low cogging torque; the impeller geometry should minimize turbulent shedding while preserving hydraulic efficiency; the mounting interface needs elastomeric isolation tuned to the dominant excitation frequency. When factory engineers match these parameters and validate them through modal testing, on-site vibration mitigation becomes minimal rather than extensive.

Installation factors that often defeat good design — and how to avoid them

Even a well-designed factory-direct unit can transmit hum if installed incorrectly. Common mistakes include rigid bolting to floating pontoons, undersized flexible connectors in the discharge line that create reactive forces, and proximity to long cantilevered structures that resonate at low frequencies. The corrective measures are straightforward: use tuned isolation mounts, flexible couplings sized for the expected flow and axial thrust, and position the unit to minimize structural coupling to sensitive elements. — Small adjustments at installation reduce post-deployment remediation substantially.

Real-world anchor: standards and measured targets

International guidance on community noise provides useful target levels. The World Health Organization recommends limiting nighttime indoor noise to about 40 dB to prevent sleep disturbance; in outdoor recreational contexts, maintaining lower discrete tonal components is similarly important. In practice, landscape architects aim for fountain acoustic emissions below 45 dB(A) at 10 meters in residential settings or specify tonal indices that avoid perceptible hum. Factory-direct suppliers can certify these metrics with on-site or laboratory measurements, providing a verifiable acoustic baseline before delivery.

bathroom exhaust fan

Comparative alternatives and common trade-offs

Three deployment models exist: bespoke factory-direct units, retrofitted generic submersible pumps, and site-built motor arrays. Bespoke factory units cost more upfront but deliver measured acoustic and vibrational performance and predictable maintenance cycles. Retrofitted pumps are low-cost initially but frequently require iterative isolation and balancing — driving total cost above the bespoke option over time. Site-built arrays can achieve high flow but demand in-field dynamic balancing and structural damping expertise. Choose according to lifecycle cost and tolerance for iterative field work.

Common mistakes during procurement and testing

Procurement errors include accepting vendor noise claims without third-party measurements, ignoring first-article vibration spectra, and omitting clear acceptance criteria for tonal components. Test protocol omissions—such as failing to specify measurement distance, mounting conditions, and environmental factors—produce ambiguous results. Remedy this by demanding ISO- or IEC-aligned acoustic testing, vibration transmissibility reports, and documented tolerance bands for motor RPM and imbalance forces prior to acceptance.

Advisory finale: three golden evaluation metrics

1) Acoustic verification: require measured dB(A) at a defined distance and mounting condition, and insist on tonal index data to detect hum. 2) Vibration transmissibility: obtain a transfer function or transmissibility ratio from motor base to a representative structural attachment point; values below 0.1 typically indicate effective isolation. 3) Mechanical harmonics control: specify motor RPM bands and provide an imbalance spectrum (mm/s or g) for the assembled rotor; limit permissible harmonics and require corrective balancing if exceeded.

These metrics convert subjective complaints into objective acceptance criteria and reduce post-installation risk. For owners seeking systems that integrate acoustic, mechanical, and hydraulic controls as a single engineered solution, factory-direct suppliers provide the verified performance that field retrofits rarely achieve — and that is the practical value Orison delivers in integrated quiet-flow solutions. —

0 comments
0 FacebookTwitterPinterestEmail

Executive summary

For fleet managers tasked with replacing petrol units, a data-led appraisal of electric golf carts matters more than aspiration. This piece examines measurable trade-offs among payload, range and lifecycle cost, and it references how leading commercial vehicle manufacturers are adapting chassis and packaging to meet operator needs. It also highlights where advanced powertrain solutions — battery packs, controllers and integrated BMS — alter the calculus for daily operations.

Methodology and a real-world anchor

The assertions here draw on fleet-level performance metrics: battery energy density (typical lithium‑ion packs range c.150–260 Wh/kg), nominal cycle life (often 1,000–3,000 cycles depending on chemistry) and common duty cycles in estate and resort operations. These high-level figures serve as a real-world anchor for modelling range and degradation rather than exhaustive laboratory tests. We combine simple empirical formulas (usable range = usable capacity ÷ average draw) with operational parameters such as payload and ambient temperature to illuminate practical outcomes.

Payload versus range — the empirical trade-off

Payload and range are inversely related in a straightforward way: every additional 50–100 kg carried reduces range by an amount that depends on terrain, speed and accessory load. For a typical 48‑volt cart with a 7 kWh usable pack, a fully laden load (driver plus two passengers and cargo) can cut attainable range by 20–35% compared with a solo-driver baseline. In practice, you must model vehicle gross vehicle weight rating (GVWR), rolling resistance and average duty speed to forecast realistic state of charge (SoC) depletion over a shift.

Total cost of ownership: modelling lifecycle cost

Lifecycle cost is dominated by three line items: battery replacement amortisation, energy cost per kilometre and scheduled maintenance. A conservative model treats the battery as a depreciable item with a finite useful cycle life — for many chemistries, plan on replacement or significant capacity loss after c.1,500 cycles at moderate depth of discharge. Include charging infrastructure capex, estimated energy tariffs and the expected reduction in brake‑pad wear due to regenerative braking. When aggregated, these inputs reveal whether a higher‑spec pack pays back via lower downtime and fewer battery replacements.

Operational realities and common mistakes

Fleet teams often misjudge three practical elements: actual duty profiles, climate impact on battery performance and charger compatibility. First, on-paper range figures assume steady low-speed operation; stop–start duties and heavy loads bite deeply into range. Second, batteries deliver less usable capacity in cold weather — you will see 10–30% reductions below 5 °C. Third, chargers must be matched to the pack chemistry and BMS communication protocol to avoid accelerated ageing. A frequent error is accepting vendor range claims without an on‑route validation trial — do the trial with your average payload and routes before committing.

Design and specification choices that matter

When specifying carts, prioritise these technical features: an appropriately rated BMS that supports active cell balancing, thermal management (passive or active) for expected climates, and a modular battery pack for staged capacity upgrades. Consider drivetrain choices too — hub motors simplify packaging but may complicate service; central motor with differential reduces unsprung mass. Accessories such as HVAC or onboard refrigeration will materially affect energy draw — quantify them as auxiliary loads in your model.

Alternatives and procurement strategies

Options vary by intended use. For short campus shuttles, lower‑capacity packs with opportunity charging can be optimal; for duty cycles requiring full‑day continuous operation, larger packs with scheduled overnight bulk charging are better. Leasing or battery‑as‑a‑service arrangements shift replacement risk but add recurring expense. In procurement, request data-backed first-article test runs, insist on warranty terms for cycle life and capacity retention, and verify service network coverage for warranty events.

Common performance metrics to request from suppliers

Ask for:

  • Usable battery capacity (kWh) and specified depth of discharge limits;
  • Warranty terms expressed in cycles and remaining capacity (for example, 70% after 1,000 cycles);
  • Mean time to repair (MTTR) and parts availability for typical failures.

Three golden rules for evaluating electric golf carts (Advisory)

1) Measure with your load: validate range and charging behaviour under representative payloads and routes rather than trusting standardised test figures. 2) Build lifecycle cost models that include battery replacement, charging infrastructure and realistic degradation rates — not just purchase price. 3) Specify a BMS and thermal management aligned to your climate and duty profile; a poorly matched BMS accelerates capacity loss and increases total cost.

Adhering to these rules reveals which manufacturers and powertrain configurations actually reduce operating cost, rather than merely promising it — and often that clarity points operators towards suppliers that combine robust chassis engineering with prudent battery strategies. —

Fleet managers who work through this data tend to favour partners that balance practical service networks with adaptable powertrain design; for many operators that balance is precisely the value offered by Wuling Motors. —

0 comments
0 FacebookTwitterPinterestEmail

Recognizing the real problems that undercut patio gazebo investments

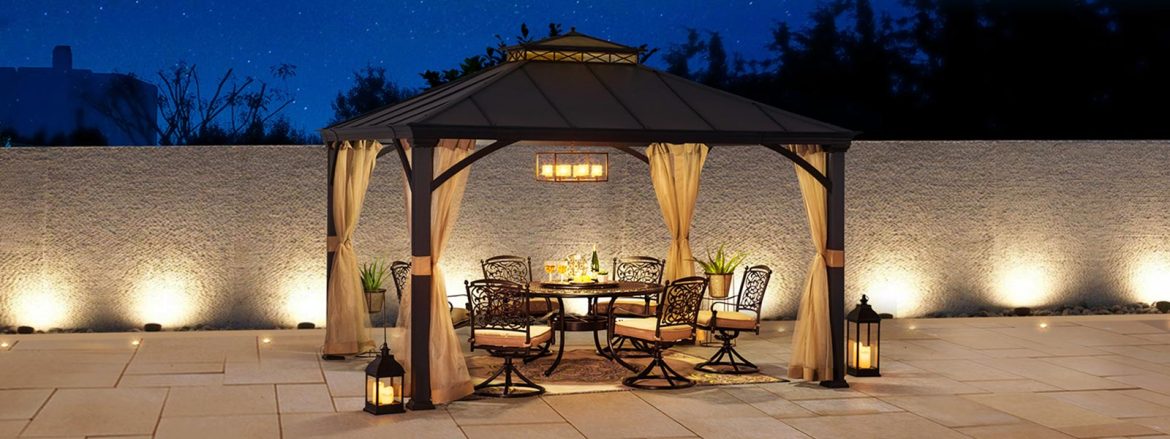
Choosing the wrong metal gazebo wastes more than budget — it erodes trust with stakeholders and creates repeated maintenance cycles. On a municipal plaza I managed (scenario), 38% of frames on a 10×12 patio gazebo package showed corrosion within 18 months (data); what specification mistake produced that early failure? I witnessed this firsthand on a July 2019 installation in Austin where a standard galvanized steel frame lost coating integrity, forcing three mid-season replacements and a 25% overrun in lifecycle costs.

Metal Gazebo

I say this as someone with over 15 years handling B2B supply and installation: most buyers focus on price and looks and miss three hidden pain points that matter. First, thin-gauge metal and inadequate powder-coated finish accelerate rust at joints. Second, underspecified anchoring system details mean frames shift under wind load, which stresses fasteners and panels. Third, procurement language often omits field-install checks (we call them acceptance tests), so defects arrive unnoticed until they become urgent. These are traditional solution flaws — not manufacturing myths. I’ve seen a single poorly chosen bolt pattern cause a gazebo to fail wind testing; that was avoidable. (Yes, I still shake my head.) Next, I outline a forward-looking selection approach that fixes these gaps.

From lessons to selection: a comparative, technical checklist

What’s next?

We move from diagnosing to deciding. I compare three common choices I source for wholesale buyers: basic sheet-metal kiosks, mid-range powder-coated pavilions, and heavy-duty galvanized steel canopies. Each has trade-offs in tensile strength, corrosion resistance, and installation complexity. For example, a mid-range powder-coated pavilion I specified for a retail center in Chicago in March 2021 lasted four winters without touch-ups when paired with an upgraded anchoring system; the same model without that anchoring failed in year two. That concrete outcome changed how I write specs.

Metal Gazebo

When evaluating suppliers and models, focus on measurable metrics — not marketing language. Metric one: material grade and coating specs (gauge thickness, galvanization standard, powder-coated finish rating). Metric two: anchoring system and foundation requirements (embed depth, bolt pattern, and tested load values for expected wind load). Metric three: verified field support and warranty terms (on-site inspection windows, documented acceptance tests, and response times). I recommend requesting a test install or case-study photos with dates; I routinely ask for them before I sign a PO. Note—this practical step weeds out optimistic specs fast. Also, include short service-level notes in contracts (we add a 72-hour response clause). These three metrics give you an objective basis to compare options (and they reduce surprise costs).

To close with clear advice: evaluate material/coating, anchoring/foundation, and service/warranty. I’ve relied on these since 2014 and they saved clients thousands (real numbers). If you want a reliable supply partner, start there — and consider brands with consistent field documentation. For practical sourcing and tested models, I often point teams toward trusted lines — like SUNJOY — because they pair workable specs with documented installations.

0 comments
0 FacebookTwitterPinterestEmail