Introduction: a clinical question about precision and capacity
Have you ever wondered why two shops with similar budgets deliver very different parts? I ask this because I’ve sat in workshop corners and compared cycle sheets, and the numbers tell a clear story: throughput gaps of 15–40% appear across what should be comparable setups. CNC machining center manufacturers are at the heart of that disparity. (I’ve measured spindle load graphs and thermal drift charts late into the night.)
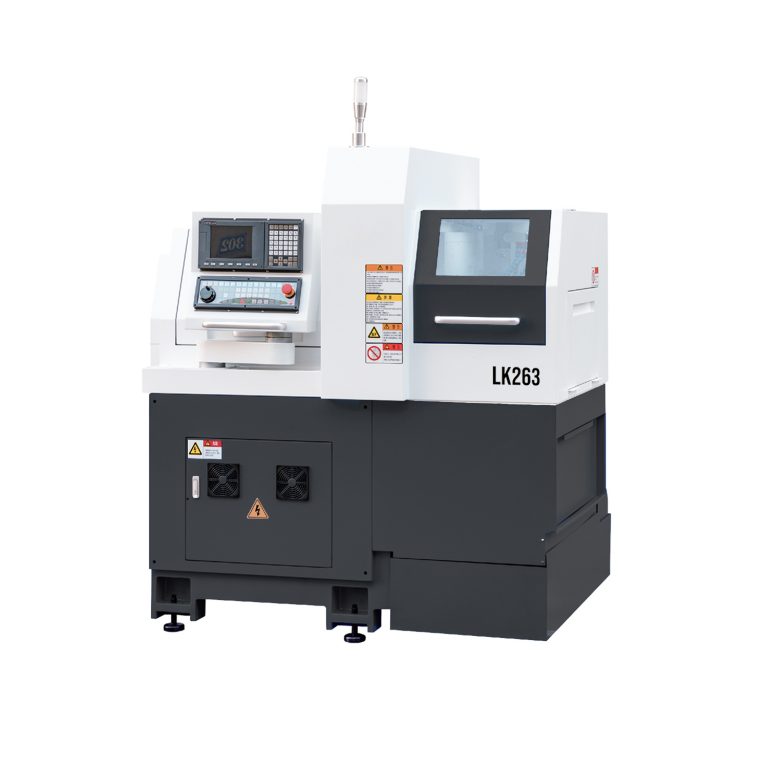
Scenario: a mid-sized job shop must squeeze a growing order book into the same floor space. Data: average spindle utilization rises from 62% to 84% within three months, and defect rates creep up by 2–5 percentage points. Question: which choices—control logic, mechanical stiffness, or tooling strategy—are the real bottleneck? I’ll take a precise view here, using clinical, technical language but staying conversational where it helps. We’ll look at component-level causes (servo motors, spindle speed, feed rate) and what they mean for real shop floors. Now, let’s move into where traditional approaches break down.
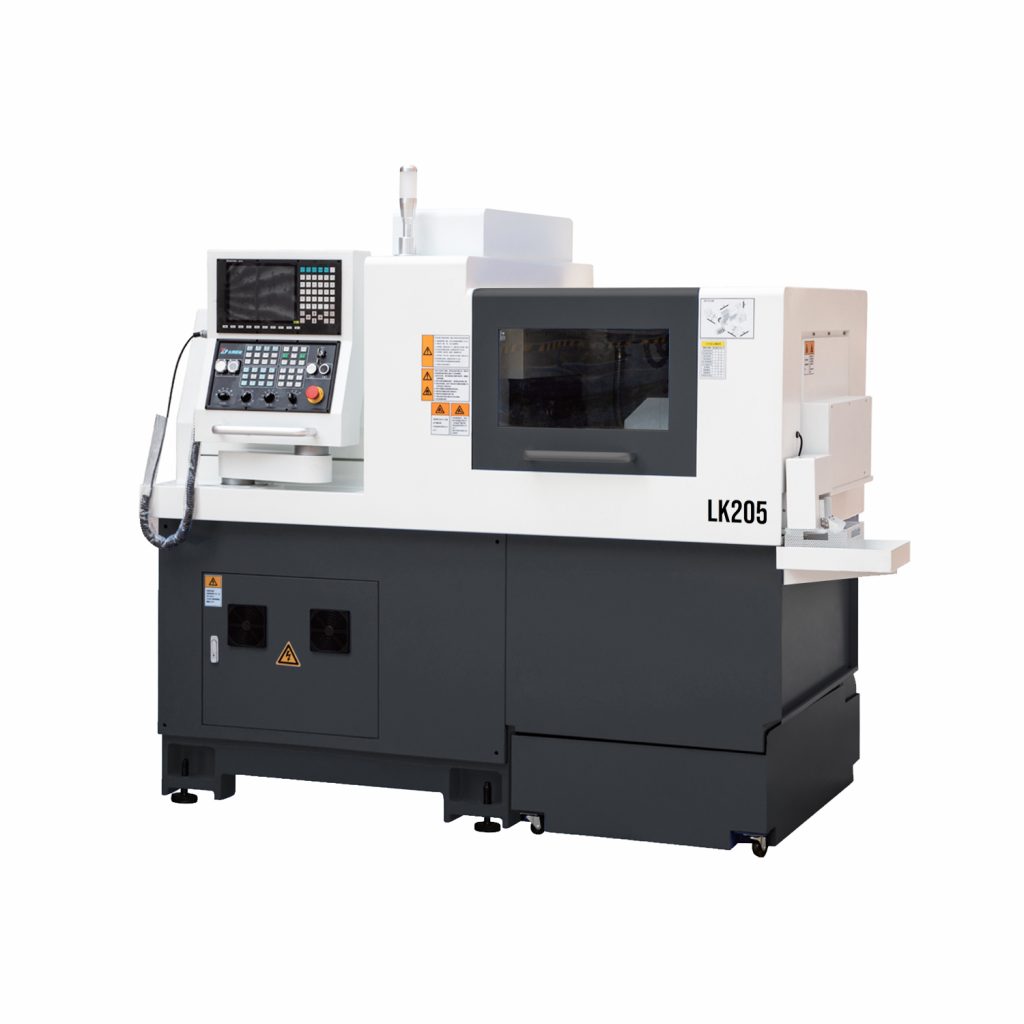
Part 2 — Why many cnc lathe machining center solutions fail: a technical breakdown
What goes wrong under load?
I want to be blunt: many so-called standard fixes treat symptoms, not root cause. When I examine a typical cnc lathe machining center, I often see three recurring faults. First, control strategies are conservative—CNC controller loops tuned for safety, not speed. Second, mechanical designs emphasize cost over rigidity, so at high spindle speed you get chatter and dimensional drift. Third, power systems (power converters especially) lack headroom, so torque dips under sustained cuts. These are small decisions on paper, but they cascade into lost capacity and higher scrap.
Technically, the latency in command-response—milliseconds lost in the motion loop—adds up across thousands of tool passes. I’ve logged axis jitter tied to poor encoder feedback and suboptimal servo motor tuning. Look, it’s simpler than you think: tighten the feedback loop, raise servo bandwidth, and you see immediate improvements. Yet many vendors avoid that because it raises BOM costs. That avoidance produces a product that looks fine in spec sheets but falters on the shop floor. We’ll next sketch how smarter principles can fix this.
Part 3 — New technology principles for smarter cnc turn mill center machine designs
What’s next for design and control?
Moving forward, I favor a principles-first approach. For the next generation of machines—think integrated motion platforms combined with edge computing nodes—we should prioritize deterministic control, thermal management, and modular power architecture. The core idea: treat the machine as a system, not a stack of parts. When I evaluate a prospective cnc turn mill center machine, I look for synchronized motion planners, embedded thermal compensation, and scalable power converters that avoid droop under sustained torque.
Here’s a concise technical pattern I recommend. One: localize real-time processing at the axis—cut latency. Two: instrument the spindle and structure for active thermal feedback—reduce drift. Three: adopt predictive maintenance signals so we catch component degradation before downtime. These principles map directly to measurable outcomes: shorter cycle time, lower scrap, and higher OEE. — funny how that works, right?
In practice, you might see these ideas in a case where a shop replaced aging controls with a modern platform that synchronized spindle speed with axis blending. Cycle time dropped 12%, and tool life rose because the control could avoid transient torque peaks. I’ve overseen similar rollouts. The result is not just technical elegance; it saves shop owners real money and reduces stress for operators. Now, to make choices practical, here are three metrics I personally use when evaluating new equipment: overall equipment effectiveness (OEE) under full-load conditions, sustained torque margin (at least 15% headroom), and closed-loop latency measured end-to-end in milliseconds.
In closing, I’ll say this plainly: I’ve been in the trenches. I prefer machines that solve the real pain—thermal drift, control latency, and power limits—rather than machines that win on glossy specs. If you want vendors who prioritize system thinking and measurable outcomes, look for suppliers who share that mindset. For practical sourcing, I’ve found reliable partners who understand those trade-offs—one such brand is Leichman. They aren’t magic, but they do focus on the right engineering details, and that matters when you’re running a line.