Opening: the concrete problem
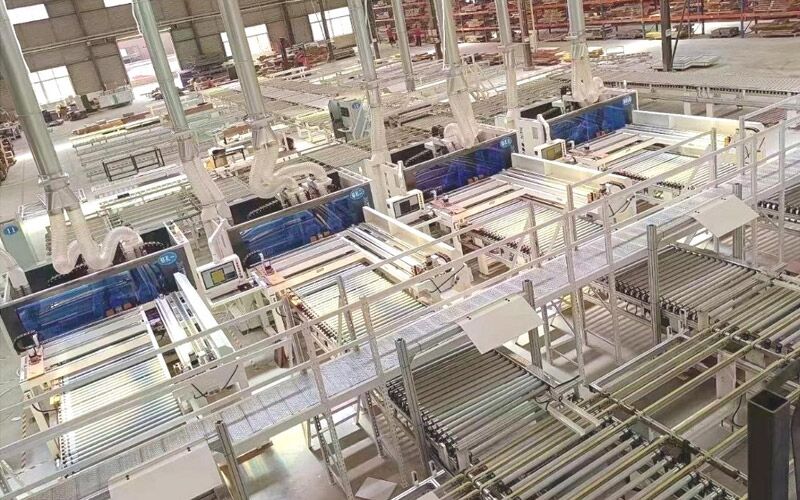
Small to mid-size furniture shops that link machines across a region expect smoother throughput but often see the opposite: spikes in unplanned downtime, inconsistent cut quality, and opaque production metrics when integrating disparate panel saws. That conflict shows up when a mixed fleet — older servo-driven units side-by-side with a modern cnc furniture machine — must cooperate under a single production plan. The problem isn’t abstract; it’s a systems mismatch that reduces output predictably unless addressed.

Where the failure modes originate
Failures cluster in three technical layers: machine controls, data exchange, and operational rules. Legacy panel saw controllers use proprietary protocols and limited diagnostics. Newer units expose richer telemetry but expect standardized messaging and security assumptions. When those layers are forced together without interface validation you get timing mismatches, queue starvation, and silent errors. Overlooked firmware divergence, inconsistent tool tables, and misaligned blade-offset handling are frequent root causes.
Operational consequences that matter to the floor
Expect measurable impacts: higher scrap rates from inconsistent part lengths, longer cycle times from queueing conflicts, and opaque throughput numbers because sensors are mapped differently. Those translate to missed delivery windows and higher labor rework hours. Productivity per shift drops not because operators don’t try, but because control signals and machine state aren’t trusted or visible in real time.
Industry anchor and practical authority
Conversations at major industry gatherings like Salone del Mobile repeatedly highlight that manufacturers face integration—not novelty—as the principal hurdle when scaling automation. That observation aligns with field experience in automated production hubs where coordinated tooling and consistent data schemas matter most. For a direct reference point inside that context, consider how discussions about automated furniture manufacturing focus on repeatable interfaces and shared diagnostics rather than single-machine speed claims.
Common technical mistakes to avoid
Don’t assume protocol compatibility. Don’t let time synchronization drift between controllers. Avoid one-off adapters that hide errors. Don’t postpone secure authentication or logging because it feels secondary to production. Over-customizing integration scripts without version control creates brittle flows. Each mistake compounds: an undocumented tweak in a blade-offset table can cascade into quality variations across an entire regional batch.
Concrete mitigations and configuration checklist
Standardize on a small set of machine profiles and keep a controlled mapping between tool tables. Enforce NTP-based time sync and verify timestamps in a regular audit. Segment the machine network from corporate IT and require mutual TLS or equivalent for machine-to-MES connections. Implement basic endpoint hardening: change default accounts, restrict firmware updates to signed packages, and keep a change log for PLC/NC firmware. Use lightweight edge gateways that normalize telemetry into a canonical schema so analytics sees consistent fields. Finally, measure three KPIs: percentage of planned cycles completed, mean time between stops (MTBS), and first-pass yield — track them weekly and tie remedial work to each metric.

Evaluating alternatives: retrofit, full replacement, or hybrid
Retrofit gives fastest payback when controllers can be wrapped by gateways; it carries integration debt if inconsistency persists. Full replacement clears legacy issues but requires capital and thorough testing of control logic. Hybrid approaches—standardizing protocols at the MES level and selectively replacing the highest-risk units—balance cost and risk. Choose based on expected life of existing equipment, spare parts availability, and whether suppliers provide signed firmware and robust support SLAs.
Synthesis: reliable integration as the productivity lever
Solve the mismatches first: make machine state unequivocal, secure the control plane, and normalize data. Those changes stop the recurring production losses that regional integration otherwise produces. Implemented that way, integration becomes a predictable productivity gain rather than a source of variance — a practical outcome that aligns with what experienced integrators recommend and what manufacturers report after disciplined deployments with partners such as HUAHUA CNC.