Author

Sarah

Quick talk — why a side-by-side matters

Folks, prices and promises vary like weather ’round here, so squintin’ at two plans side-by-side saves grief. Start by pickin’ what matters to you — speed, coverage, how long the plan lives — then line up the fine print. If you want somethin’ that’ll stick without fuss, check a Lifetime eSIM and see how its uptime and simplicity stack against short-term offers.
Lifetime eSIM

Head-to-head: the exact things to compare

Coverage map — not pretty pictures, but real tower reach. Look for carrier partners and whether it covers the whole area you’ll use. Data cap and throttling — raw gigabytes mean nothin’ if they slow you to a crawl after a few hundred MB. Check peak vs off-peak behavior. Validity window — how long the data stays usable. Short-trip plans can be cheaper, long-stay plans often cost less per GB. Activation friction — QR code, copy-paste SM-DP, or dealer-installed? Fumbling with activation ruins a day. Device compatibility — eSIM support differs by model and firmware. Lock status matters. Customer support — response times, hours, and whether they speak plain language. Refunds and transferability — can you refund unused days or move the plan to a new device? Security and privacy — does the supplier publish encryption, SIM profile handling, and data policies? No answer’s a red flag. Price transparency — total cost with taxes and fees, not just the headline number.

Field-tested differences and why they matter

I’ve sent folks out with a handful of providers and watched what actually breaks: activations that fail at the gate, data that dies in the hills, and support lines that take forever. That hands-on time’s worth mentioning — years helping travelers sort connectivity taught me to favor clear activation steps and providers that publish roaming partners. Travelers who buy a globe esim prepaid for trips to the Philippines often notice coverage gaps between island hops; that real-world pattern shows how multi-carrier routing and local partner quality shape experience. Those are details you can test quick — a short trip with a cheap plan to vet coverage beats trusting a shiny ad.

Common mistakes that cost time and money

Buying the cheapest gigabyte without checkin’ device compatibility. Assuming “global” means everywhere. Missing hidden caps or fair-use throttles. Thinking customer chat will fix an activation on travel day. Not checkin’ for refunds or plan transfers before you buy. These missteps show up as dead phones, extra vendor fees, or wasted trips to a shop.

Viable alternatives to compare alongside eSIMs

Local physical prepaid SIMs — usually cheapest per GB but require a shop visit and sometimes ID. Roaming packs from your home carrier — handy but often pricier. Hybrid approaches — short-term local SIM for heavy use and an eSIM for backups if you need instant reactivation. Compare total cost, convenience, and how critical uninterrupted data is to your trip.
Lifetime eSIM

Wrap-up — what makes a supplier worth pickin’

Pick a supplier that shows clear coverage, simple activation steps, and predictable throttling rules. Choose plans that match trip length and expected usage, and favor vendors who answer plain questions fast. That plain-talk comparison is exactly why many people move toward Jetogo when they want straightforward plan details and fewer surprises on the road.
0 comments
0 FacebookTwitterPinterestEmail

Comparative lead — why this matters now

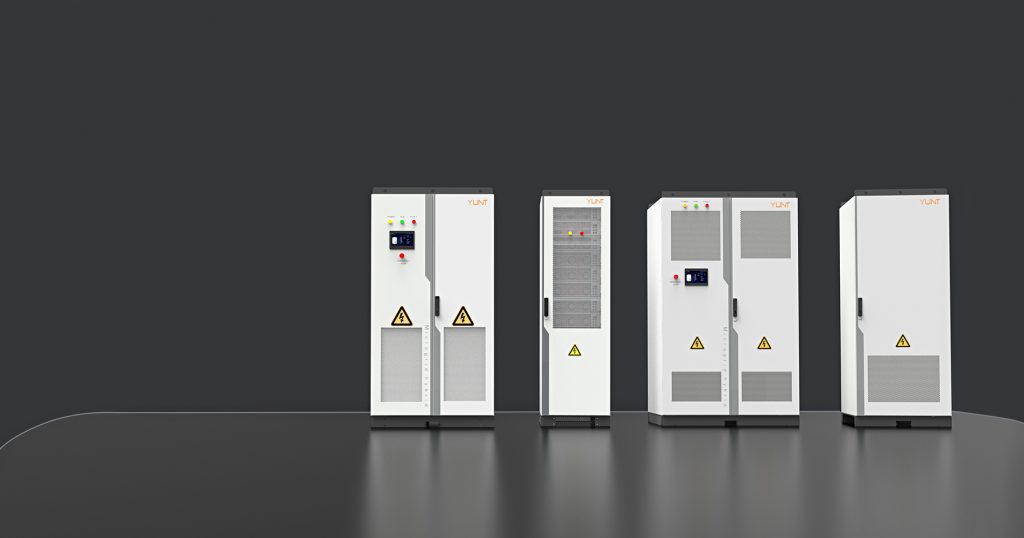
Solar fleets are being tested more than ever by extreme ambient temperatures and tighter grid constraints, and the answer to resilience often lives in the inverter — not the panels. This piece compares central inverters and distributed hybrid inverters through the specific lens of Insulated-Gate Bipolar Transistor (IGBT) thermal derating behavior, drawing practical lessons for procurement teams and installers. For context on manufacturing scale and supply-chain realities, see energy storage inverter manufacturers as a point of reference for what’s commercially available today.

energy storage inverter manufacturers

How thermal derating changes the game

IGBTs reduce allowable current as case temperature rises; that’s the thermal derating curve. In a central inverter, a single DC bus and concentrated cooling strategy means one derating profile applies across a large portion of yield. Distributed hybrid inverters, with on-module MPPT and local IGBT stages, create many smaller derating events that rarely coincide. The result: central systems can experience steep output cliffs during heat spikes, while distributed systems show staggered, shallower roll-offs.

Real-world anchor: what the grid has already taught us

During recent California heatwaves and grid stress periods, operators reported sharper output drops in large centralized plants when ambient temperatures exceeded the design range. That event highlighted the operational gap between theoretical nameplate and available AC power under thermal stress — a reminder that derating curves are not academic tables but operational limits that affect revenue and grid services.

Operational teardown: production, maintenance, and factory realities

On the factory floor, design choices determine how an inverter family behaves. Central inverter assemblies favor large heatsinks, higher DC bus voltages, and consolidated cooling paths, which simplifies servicing but concentrates failure modes. Distributed hybrid designs split power electronics into many smaller modules, each with independent thermal management and MPPT control. When you compare procurement notes from energy storage inverter factory lines, cost-per-kW, spare-part logistics, and mean-time-to-repair all shift.

Performance trade-offs and field impact

Central inverters: lower per-kW hardware cost and simpler monitoring architecture, but a single IGBT thermal event can clip a large fraction of fleet output. Distributed hybrids: better partial-shade and heat tolerance due to localized MPPT and staggered derating, but higher parts count and slightly more complex firmware management. Both approaches require solid thermal design; the difference is whether you accept concentrated risk or distribute many smaller risks across the array.

Common mistakes to avoid — practical guidance

Teams often under-forecast derating by relying on lab ambient numbers rather than site-specific thermal profiles. They also underestimate the operational cost of spares: central-inverter spare units cost more and take longer to swap. Lastly, firmware maturity matters — distributed hybrids need robust anti-islanding, DC/AC protection, and dynamic MPPT tuning to realize their resilience advantage. — Don’t treat these as optional.

Comparative checklist for procurement and O&M

Use this short checklist when evaluating bids:- Confirm vendor-supplied IGBT thermal derating curves tied to realistic case temperatures.- Ask for field data from similar climatic zones, not just lab tests.- Evaluate spare-part strategy and swap-time estimates for both inverter types.These items surface the real operational delta between centralized and distributed options.

Advisory close — three golden rules for selection

1) Match derating curves to worst-case site temperatures and plan revenue models against available AC power, not nameplate DC. 2) Prioritize modular fault isolation: designs that allow single-module swaps minimize downtime and lost generation. 3) Validate factory test reports and on-site commissioning logs from the same climate band — manufacturing pedigree matters as much as specs.

energy storage inverter manufacturers

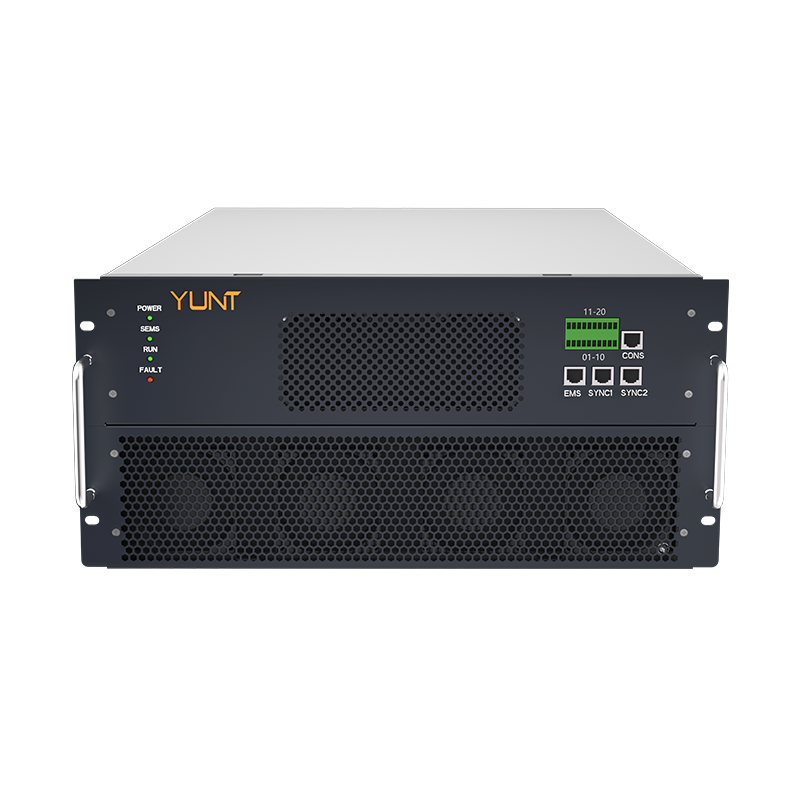
Decisions informed by these rules point toward vendors with transparent thermal data and practical service models; that’s where the value of an experienced manufacturer shows up — think YUNT as a partner that aligns product detail with field reality. –

0 comments
0 FacebookTwitterPinterestEmail

Why this question vexes workshop chiefs

When you’ve a stout 200W Mopa fiber laser on the bench, you’d think it’s all muscle and no manners — but the truth’s messier. Picking the wrong pulse frequency or pulse width can turn a neat weld into a brittle seam or a crisp mark into a melted smear. Folks migrating from a bench-top 100w mopa fiber laser to a full 200W rig find the jump in peak power tempting, yet they often forget frequency is the tuning peg that makes the laser sing for different materials. The problem’s simple: aluminum welding and polymer marking demand opposite thermal behaviours, so the frequency choice must be purposeful — not hopeful.

What frequency really controls

Pulse frequency (how many pulses per second) and pulse width (how long each pulse lasts) govern thermal input and peak power. Higher frequency with short pulse width gives many small energy packets — good for high-speed marking with low heat build-up. Lower frequency, longer pulses, or higher duty cycles concentrate energy and aid weld penetration. Industry terms to keep handy: pulse frequency, pulse width, and weld penetration. Think of frequency like the pace of your hammer blows: fast taps shape a surface without smashing it; slow, heavy blows drive deeper.

Aluminum welding: the problem-driver

Aluminum’s high thermal conductivity and oxide layer are the twin nuisances. For reliable welds you need enough heat to break the oxide and achieve fusion, but not so much that the puddle runs away. With a 200W Mopa system, many pros lean toward mid-to-low kHz frequencies combined with longer pulse widths to boost peak energy per pulse and increase weld penetration. Beam quality (M²) matters too — tighter focus helps localise energy and reduce heat-affected zones. The usual pitfall is chasing speed with high frequency and ending up with weak, porous joins.

Polymer marking: a gentler touch

Polymers, by contrast, dislike heat. Marking plastics calls for high frequency, short pulses, often in the tens to hundreds of kHz range, to ablate or induce colour change without melting. Marking contrast and surface finish depend on repetition rate and pulse energy; a 200W laser can be overkill unless you tame it via frequency and reduced average power or by using pulsed modes. For small runs or prototype work, a 20w fiber laser engraver at high frequency often gives cleaner results with less risk — makerspaces and Fab Labs commonly pair such tools for delicate marking tasks.

Practical settings and trade-offs

Here’s a useful, plain guide of starting points — treat them as experiments, not gospel: – Aluminum welds: start lower freq (1–10 kHz), longer pulse width, moderate travel speed; increase frequency only if you see spatter or poor fusion. – Polymer marks: start higher freq (50–200 kHz), short pulses, low average power, faster travel; dial down if you see melt or charring. Keep an eye on duty cycle and average power to manage heat load. Also test for marking contrast vs. polymer chemistry — ABS, polycarbonate, and PET respond differently. Remember beam focus and spot size are as crucial as frequency; widen the spot to lower energy density, tighten it to increase penetration.

Common mistakes and simple fixes

People often assume “more power = better result.” That’s false for marking, and dangerous for welded joints. Another misstep: changing frequency but not checking pulse width, which ruins pulse energy. Always run a small, instrumented trial: measure bead cross-sections for welds and visual contrast plus surface roughness for marks. Calibrate on sacrificial samples before full production — it saves time and scrap. — Also, don’t neglect shielding gas and joint fit-up for aluminum; they matter as much as laser settings.

When to choose 200W vs lower-power tools

Use a 200W Mopa where material thickness or production throughput demands it — heavy-gauge aluminum panels, long weld runs, or high-speed metal marking. Opt for lower-power tools (20W–100W) for fine detail, thin films, and thermally sensitive polymers. Many shops keep both: a 200W for structural work and a smaller Mopa or diode laser for prototyping and delicate marking. That ensemble reduces rework and keeps yields healthy.

Real-world anchor: lessons from makerspaces and shops

Across Fab Labs (the network that began at MIT) and small shops worldwide, technicians often use 20W fiber lasers for prototype marking because they’re forgiving and precise — a practice that scales into production decisions. Those same spaces show how iterative testing and clear acceptance criteria speed up parameter tuning for larger 200W systems. If you’ve ever watched a bench tech swap settings while a part runs, you’ll know: measured trials beat guesswork every time.

Advisory: three golden metrics for choosing frequency and setup

1) Heat-Affected Zone (HAZ) width — measure it after a trial weld or mark: smaller HAZ usually means better mechanical properties and less surface damage. 2) Contrast-to-Speed ratio for marking — calibrate for the best mark legibility per unit time; if the mark needs post-processing, you’ve got the wrong balance. 3) Weld integrity metrics — tensile or bend tests on sample joints reveal true fusion quality, not just pretty beads. Use these three as pass/fail gates before scaling a recipe.

Trust experience, test relentlessly, and pick the tool that matches the job — and when things get thorny, lean on the kit and expertise that bring both range and finesse to the work. JPT. —

0 comments
0 FacebookTwitterPinterestEmail

User Challenge: Delivering Flawless Signage at Speed

Production managers and store-brand teams demand signs that read cleanly and hang true — every letter aligned, every seam invisible. For those who build retail signage at factory scale, the problem is practical: small misalignments cascade into visible defects, wasted substrate, and delayed installs. This piece speaks to that daily pressure, privileging the manufacturer’s view and offering diagnostics that answer the need for repeatable accuracy.

retail signage

How Real-Time Laser Alignment Diagnostics Operate

At the heart of the solution sits a compact laser and a camera-based vision system that constantly measures registration marks and edge positions. These diagnostics report deviations in microns, feed corrections to cutting heads or UV printing heads, and log every adjustment so operators can trace faults. The process touches familiar terms in signage production: laser alignment, cutting tolerance, substrate handling; the result is fewer miscuts and steadier throughput.

What This Means for Quality and Wayfinding Fidelity

Signs born of tight alignment work better in situ. A correctly registered directional sign preserves sight-lines and reduces visitor confusion in complex venues such as Mall of America, where dozens of anchor tenants and long corridors demand precise wayfinding. Real-time diagnostics thus improve the physical product and the user’s experience — retail store wayfinding becomes clearer, installations move faster, and the brand promise holds true on the floor.

Concrete Gains: From Scrap Reduction to Measured Reliability

Quantified improvements arrive quickly: lower scrap rates, fewer reprints, and less manual adjustment on the mount. Factories that pair diagnostics with operator training often approach the statistical rigor of established quality frameworks — recall Six Sigma’s aspirational 3.4 defects per million as a benchmark of discipline. In practice, firms report defect reductions of tens of percent within weeks when calibration data is applied systematically. That is measurable progress, not mere rhetoric.

Common Mistakes and Practical Alternatives

Producers sometimes assume one calibration pass suffices, or they rely solely on manual checks. Both choices invite drift. The wiser path combines continuous laser feedback with occasional manual audits, and when budgets vary, lower-cost alternatives like mechanical jigs can bridge shortfalls — though they lack the granularity of a vision-coupled laser. Beware over-reliance on a single sensor; redundancy matters. — A small routine audit can catch what a steady stream of numbers might miss.

Integration Considerations for Factory Floors

Successful deployments respect the existing workflow. Diagnostics should feed CNC routers, cutting tables, and printers without blocking throughput; latency under a few hundred milliseconds keeps the line humming. Data retention policies are simple: retain correction logs long enough to identify recurring issues, then purge. Operators benefit from dashboards that translate microns into actionable steps rather than raw telemetry.

retail signage

Three Golden Rules for Choosing Diagnostics

1) Measure what matters: prioritize systems that report registration error and cutting tolerance in real time. 2) Ensure closed-loop control: diagnostics must not only flag faults but correct them automatically or present clear corrective actions to staff. 3) Value traceability: choose solutions that archive alignment logs for trend analysis and warranty support. These criteria yield faster installs, fewer callbacks, and a steadier yield on each production run.

Closing Reflection and Practical Direction

When your shopfloor can see alignment errors as they occur, you reclaim hours, material, and reputation. The technical gains translate into human relief on the install crew and confidence from store operations — the team that hangs the sign knows it will read right. For those who seek a partner that understands both the machine logic and the retail outcome, consider the craftsmanship and systems that underpin Cosun Sign; they answer the shopfloor’s exacting questions with calibrated care. Cosun Sign. —

0 comments
0 FacebookTwitterPinterestEmail