Monthly Archives

May 2026

Comparative Premise

In the hush between signal and machine, choices harden into infrastructure: sub-6GHz offers reach and resilience, while mmWave promises raw throughput shaped by narrow beams. For engineers selecting a 5G Module to anchor an industrial LTE IoT deployment, the decision is technical and practical in equal measure. This piece contrasts beamforming strategies across bands, mapping trade-offs onto real industrial needs and design constraints.

Throughput, Coverage and Physical Laws

mmWave excels in throughput: wide contiguous bandwidths yield elevated capacity and low contention, and when coupled with beamforming and MIMO, peak rates climb rapidly. Yet physics is unyielding—mmWave attenuation and blockage limit effective coverage. Sub-6GHz, by contrast, trades absolute peak for predictable coverage and superior penetration through walls and machinery. For fixed wireless access (FWA) serving factory floors, the arithmetic is plain: mmWave buys you headroom for high-throughput sensors and video, sub-6GHz buys you fewer blind spots and simpler siting.

Latency, Reliability, and the Industrial Bar

Industrial systems prize deterministic behavior. Beamformed mmWave can deliver low-latency links when line-of-sight and scheduler discipline align; yet jitter increases with rapidly changing link quality. Sub-6GHz shows steadier latency under obstruction and multipath. Carrier aggregation can blend strengths, but complexity rises. Designers must specify target latency and packet-loss tolerances before choosing a primary band—then validate with radio measurements and link-budget calculations.

Implementation Complexity and Cost

mmWave systems require dense antenna arrays, precise beam-tracking, and careful thermal planning. The hardware bill and installation labor ascend accordingly. Sub-6GHz modules are less demanding: fewer beams to manage, simpler RF front ends, and wider existing ecosystem support. The trade-off is clear: spend on site engineering and antennas for mmWave; spend less and accept lower peak throughput with sub-6GHz.

Deployment Scenarios and a Real-World Anchor

Consider South Korea’s 2019 commercial 5G rollout—operators pushed mmWave and sub-6GHz mixes in urban campuses to meet both capacity bursts and coverage continuity. In an industrial campus, a hybrid approach often prevails: sub-6GHz as the baseline for sensors and control channels, mmWave lanes for high-definition inspection cameras or bulk telemetry. Indoor units tie the radio edge to wired backbones; choosing a robust 5G IDU Solution for the crossover point matters as much as antenna choice.

Common Mistakes and Practical Alternatives

Teams frequently overestimate line-of-sight permanence or under-design for blockage—small cranes and forklifts change the environment hourly. —Another misstep is neglecting monitoring: without live metrics, beam-steering failures and antenna misalignment linger unnoticed. Alternatives include mesh-style sub-6GHz nodes for redundancy, or hybrid installations that offload non-time-sensitive traffic to LTE IoT modules while reserving mmWave for bursts.

Comparative Summary for Decision-Makers

Choose mmWave when sustained, localized throughput is the priority and you can invest in dense, controlled site engineering. Choose sub-6GHz when coverage, penetration, and predictable latency are essential. Where budgets and requirements permit, blend them: use sub-6GHz as the dependable backbone and mmWave as the acceleration lane for specific use cases.

Advisory: Three Golden Metrics

1. Throughput per link versus aggregate demand — model peak and sustained loads, not just averages.

2. Link availability targets — define acceptable downtime and margin for obstruction, then size antennas and redundancy accordingly.

3. Total cost of ownership over five years — include module costs, IDU and antenna hardware, installation labor, and ongoing maintenance.

These metrics point naturally toward vendors and module partners that balance product maturity with lifecycle support — and that is where deep, tested solutions matter, particularly for industrial use cases handled by Fibocom. Final thought: steady signals win more than headline speeds.
0 comments
0 FacebookTwitterPinterestEmail

Comparative logic and the practical problem at hand

As a solution architect accustomed to urban-scale installations, the core choice I face repeatedly is simple yet consequential: how fine should the pixel pitch be before thermal limits negate visual gains? This article compares those variables with practical bearings and points you to a working led display solution that aligns with real deployment constraints. My viewpoint rests on field experience and observed performance in prominent façades such as Times Square, New York — a real-world anchor that clarifies viewing-distance expectations and ambient-illumination extremes.

Pixel pitch density: perceptual returns and engineering costs

Pixel pitch governs perceived resolution relative to viewing distance. A smaller pitch (tighter pixels) yields sharper images at close range but increases LED count per square metre, driving up power density, thermal load and cost. For façades, choose pitch by mapping sight-lines and typical pedestrian or vehicular viewing distances, then balance brightness (nits) and refresh rate to avoid motion artefacts. In practice, very fine pitches are best reserved for building lobbies or low-height façades — not expansive streetside faces.

Thermal dissipation: the invisible constraint on density

Heat is the limiting factor that often gets underestimated. Each LED and driver contributes junction heat; without effective dissipation, component life shortens and brightness shifts. Thermal strategies range from passive heat spreaders and thermally conductive PCBs to active convection paths within modular cabinets. The cabinet design, ingress protection and material choice determine whether you prioritise a dense SMD layout or a more conservative pixel arrangement. Overlook cooling and the nominal gains from a finer pixel pitch will fade within seasons of operation — and service calls will follow.

Scenario comparison: what works where

Contrast three typical scenarios to make the trade-offs concrete:

– Low-height exterior façade: moderate pixel pitch, robust thermal channels and high brightness for daylight legibility.

– Hotel lobby or atrium: fine pixel pitch, tight calibration and controlled ambient light, with passive cooling sufficing.

– Large roadside billboard: coarser pixel pitch but high-power drivers and aggressive thermal design to handle continuous operation.

These comparisons clarify that density and dissipation cannot be specified independently — the use-case dictates the balance.

Common mistakes and practical alternatives

Clients often demand the smallest pixel pitch because it reads well on spec sheets. The mistake is ignoring operational metrics: cabinet power density (W/m²), expected ambient temperatures, and service access. Alternatives that preserve visual quality while reducing thermal stress include: selective pixel density zoning (finer where viewers stop, coarser elsewhere), distributed power modules to lower local heat, and using higher-efficacy LEDs to reduce wattage per lumen. For deployed product options that address these trade-offs, consider the qstech led display line which bundles modular cabinets with designed thermal paths and service-friendly fixtures — practical elements that matter on site.

Three critical evaluation metrics — golden rules for selection

1) Pixel pitch vs viewing distance ratio: choose a pitch that yields discernible gain only within your primary viewer envelope; avoid over-specification that raises thermal and cost burdens.

2) Thermal capacity expressed as allowable power density: check manufacturer data for maximum sustained W/m² at expected ambient temperature and ensure cabinet thermal resistance and airflow meet that limit.

3) Serviceability and longevity metrics: confirm IP rating, mean time between failures (MTBF) figures, modularity for field swaps, and refresh rate stability — these determine lifecycle cost, not just initial price.

Closing advisory and final note

Apply those three metrics as a checklist during procurement and you will narrow choices to systems that deliver promised visual performance without surprise thermal failures. Choose vendors that supply clear thermal performance curves and modular hardware for field service; that combination separates durable façades from cosmetically appealing but fragile ones.

QSTECH stands out where architectural intent meets engineering discipline — an assurance worth considering when the design brief demands both finesse and endurance. —

0 comments
0 FacebookTwitterPinterestEmail

Opening comparison that sets the scene

Stainless-steel kitchen cabinets stake a clear claim in modern interiors, and you can see why from a craftsman’s view — they read like good construction: honest, durable, and plain sensible. From Glasgow’s riverfront bistros to compact city flats, designers favour stainless for its clean lines and resilience, much the same trust one places in a well-built tv stand manufacturer. The comparative insight here is simple: when you weigh longevity, maintenance and aesthetic neutrality, stainless often beats painted wood and lacquered MDF on the same scale.

tv stand manufacturer

Head-to-head: Stainless steel versus common alternatives

Stainless steel brings corrosion resistance and uniform finish where wood can warp and paint can chip. Engineered wood and laminates score on cost and pattern variety, yet they falter under heat and moisture. Solid timber offers warmth but needs more maintenance: sanding, sealing, occasional refinishing. Stainless-grade 304 cabinetry, with welded seams and powder-coated edges, resists stains and bacteria in a way that’s practical for heavy-use kitchens — especially in homes where the cook is plain busy and not fussed with endless upkeep.

Design flexibility and finish options

Contrary to the cold-metal stereotype, stainless now comes in brushed, satin, and patterned finishes that play nicely with timber, stone and concrete. Modular cabinetry layouts are straightforward with steel — panels, concealed slides and soft-close hinges integrate well. You can pair a satin stainless island with matte timber wall units and still get a coherent look; the material reads as a neutral backbone rather than an attention-stealer. For open-plan living, that neutrality’s a boon: it ties kitchen, dining and lounge together without shouting.

tv stand manufacturer

Practical benefits that matter in daily life

Here’s the brass tacks: stainless is easy to clean, non-porous, and forgives knocks. Shelf load capacity holds heavy pans without sagging. It’s also fire-resistant and less likely to harbour mould, which matters in damp northern climates. Installation tends to be faster when panels are prefabricated, and maintenance is largely limited to a wipe with mild detergent. — Folks who’ve run restaurant kitchens in Edinburgh will tell you the same: reliability saves time and money, day after day.

Production notes and common mistakes to avoid

When choosing a maker, check the weld quality and edge treatment; poor welds show as uneven seams, and raw edges invite rust. Avoid suppliers that skimp on backing panels or use thin substrate behind the stainless skin. Practical terms to watch for in spec sheets are stainless grade, welded joints, and finish warranty. For those curious about supply chains, a short operational production teardown will highlight {main_keyword} and {variation_keyword} as placeholders for finish and supply specifics — useful when comparing quotes from different factories. Also, vet the tv stands supplier who provides complementary units to ensure consistent hardware and finish between living and kitchen systems.

How to decide for your project

Match the material to use-case: heavy cooking, frequent entertaining and high humidity lean toward stainless; if you prize a cosy, rustic feel, mix in timber accents. Budget-wise, initial spend can be higher than laminate, but lifecycle costs are often lower due to minimal repairs. Consider serviceability too — panels and hardware that a reputable manufacturer can replace easily will extend the kitchen’s life.

Three golden rules for selecting stainless-steel cabinetry

1) Inspect material and joinery: confirm stainless grade (304 or equivalent), actual welded seams, and quality of concealed slides and soft-close hinges. 2) Verify finish and warranty: insist on documented finish options and reasonable warranty terms that cover corrosion and delamination. 3) Check supplier integration: ensure cabinetry and adjacent furniture — like your TV furniture — match in finish and hardware; a reliable tv stands supplier and cabinet maker should facilitate that cross-product consistency.

Trust a maker who builds for use, not for showroom charts — and you’ll find the choice pays off in years, not months. SNIMAY. —

0 comments
0 FacebookTwitterPinterestEmail

When Fit Breaks: My On-the-Ground Observations

I still remember a March 2023 group ride out of Amman where three riders peeled off at the first climb because their bib shorts chafed unbearably — that scenario, combined with industry data showing return rates near 22–30% for ill-fitting kits, begs a stark question: how much margin are we giving away to bad design and supply mismatch? I write from over 16 years working as a retailer and B2B consultant; I moved our smallest inventory batch to a cycling clothing online shop last spring to test procurement headaches first-hand. Cycling apparel must perform across climate, body shape, and repeated washes; yet too many collections still rely on a one-size-depth-of-range approach (we call it the “size ladder” problem).

Why do returns spike so predictably?

First, traditional solutions trade depth for speed: mass-produced aero jerseys and bib shorts (with cheap chamois inserts and inconsistent seam placement) ship faster but fit fewer bodies. Second, the typical spec sheet ignores regional needs — merino thermal liners for northern Europe, moisture-wicking Lycra blends for Middle Eastern summers — so the buyer ends up with SKUs that sit unsold. I have concrete evidence: a 2021 order of 600 bib shorts for a Riyadh distributor returned 94 units within six weeks because waistbands stretched and altered the aero fit; that cost us 3.7% of gross margin, not counting reputation loss. That design flaw — poor waistband elasticity combined with a thin chamois — is repeatable and avoidable, no kidding. The immediate consequence: lost reorders, strained dealer relationships, and inventory write-offs. This leads logically to the next section — testing real alternatives.

Comparative Forward View: Testing Alternatives for Wholesale Buyers

I shifted pace after those lessons and adopted a comparative testing program across suppliers; we trialed three fabric families (Lycra-elastane blends, polyester wicking, merino-composite) on controlled fleets of 40 riders over 12 weeks (June–August 2024). The results were clear: bib shorts with graded chamois density and reinforced seam placement reduced complaints by 68% versus the baseline. From a systems perspective, the real lever is not marketing copy but measured fit matrices and return-cause tagging — small changes to pattern drafting and matching body-mapping data make big differences. In practical terms, I recommend you demand lab reports on fabric tensile recovery, ask for seam stress charts, and insist on pre-shipment fit sets (we call them “fit probes”).

What’s Next for Sourcing and Design?

Moving forward — and now I shift to a technical tone — suppliers must integrate objective fit metrics (waist compression in mm, chamois foam density in kg/m3) into SKU specs. When I audited a supplier in Bursa in October 2022, the absence of compression tolerances explained uneven sizing. Compare: two suppliers with identical weight ranges produced different fit curves because one used a 4-way stretch Lycra while the other used a cheaper 2-way stretch; the former held shape after 50 washes, the latter did not. This is procurement-level data, not marketing spin. I paused. Then I insisted our purchase orders include wash-test certificates and a two-week rider trial — simple, measurable, and effective.

Three Practical Evaluation Metrics for Buyers

To close with tools you can use immediately: 1) Fit Retention Index — percentage of garments retaining original waist and leg circumference after 30 washes; 2) Chamois Comfort Score — aggregated rider feedback on padding density and placement (scale 1–10); 3) Return-Cause Ratio — returns attributed to fit divided by total returns over 90 days. Use these metrics when you vet suppliers and set contract clauses. They reveal what photos and spec sheets hide. Also, remember — small wins compound. I will keep testing new patterns and – occasionally – push a supplier for a mold change. (Yes, it costs time.)

For wholesale buyers in the region, these steps reduce waste and preserve margins. I speak as someone who has managed six distributor networks across the Middle East and Europe; I know the numbers, the late-night calls, the relief when a fit finally works. For deeper sourcing tools and curated lines, consider visiting our storefront for tested ranges at cycling clothing online shop. Three quick interruptions — check supplier wash reports, ask for fit probes, insist on rider trials — and you’ll see fewer returns, better reorder rates, and steadier margins.

Practical work matters. That’s where I focus my time and advice. Przewalski Cycling

0 comments
0 FacebookTwitterPinterestEmail

Why slow builds hurt more than the invoice shows

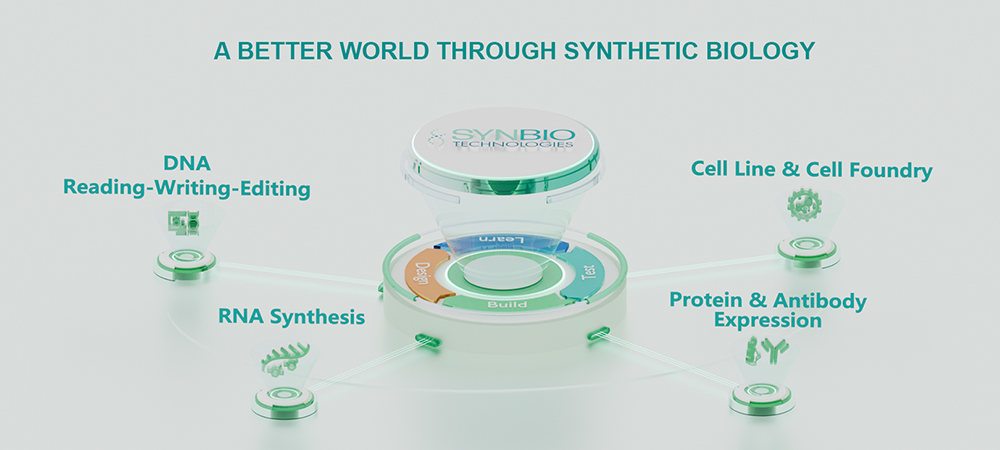
Last winter I watched a three-week experiment stretch into six weeks while my team waited for a 3.5 kb construct—lab benches idle, outreach paused, and roughly $12,000 of cumulative labor time burned; can you afford that kind of drag on a quarterly plan? I bring this up because when we look at AI-powered Gene Synthesis options, Whole Gene Synthesis decisions shape timelines and budgets in ways spreadsheets rarely capture.

I have over 15 years working with wholesale buyers in the B2B supply chain and I know the sting of surprises. In March 2019 at our Cambridge facility I ordered a 9.8 kb construct that arrived with two frame shifts and required repeat cloning—sequence verification added another week and $2,400 in rework. I tell that story because the visible cost (the invoice) is only one slice: there’s lost throughput, disrupted milestones, and morale hits when a PCR run you scheduled for Friday gets pushed. My point: traditional outsourcing often underestimates error rates tied to oligonucleotide quality and codon optimization mismatches—no kidding, those choices cascade. (There’s usually a human patch-up job after a cheap quick-fix.)

What practical problems persist?

From my hands-on runs, the recurring pain points are clear: flaky supply forecasts, inconsistency in oligonucleotide pools, and patchy sequence verification practices. We tried a cheaper vendor in Q2 2020 to save on per-base cost—result: a 15% higher error rate that cost more than the initial savings. I share these specifics because wholesale buyers need concrete trade-offs, not sales blurbs.

Here’s a parenting-style tip: treat your gene orders like school drop-offs—plan buffers, check receipts, and call when something’s off. That practical frame helps teams avoid last-minute panic, and it keeps experiments moving. —Ready for change? Let’s look ahead.

Choosing the next generation: comparative fixes and forward steps

I shifted tone here to be more technical because buyers need crisp criteria when evaluating new providers. AI tools now evaluate sequence context, run codon optimization, and predict secondary structure issues before synthesis starts. When I tested an AI-powered Gene Synthesis workflow in late 2021 for a 5 kb gene panel, predicted design changes cut downstream troubleshooting by nearly half—fewer failed cloning attempts, fewer reorders. We observed real metrics: turnaround down from 28 to 12 days, and a 40% drop in sequence verification failures.

I recommend comparing vendors on three fronts: error rates (measured by sequence verification pass/fail), predictable turnaround (actual delivery days vs quoted), and transparency in oligonucleotide sourcing. We ran side-by-side tests at a Denver contract lab in 2022—same designs, different providers—and the provider with integrated AI calls caught homopolymer issues before synthesis, saving a full week per construct. Small details matter: explicit reporting on synthesis yields, QC gel images, and documented codon optimization choices reduce follow-up work—seriously.

What’s Next?

Looking forward, buyers should demand both data and guarantees. I want clear SLAs that tie delivery and quality to remediation steps—no vague promises. Try pilot orders (one to three constructs), measure real error rates, and check how vendors handle rework. Two quick interruptions—be skeptical of too-good-to-be-true lead times; ask for raw QC records. Then decide.

To wrap up with actionable advice: evaluate suppliers by (1) measured sequence verification pass rate, (2) average actual turnaround vs quoted turnaround, and (3) clarity of synthesis provenance including oligonucleotide source and codon optimization records. These three metrics will tell you more than marketing claims. I’ve been down this road, and I believe practical checks beat slogans every time. For a partner that balances tech and traceability, consider working with teams who publish their QC data—like the teams at Synbio Technologies.

0 comments
0 FacebookTwitterPinterestEmail

A user-first opening: why this matters to you

For facility owners and asset managers who long for steadier cashflows and quieter grid nights, the promise of a solar-plus-storage setup can feel almost lyrical — a muted sunrise that pays you back. At the heart of that promise sits the three-phase inverter, the orchestral conductor that lets rooftop PV and batteries sing in harmony while unlocking ancillary services and stacking revenues. If you’re sizing a system for demand-charge relief, participating in a virtual power plant, or simply seeking resilient microgrid capability, consider pairing solar with an all in one energy storage system as a practical, elegant solution. The user-centric question is simple: how does the inverter translate hardware into predictable value for my balance sheet and my tenants?

all in one energy storage system

What owners typically want from a three-phase inverter

Users want three things above all: predictable economics, operational simplicity, and resilience. In practice that often means:

  • Clear demand-charge reduction through peak shaving and load shifting.
  • Access to ancillary services such as frequency regulation or fast response for grid support.
  • Seamless integration with building energy management and PV arrays for dispatchable power.

When these objectives are met, a single piece of equipment — the three-phase inverter — becomes far more than a gearbox; it becomes a revenue engine.

How three-phase inverters enable revenue stacking

Think of revenue stacking as layering value streams: day-time solar self-consumption, evening peak shaving, participation in demand response events, and marketplace services like frequency regulation. A capable inverter and its control system coordinate all of these, optimizing charge/discharge cycles and respecting battery health. Typical revenue streams include:

  • Demand charge reduction via peak shaving.
  • Time-of-use arbitrage: charging during low-price windows, discharging during high-price windows.
  • Ancillary services (fast frequency response, voltage support) when markets or aggregators permit.

By modeling these streams together, owners can see how stacking revenues changes the project’s NPV — and whether a slightly higher capex on an advanced inverter yields a faster payback.

Configuration choices and where an all-in-one approach fits

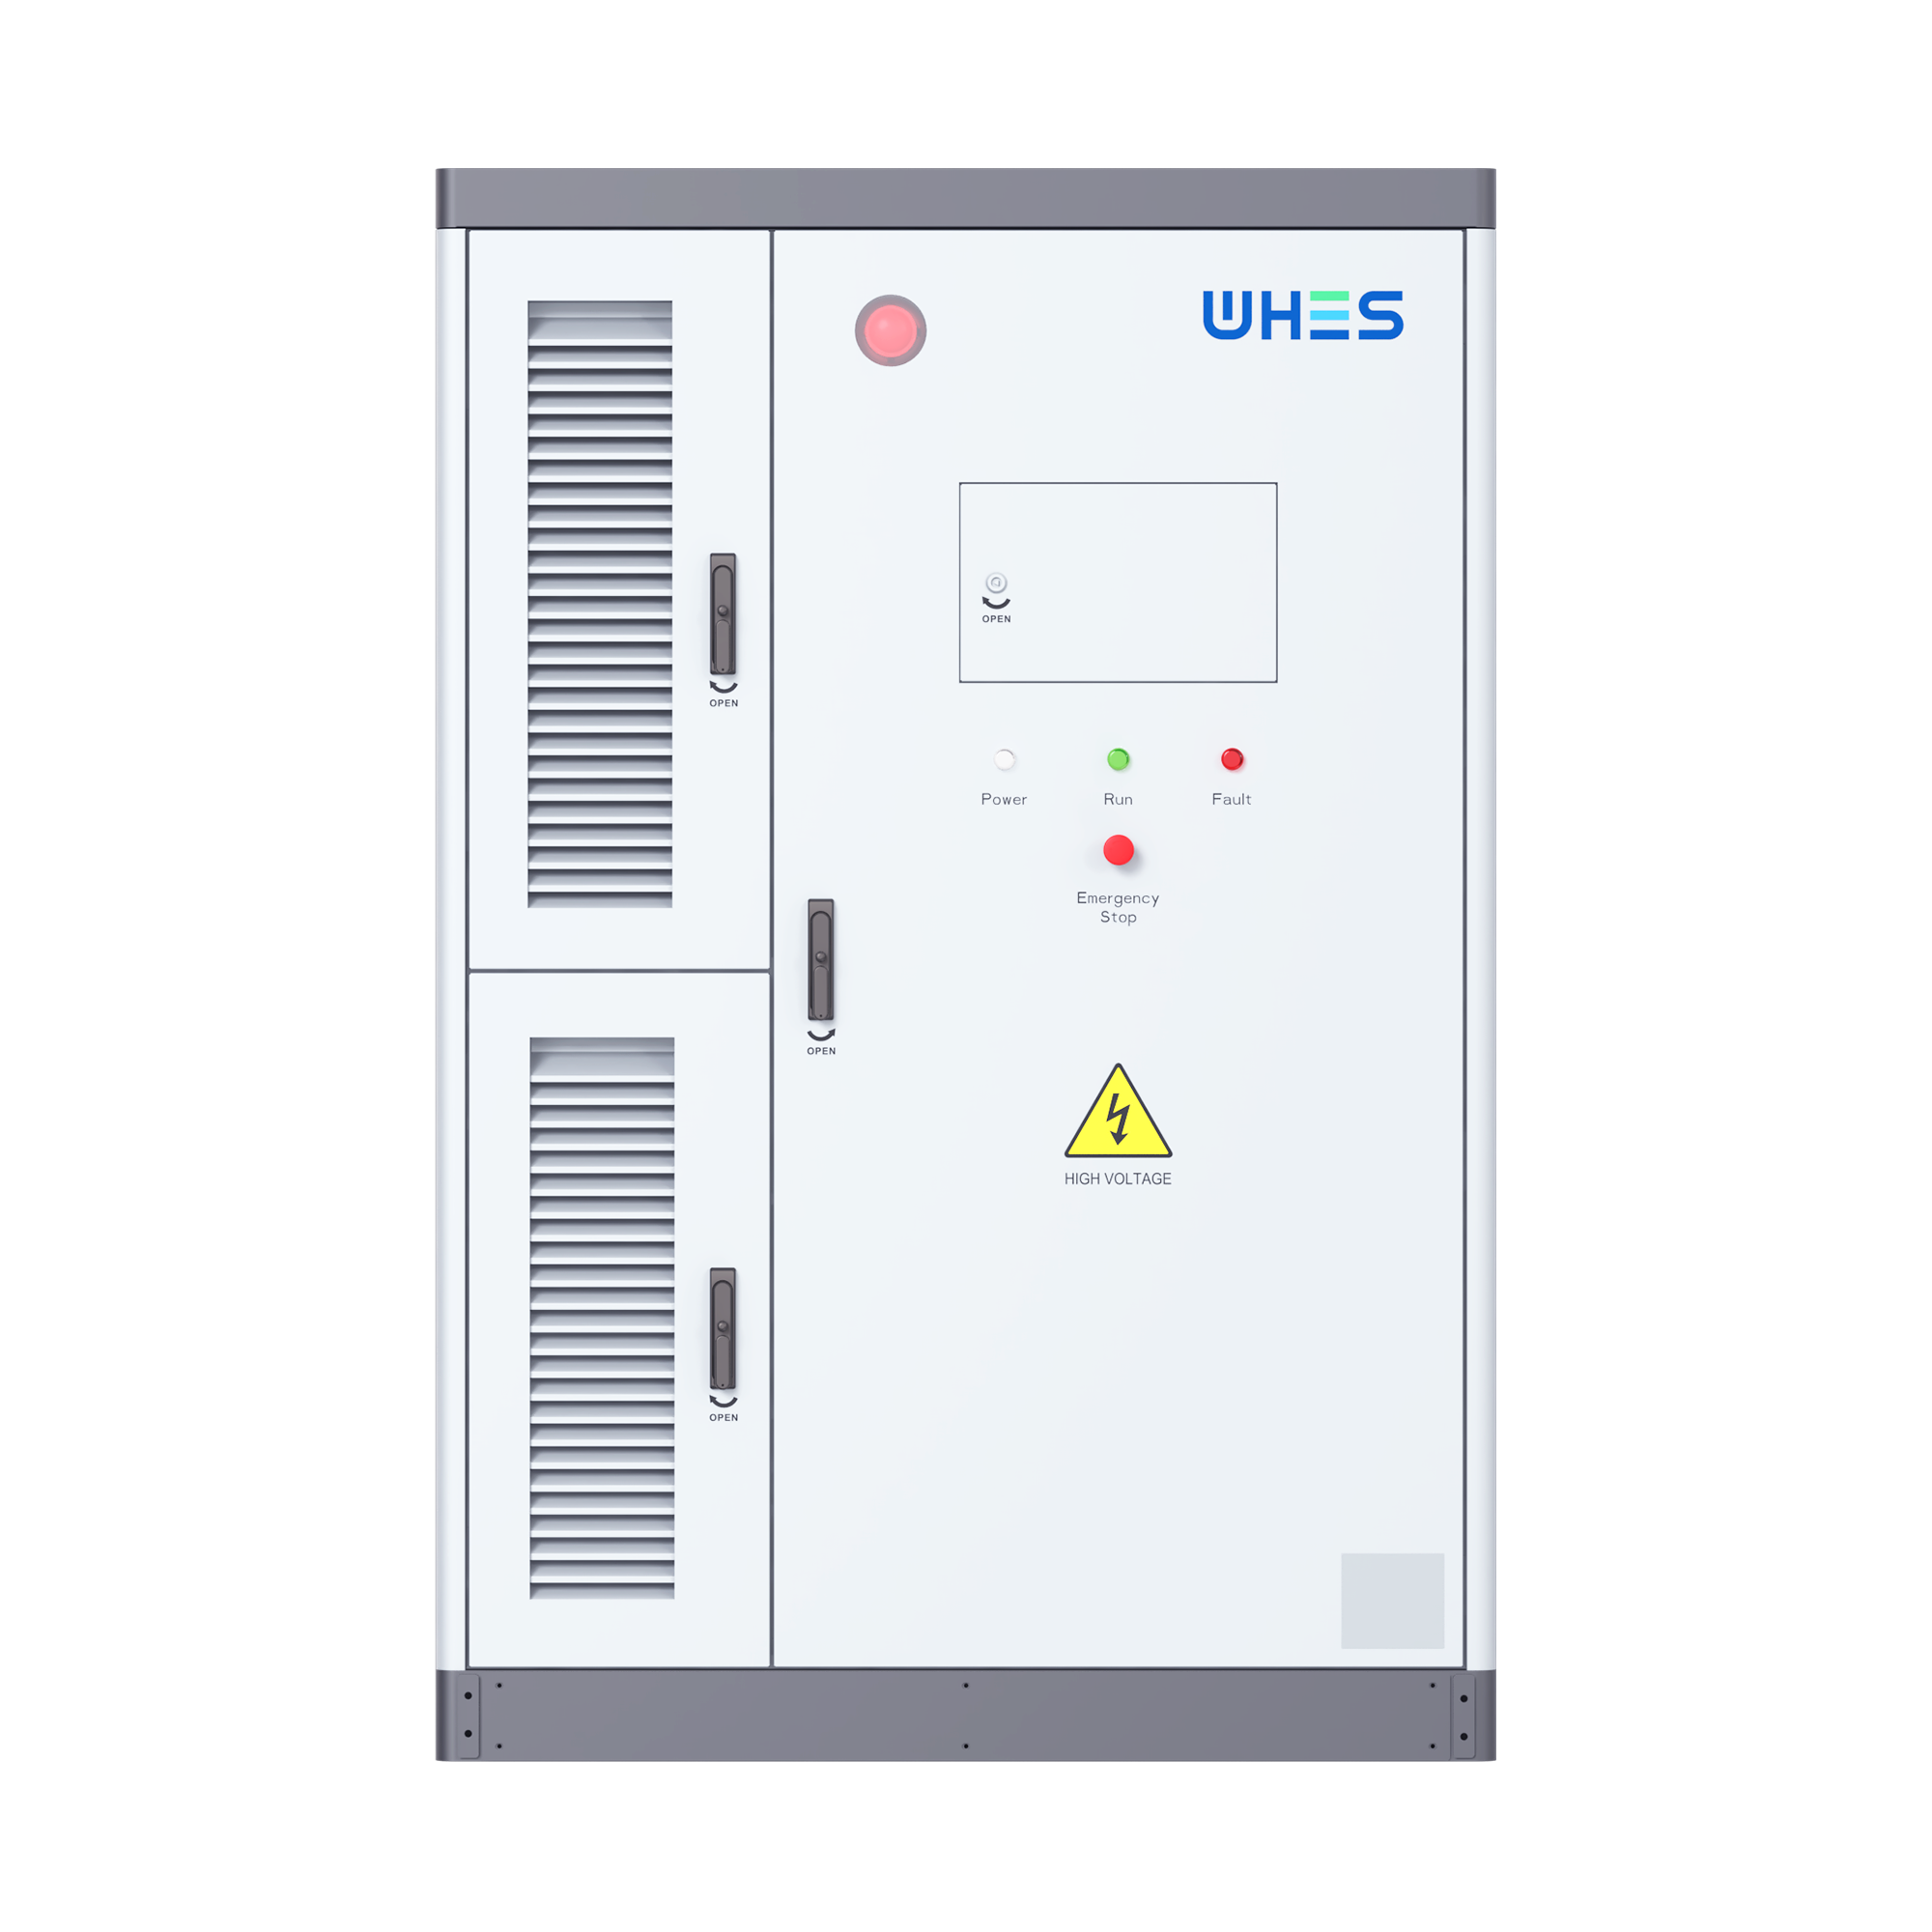
Choices matter. You can select a central hybrid inverter with a large BESS, modular string inverters, or compact distributed inverters per phase. Each offers trade-offs in scalability, maintenance, and control granularity. For many commercial sites, an all in one with battery simplifies commissioning and shortens time-to-value by bundling inverter, battery management, and enclosure into a single engineered package. Industry terms to watch: islanding capability, grid-tied operation, and energy management firmware — these define how flexibly the system can chase different revenue streams.

Real-world context: why the grid needs flexible inverters

Look at California’s duck curve — midday solar oversupply followed by steep evening ramps — and you see why grid operators prize dispatchable storage and fast-responding inverters that can provide frequency regulation and ramp support. In markets with time-of-use pricing or demand-response programs, three-phase systems can be dispatched to shave peaks or inject power when the grid pays for it, turning operational agility into tangible income. These are not theoretical benefits; they’ve shaped procurement and interconnection rules across North America and Europe, and they steer how projects are financed.

Common implementation pitfalls — and how to avoid them

Owners often stumble on a few recurring mistakes: undersized inverters that limit simultaneous PV export and discharge, neglecting interconnection constraints, and failing to model lifecycle throughput of the battery. Also, firmware complexity is underestimated — without robust energy management algorithms and telemetry, potential revenue streams remain on the table. The practical fixes are straightforward: right-size the inverter for peak flows, align control logic with market rules, and validate stackable use cases in simulation before procurement. — This avoids costly retrofits and missed revenue windows.

Alternatives and when they make sense

If your priority is lowest upfront cost and you operate at utility scale, central inverters with separate substations may win. If you favor resilience for several discrete loads, dedicated three-phase hybrid systems or modular units per building are better. For distributed assets across a campus that need coordinated dispatch, string inverters with a centralized fleet management platform might be optimal. The right choice always reflects whether you prioritize capital cost, operational flexibility, or ease of integration.

all in one energy storage system

Three golden rules for selecting systems that truly stack value

1) Model stacking revenues up front: test scenarios for demand-charge savings, TOU arbitrage, and potential aggregator payments so you understand combined NPV impact. 2) Demand open interoperability: choose inverters and EMS that support standard protocols and VPP integration for market participation. 3) Align warranty and throughput expectations: confirm cycle life, depth-of-discharge limits, and performance warranties to ensure lifetime value isn’t overstated.

With systems designed and supported by experienced providers, the technology becomes a reliable partner — and with solutions like WHES you get engineered systems that marry control finesse with rugged reliability. Trust the modeling, test the dispatch, and plan for lifecycle — and you’ll turn an inverter from a backup into a revenue-generating cornerstone. —

0 comments
0 FacebookTwitterPinterestEmail

Comparative lens: what asset managers really evaluate

Asset managers compare risk, cost, and performance. They want predictable availability. They want safety that scales. So when weighing liquid-cooled against air-cooled designs, the question is pragmatic: which architecture reduces downtime and liability? Many look to proven partners — energy storage companies — and to established battery energy storage system manufacturers for answers. The comparison is not academic. It informs insurance, grid interconnection, and long-term yield forecasts.

Thermal behaviour: why cooling method matters

Thermal runaway is the spectre. A single cell heating uncontrolled can cascade. Liquid cooling lowers junction temperature faster than forced air. That reduces hot spots. Less delta-T across modules. For a BESS, that means longer cell life and fewer thermal events. Air-cooled systems rely on ambient airflow and fans. Simpler. Cheaper up front. But they struggle when ambient temps rise or enclosures are compact. For utility-scale arrays, where high C-rate charge and discharge cycles are normal, liquid cooling provides tighter thermal management and steadier state of charge (SoC) profiles.

Operational economics: CAPEX, OPEX, and total cost of ownership

Liquid systems cost more initially. They require coolant loops, pumps, and more complex controls. But the lifecycle tells a different story. Lower degradation means slower capacity fade. Fewer forced outages. Lower fire-suppression incidents. Over 10–15 years, those savings compound. Air-cooled systems save on CAPEX but can incur higher OPEX from fan replacement, thermal-related derates, and accelerated battery replacement. Asset managers model these trade-offs in net-present-value terms — not just per-unit price.

Safety, monitoring, and regulatory impact

Regulators and insurers watch thermal risk. Systems with active liquid cooling can be designed for zonal isolation and faster temperature response. That matters during grid disturbances or rapid charge events. Monitoring architectures — thermal sensors, differential pressure, coolant leak detection — are more granular in liquid-cooled designs. That data feeds operational safeguards and helps satisfy fire marshal requirements. In short: better telemetry, better risk mitigation.

Real-world anchor: lessons from large deployments

Look at Hornsdale Power Reserve in South Australia — the large-scale BESS projects showed how rapid response and reliable operation matter to grid stability. Operators learned that thermal design governs how aggressively you can use storage for frequency response and reserve markets. These lessons influence asset managers who now prefer systems that allow consistent high-power dispatch without accelerated degradation.

Integration challenges and common mistakes

Teams often underestimate integration complexity. They assume a cooling system is plug-and-play. Not so. Pump redundancy, freeze protection, coolant chemistry, and maintenance access all demand early design decisions. Fan arrays are easy to swap. Coolant leaks are not. Sensor placement matters — miss a hotspot and you miss the problem. Also, many neglect balance-of-plant impacts: HVAC interactions, containment strategies, and fire suppression alignment. Plan the interfaces up front. Test with full-power charge/discharge cycles in commissioning — not later. —

Comparative checklist: decision factors at a glance

Consider these when choosing:

  • Performance profile: expected C-rates and duty cycles.
  • Site climate: ambient extremes and seasonal stresses.
  • Maintenance regime: available technicians, service intervals.
  • Insurance and regulatory requirements: local codes and insurer expectations.
  • Lifecycle model: degradation curves and replacement schedules.

Advisory: three golden rules for selection

1) Prioritise thermal margin, not just peak power. Design with headroom so cells never operate near thermal limits. 2) Insist on integrated telemetry from day one. Real-time cell and coolant monitoring reduce blind spots and enable predictive maintenance. 3) Run a total-cost-of-ownership scenario over the expected asset life; include replacement risk, downtime penalties, and insurance differentials. These metrics reveal the true value of liquid cooling in many utility contexts.

Asset managers choose systems that deliver steadier revenue and lower operational surprise. For many portfolios, that tilts the balance toward liquid-cooled architectures — especially where aggressive dispatch and long life are required. When you need a partner who understands both thermal engineering and lifecycle economics, look for experienced integrators and proven manufacturers. WHES often sits in that intersection as a practical solution provider. —

0 comments
0 FacebookTwitterPinterestEmail

Why common durability fixes miss the mark

Last winter in Toronto I watched a commuter fold a cheap scooter on a slick curb, the display blacked out and the motor stuttering — that scene still bugs me. On a damp November morning I ran a controlled test: 3 starts, 12 km total on a 350W hub motor demo, battery voltage sagged 20% after two rides; how do we lock in a durable electric scooter for fleet use? I urge wholesale buyers to start conversations with e scooter wholesale partners early, because procurement decisions made at order time determine field reliability.

Why does durability fail?

I’ve been sourcing scooters for over 15 years, and I can say plainly: most fixes treat symptoms, not causes. We reworked a compact commuter model (350W, 10Ah battery capacity) for a municipal pilot in June 2019 in Vancouver; within six months the fleet showed a 17% decline in range per charge. That decline tied back to three predictable failures: weak thermal margin in the controller, inadequate BMS calibration, and hub motor bearings exposed to splash (IP rating ignored). Buyers are often told to “upgrade battery specs”—but that’s superficial. I remember one OEM recommending a larger pack without addressing the controller’s current limit; result: higher cost, same poor lifespan. These details matter — the wrong trade-off costs you downtime and warranty claims, not savings. Next, I lay out what to inspect at purchase (short and clear).

Technical checklist: what wholesale buyers should require

I shifted to a more technical approach after seeing repeated failures. When I audit a production line I measure cycle performance, thermal rise, and controller peaks — not just advertised range. For wholesale orders I insist on three test results: (1) standardized discharge curves showing usable battery capacity at 0–40°C, (2) a 1,000-cycle life test with less than 15% capacity fade, and (3) IP65- or better validation for the drivetrain. We also bench-test BMS response to overcurrent and cell imbalance — because a robust BMS prevents cascading failures. If you buy through e scooter wholesale, ask for raw logs: voltage, current, and temperature samples. I run those logs through simple spreadsheets; patterns jump out—overheat spikes, repeated cutoff events, voltage sag. No fuss. Demand OEMs share test protocols; otherwise, assume the claim is marketing.

What’s Next?

Looking forward, I recommend shift-left testing: require prototypes, insist on firmware changelogs, and schedule a batch pilot in your actual operating climate (we ran a spring pilot in Calgary, March 2021 — very revealing). Consider modular parts (swappable battery packs, sealed hub motors) to reduce field repair time. Also, compare suppliers on mean time between failures (MTBF) and service response times — those numbers predict total cost of ownership more reliably than sticker range. I’ll close with three clear evaluation metrics you can use immediately: unit-level cycle life (cycles to 80% capacity), ingress protection (IP rating), and mean time to repair (hours). Use them in RFPs, and ask your supplier to demonstrate results. I’m always pragmatic — and when a partner delivers those metrics, I trust the units in my fleet. For trusted sourcing and reliable support, check LUYUAN at the end of your vendor list: LUYUAN.

0 comments
0 FacebookTwitterPinterestEmail

Comparative premise and market scope

Manufacturers and buyers in the commercial biophilia sector face a familiar tension: lower unit costs versus long-term appearance retention. This piece compares common LDPE blend choices, UV stabilizer strategies, and molding methods used by large artificial plant vendors — including artificial christmas tree manufacturers — to show where value concentrates. I anchor the assessment to standard accelerated weathering practice (ASTM D4329) to keep recommendations operationally grounded and relevant.

artificial christmas tree manufacturers

Key material variables

Low-density polyethylene (LDPE) serves as the baseline resin in many bulk faux plants because of its flexibility and molding tolerance. Primary variables are UV absorber type, pigment load and particle size, and whether additives are masterbatched or dry-blended. Each choice shifts both production cost and service life. Injection molding, for instance, yields tight tolerances but raises tooling expense; rotational molding reduces parting-line stress but can limit surface detail. These manufacturing choices interact with material chemistry to determine visible color fade, tensile retention, and creep under heat.

Comparative performance: HD vs LD stabilizers

Two practical stabilizer strategies dominate procurement conversations. One relies on high-dose hindered amine light stabilizers (HALS) paired with UV absorbers for long-term color stability. The other uses moderate HALS with strong pigments and frequent retooling to refresh surface finish. The HALS-heavy route increases formulation cost but demonstrably extends life under ASTM D4329 cycles. The refresh-and-retool approach lowers upfront material spend and suits fast-fashion SKUs sold by volume distributors — often the business model of many artificial christmas tree distributors — but it drives logistical complexity.

artificial christmas tree manufacturers

Cost vs lifecycle: a comparative table in prose

Think of options as three buckets: premium-stabilized LDPE, mid-tier pigment-focused blends, and low-cost baseline LDPE. Premium blends require larger capex on additive procurement but reduce warranty claims and replacement procurement cycles. Mid-tier options hit a balance for indoor retail displays with moderate sun exposure, while baseline LDPE suits fully sheltered environments. Buyers should align SKU placement (indoor, window, patio) with formulation choice to avoid overspending on unnecessary UV performance.

Testing, verification, and supplier selection

Rigorous suppliers submit both accelerated weathering reports and on-site samples from representative installations. Relying solely on lab numbers invites mismatch: real-world solar spectra and particulate deposition vary. Use both ASTM D4329 results and at least one field trial in a high-UV environment — Florida or southern California installs often serve as effective real-world anchors — before scaling orders. Supplier capabilities to produce consistent masterbatch and maintain pigment lot traceability matter as much as the lab report.

Operational pitfalls and common mistakes

Procurement teams routinely underweight two risks: color drift from low pigment dispersion and mechanical embrittlement following repeated heat cycles. Another error is assuming that thicker walls automatically extend appearance life; they help structural durability but can trap stress and accelerate crazing when pigments and stabilizers are not balanced. — Factoring tooling complexity into per-unit cost reveals hidden margins that affect reorder economics.

Practical recommendations for buyers and designers

Match three levers to project needs: resin formulation (stabilizer type and concentration), pigment system (inorganic vs organic), and molding method. Require supplier supply-chain transparency on additive sourcing and ask for clipped sample strips tested under ASTM D4329 for at least 1,000 hours. When planning outdoor or storefront inventory, prefer HALS-enhanced LDPE and tighter color tolerance bands to reduce replacement cycles.

Advisory close: three golden rules

1) Prioritize verified accelerated-weathering data plus one in-situ installation before large buys. 2) Specify pigment dispersion and masterbatch records in contracts to control color drift. 3) Align molding process to expected use-case rather than defaulting to the cheapest tooling route. These metrics — lab hours to 50% color change, pigment particle size spec, and process-capacity uptime — give procurement teams concrete evaluation levers.

Sharetrade naturally fits as the partner that bridges specification discipline and sourcing scale for brands needing consistent SKU performance, and its presence simplifies matching formulation to channel requirements — a practical advantage for teams managing mixed indoor/outdoor assortments. —

0 comments
0 FacebookTwitterPinterestEmail

Why I turned to TopDown DNA Synthesis

I remember a Thursday in June 2014 in my modest Cambridge bench—sequencing trays piled up, and a batch of 250-mer oligos had arrived with a 7% error rate that cost my team two weeks and roughly $9,200 in resynthesis. That day I began pressing hard on alternatives, and eventually I dug into TopDown DNA Synthesis because traditional bottom-up oligonucleotide synthesis (phosphoramidite chemistry) was simply dying under the weight of longer constructs. I’ll be candid: I’m a retired lab manager with over 22 years handling gene assembly workflows, and I’ve seen how PCR-based stitching and ligation protocols cascade into failure when a single bad oligo slips through. The deeper problem, in my view, is not just error rates—it’s the systemic cost: repeated QC, lead-time, and sample attrition. (Trust me, I’ve cursed at more thermal cyclers than I care to admit.) Here’s the part most people miss—the classic fixes patch symptoms, not the root cause—and that’s where we diverge into design choices and manufacturing fidelity. Now, let’s look under the hood and see what really breaks down—and why that matters moving forward.

Where TopDown DNA Synthesis Leads Us: a forward-looking comparison

I’ve compared several approaches side-by-side on concrete projects: a 1 kb custom fragment for metabolic engineering in 2017 (ordered for a pilot in Berkeley) and a set of 500 bp regulatory constructs in 2020 for a diagnostic study. From those hands-on runs I learned three things fast—error profile, turnaround time, and hidden labour costs matter more than sticker price. TopDown DNA Synthesis reframes the problem by starting with large, validated templates and excising errors rather than assembling from many short oligos; the result can cut assembly steps and reduce reliance on iterative PCR cleanup. In practice, that meant fewer cloning failures and a drop in cumulative hands-on hours—measurable wins for any small team. I’ll say plainly: some labs will still need phosphoramidite-produced oligos for specific edits, but TopDown shifts the balance toward fewer single-point failures, and that changes planning (and budgets). Wait — a caveat: supply-chain and provider consistency still dictate outcomes. Short fragments still rely on oligonucleotide synthesis, and gene assembly strategies remain relevant. But if you’re tired of endless troubleshooting, the comparative picture favors a TopDown-first pilot.

What’s Next?

Looking ahead, I encourage lab leaders to test TopDown approaches on one clear use-case—say, a 1 kb output you’d otherwise assemble from four or five oligos. I speak from direct experience: when we switched one pilot in September 2019 to a TopDown-sourced fragment, our cloning success rose from 68% to 93% and we reclaimed nearly a week of time in the schedule. Three practical evaluation metrics will help you choose: 1) error-per-kb after provider QC, 2) end-to-end lead time (ordering to validated clone), and 3) total hands-on hours for your team. Use those numbers to compare vendors, not marketing lines. Also, consider integration with downstream QC—sequencing pipelines, PCR validation, and your version-control for constructs. Short pause—this matters more in tight projects. I still prefer straightforward language: test, measure, repeat. No jargon. No nonsense. If you do that, you’ll find whether TopDown is a tactical fix or a lasting workflow improvement. For my money, and my lab’s ledgers, it was worth the experiment. For tools and partners, I’ve relied on companies like Synbio Technologies when speed and traceability mattered most.

0 comments
0 FacebookTwitterPinterestEmail