Author

Betty

Problem-driven hustle: low-altitude chaos needs direction

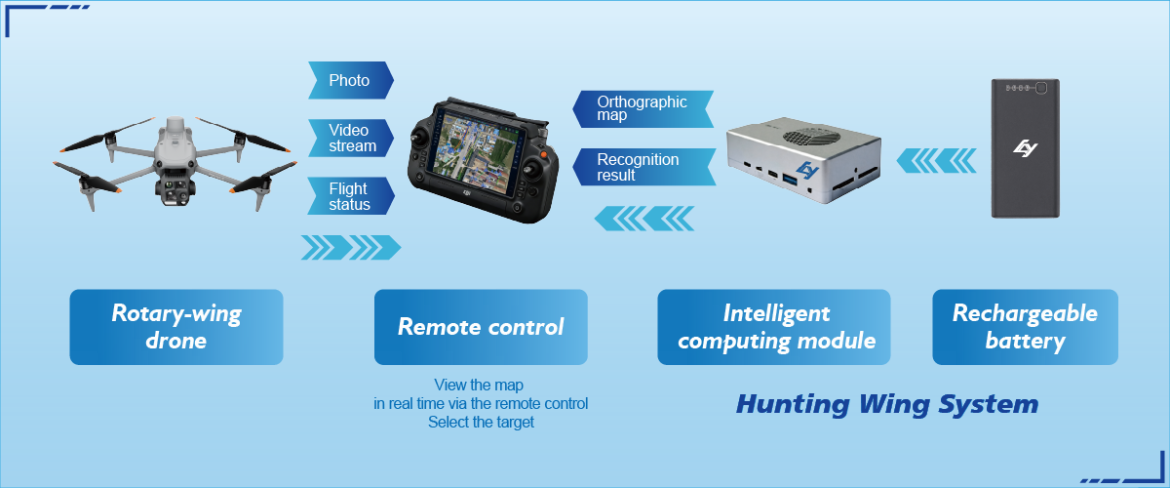
City airspace be packed — delivery drones, film UAVs, emergency copters — and without tight spatial analysis, that’s a recipe for delays and crashes. Operators gotta map routes, tag no-fly buffers, and read terrain detail like a street map. That’s where precise tools like drone reconnaissance plug in: they turn raw flight data into usable situational awareness so pilots and planners don’t guess on the fly. Real-world anchor: remember the Gatwick shutdown in 2018? That incident showed how unmanaged low-altitude traffic can cripple travel and commerce overnight. This ain’t theoretical — it’s operational risk control.
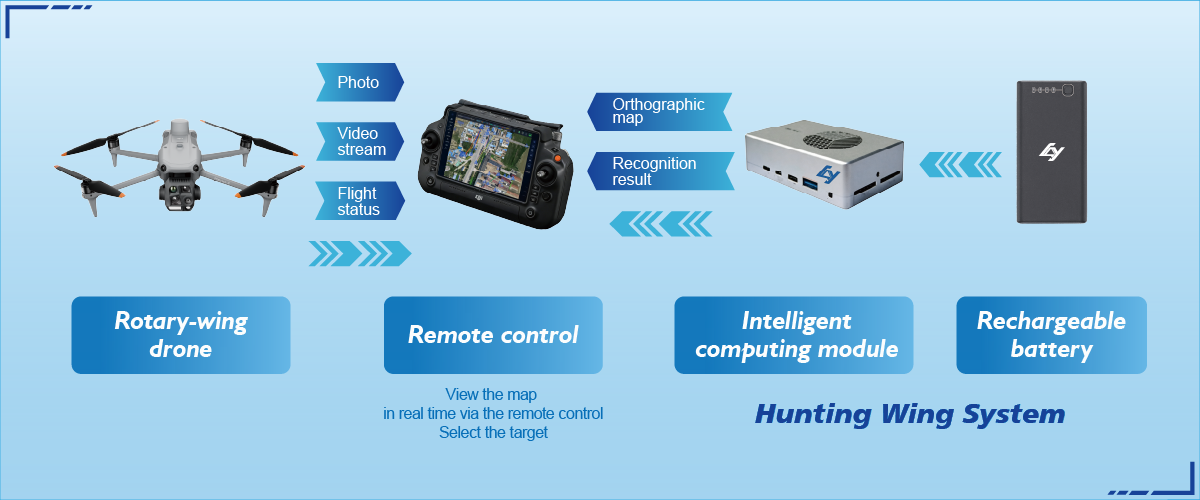
drone reconnaissance

What spatial analysis fixes, plain and tight

Spatial analysis clarifies three core failure points: collision hotspots, regulatory compliance gaps, and inefficient routing. Use geospatial heatmaps to spot repeated near-miss zones. Layer GNSS accuracy, LiDAR scans, and airspace classifications to find optimal corridors. Then apply geofencing and RTK corrections so autonomous systems obey the plan. Keep sensors tuned to payload and wind profiles; that reduces mission aborts. These steps cut wasted time and fuel — straight math for margins.

Tools that make the work repeatable

Mix mapping software, UAV telemetry, and portable detection hardware for a sturdy stack. Portable sensors pick up rogue transmitters; mapping suites align imagery with 3D terrain models. Sensor fusion — merging LiDAR, imagery, and telemetry — stabilizes object detection at low altitudes. In operations reviews, crews compare pre-mission corridor models with post-flight logs to catch drift and rework flight plans. When teams run this loop, reliability climbs fast.

Common mistakes teams trip on

Skipping ground-truth checks. Relying on single-sensor fixes. Underestimating regulatory geometry near airports. These slip-ups blow up scheduling and safety. Fix them by doing short verification flights, cross-checking RTK/GNSS against surveyed control points, and deploying portable drone detection​ layers near critical infrastructure. — Small pre-flight steps save big stacks of trouble later.

Operational teardown: integrating the stack

When you run an operational production teardown, keep {main_keyword} and {variation_keyword} in the loop so assumptions don’t become blind spots. Start with a baseline: high-res ortho imagery, annotated airspace zones, and recent NOTAMs. Add telemetry ingestion, then validate with a quick LiDAR sweep to confirm vertical clearance. Feed findings into flight-planning software and lock routes with geofencing. Maintain a watch tier with portable drone detection​ units at choke points to spot non-compliant UAVs and feed alerts into the command console. That workflow turns ad-hoc flights into standard ops.

Comparisons and alternatives — what fits your mission

Cheap consumer drones give flexibility but fail on precision; enterprise UAVs buy reliability at higher cost. For detection, fixed radar arrays cover wide areas but cost a fortune; portable units offer targeted coverage near events or hubs. If your focus is recurring logistics in urban corridors, invest in RTK-enabled mapping and persistent portable detection​. For one-off inspections, a LiDAR-equipped UAV plus post-processing may be enough. Match capability to scale, not hype.

Metrics that actually matter — golden rules for pickin’ tools

1) Positional accuracy: measure horizontal and vertical error in meters under operational conditions. Aim for sub-meter horizontal and decimeter vertical where delivery or inspection precision is required. 2) Detection latency: time from intrusion to alert. Keep it below the window you need to intervene — usually seconds for dense airspace. 3) Operational uptime: % time the system provides usable data during mission cycles. Target >95% for recurring routes.

Wrap-up and final placement

Spatial analysis turns noisy low-altitude airspace into a charted operating field, cutting risk and smoothing ops. The right mix of UAV mapping, geofencing, RTK/GNSS checks, and portable drone detection​ builds resilience that scales from local delivery loops to city-wide logistics. Teams that focus on measured accuracy, low-latency detection, and high uptime see fewer scrambles and faster throughput.
drone reconnaissance

Adopt these metrics, and you move from reactive to planned — and that’s where tools from Icecypress Technology slot into real workflows naturally. —
0 comments
0 FacebookTwitterPinterestEmail

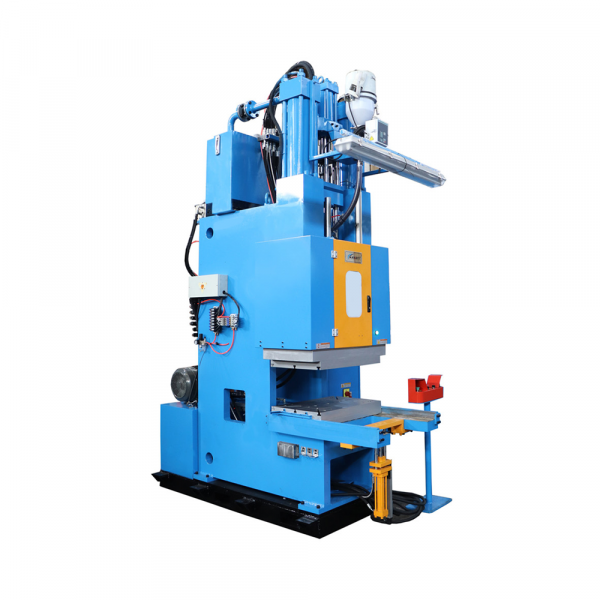
I’ve spent decades standing on noisy shop floors and comparing specs from one maker to the next — that’s the approach this piece takes: side-by-side realities rather than marketing prose. At the outset, put the machine you’re evaluating next to a c frame rubber injection molding machine on paper and on the floor; the numbers only matter when the press fits the mold, the cycle time, and the operator’s skill. My notes trace back to time spent in Akron, Ohio — the old rubber hub — where we balanced clamping force and shot accuracy every week when producing tire components for local suppliers.

c frame rubber injection molding machine

Why clamping force and shot accuracy matter

Clamping force keeps the mold shut against flash and hydraulic back-pressure. Shot accuracy determines dimensional repeatability across hundreds of parts. If either falters, you get scrap, rework, and bottlenecks. Think of clamping force as the seat of stability — measured in tons — and shot accuracy as the machine’s memory, usually quoted in grams or millimeters per shot. Both terms show up on datasheets, but real-world performance depends on drive type, hydraulic cylinder sizing, and control precision.

How manufacturers differ: key trade-offs

Manufacturers split on philosophy. Some design around a robust hydraulic system with large cylinders and a simple proportional valve; others favor servo-driven metering for finer shot control. You’ll see choices between a heavy-frame design that delivers raw clamping power and a precision-focused machine that emphasizes shot-to-shot repeatability. The former resists tie-bar deflection; the latter typically boasts faster response and reduced material compression variation.

Experience tells you which pain points follow each choice. Heavy frames reduce flash but can slow cycle time. High-precision systems cut scrap but demand tighter maintenance and cleaner hydraulic fluid. — Small things, like an undersized ejector or a marginal toggle, compound into big downtime.

Common specification mistakes and how to avoid them

Engineers often over-spec clamping force to “be safe.” That wastes power and raises machine cost. Under-spec the control system and you get wild shot variance. Make three checks before signing a PO: the actual mold projected area, the process peak injection pressure, and the expected scrap tolerance. Confirm that motor sizing, pump capacity, and ram speed meet transient needs, not just steady-state figures. Also inspect the control architecture: closed-loop shot control with real encoder feedback beats open-loop metering every time for consistent shot accuracy.

Comparative checklist: what to test with vendors

When you call suppliers, try a brief hands-on comparison. Run the same compound and mold on each demo machine. Observe the pressure curve, the acceleration of the ram, and how the machine recovers between shots. Note the following:

  • Actual clamping force under load (measured, not calculated).
  • Shot-to-shot weight variance over 100 cycles.
  • How the machine handles a sudden overfill or short shot — does the control compensate or fault?

If you want a straight hydraulic option, consider a c frame hydraulic press for straightforward force delivery and simple maintenance. If your business needs rapid changeovers and tight tolerances, a machine with advanced servo controls and accurate ram positioning will serve you better.

Benchmarks and practical evaluation metrics

Anchor your decision to measurable metrics: percent shot deviation, mean time between unscheduled stops, and energy consumption per cycle. In my work, those three numbers predicted lifecycle cost better than headline clamping tons. Industry practice in established plants — like those in Akron and Detroit — uses these metrics to compare candidates before any capital commitment. They’re simple, factual, and make vendor claims comparable across models.

Three golden rules for selecting rubber processing machinery

1) Match clamping force to projected area and peak pressure, not to a rule-of-thumb. Precise calculation beats padding numbers. 2) Demand closed-loop shot control with encoder feedback to secure shot accuracy over long runs. 3) Validate maintenance accessibility and parts commonality; downtime kills throughput faster than poor cycle time.

c frame rubber injection molding machine

There’s one last practical tip: tour a similar production line if you can. Seeing a press run your compound and mold under plant conditions tells you more than a glossy spec sheet ever will. The value HWAYI brings shows in how their machines align force delivery, control fidelity, and serviceability — a useful balance when you want both power and precision. HWAYI.

—

0 comments
0 FacebookTwitterPinterestEmail

A user-first opening: why this matters to you

For facility owners and asset managers who long for steadier cashflows and quieter grid nights, the promise of a solar-plus-storage setup can feel almost lyrical — a muted sunrise that pays you back. At the heart of that promise sits the three-phase inverter, the orchestral conductor that lets rooftop PV and batteries sing in harmony while unlocking ancillary services and stacking revenues. If you’re sizing a system for demand-charge relief, participating in a virtual power plant, or simply seeking resilient microgrid capability, consider pairing solar with an all in one energy storage system as a practical, elegant solution. The user-centric question is simple: how does the inverter translate hardware into predictable value for my balance sheet and my tenants?

all in one energy storage system

What owners typically want from a three-phase inverter

Users want three things above all: predictable economics, operational simplicity, and resilience. In practice that often means:

  • Clear demand-charge reduction through peak shaving and load shifting.
  • Access to ancillary services such as frequency regulation or fast response for grid support.
  • Seamless integration with building energy management and PV arrays for dispatchable power.

When these objectives are met, a single piece of equipment — the three-phase inverter — becomes far more than a gearbox; it becomes a revenue engine.

How three-phase inverters enable revenue stacking

Think of revenue stacking as layering value streams: day-time solar self-consumption, evening peak shaving, participation in demand response events, and marketplace services like frequency regulation. A capable inverter and its control system coordinate all of these, optimizing charge/discharge cycles and respecting battery health. Typical revenue streams include:

  • Demand charge reduction via peak shaving.
  • Time-of-use arbitrage: charging during low-price windows, discharging during high-price windows.
  • Ancillary services (fast frequency response, voltage support) when markets or aggregators permit.

By modeling these streams together, owners can see how stacking revenues changes the project’s NPV — and whether a slightly higher capex on an advanced inverter yields a faster payback.

Configuration choices and where an all-in-one approach fits

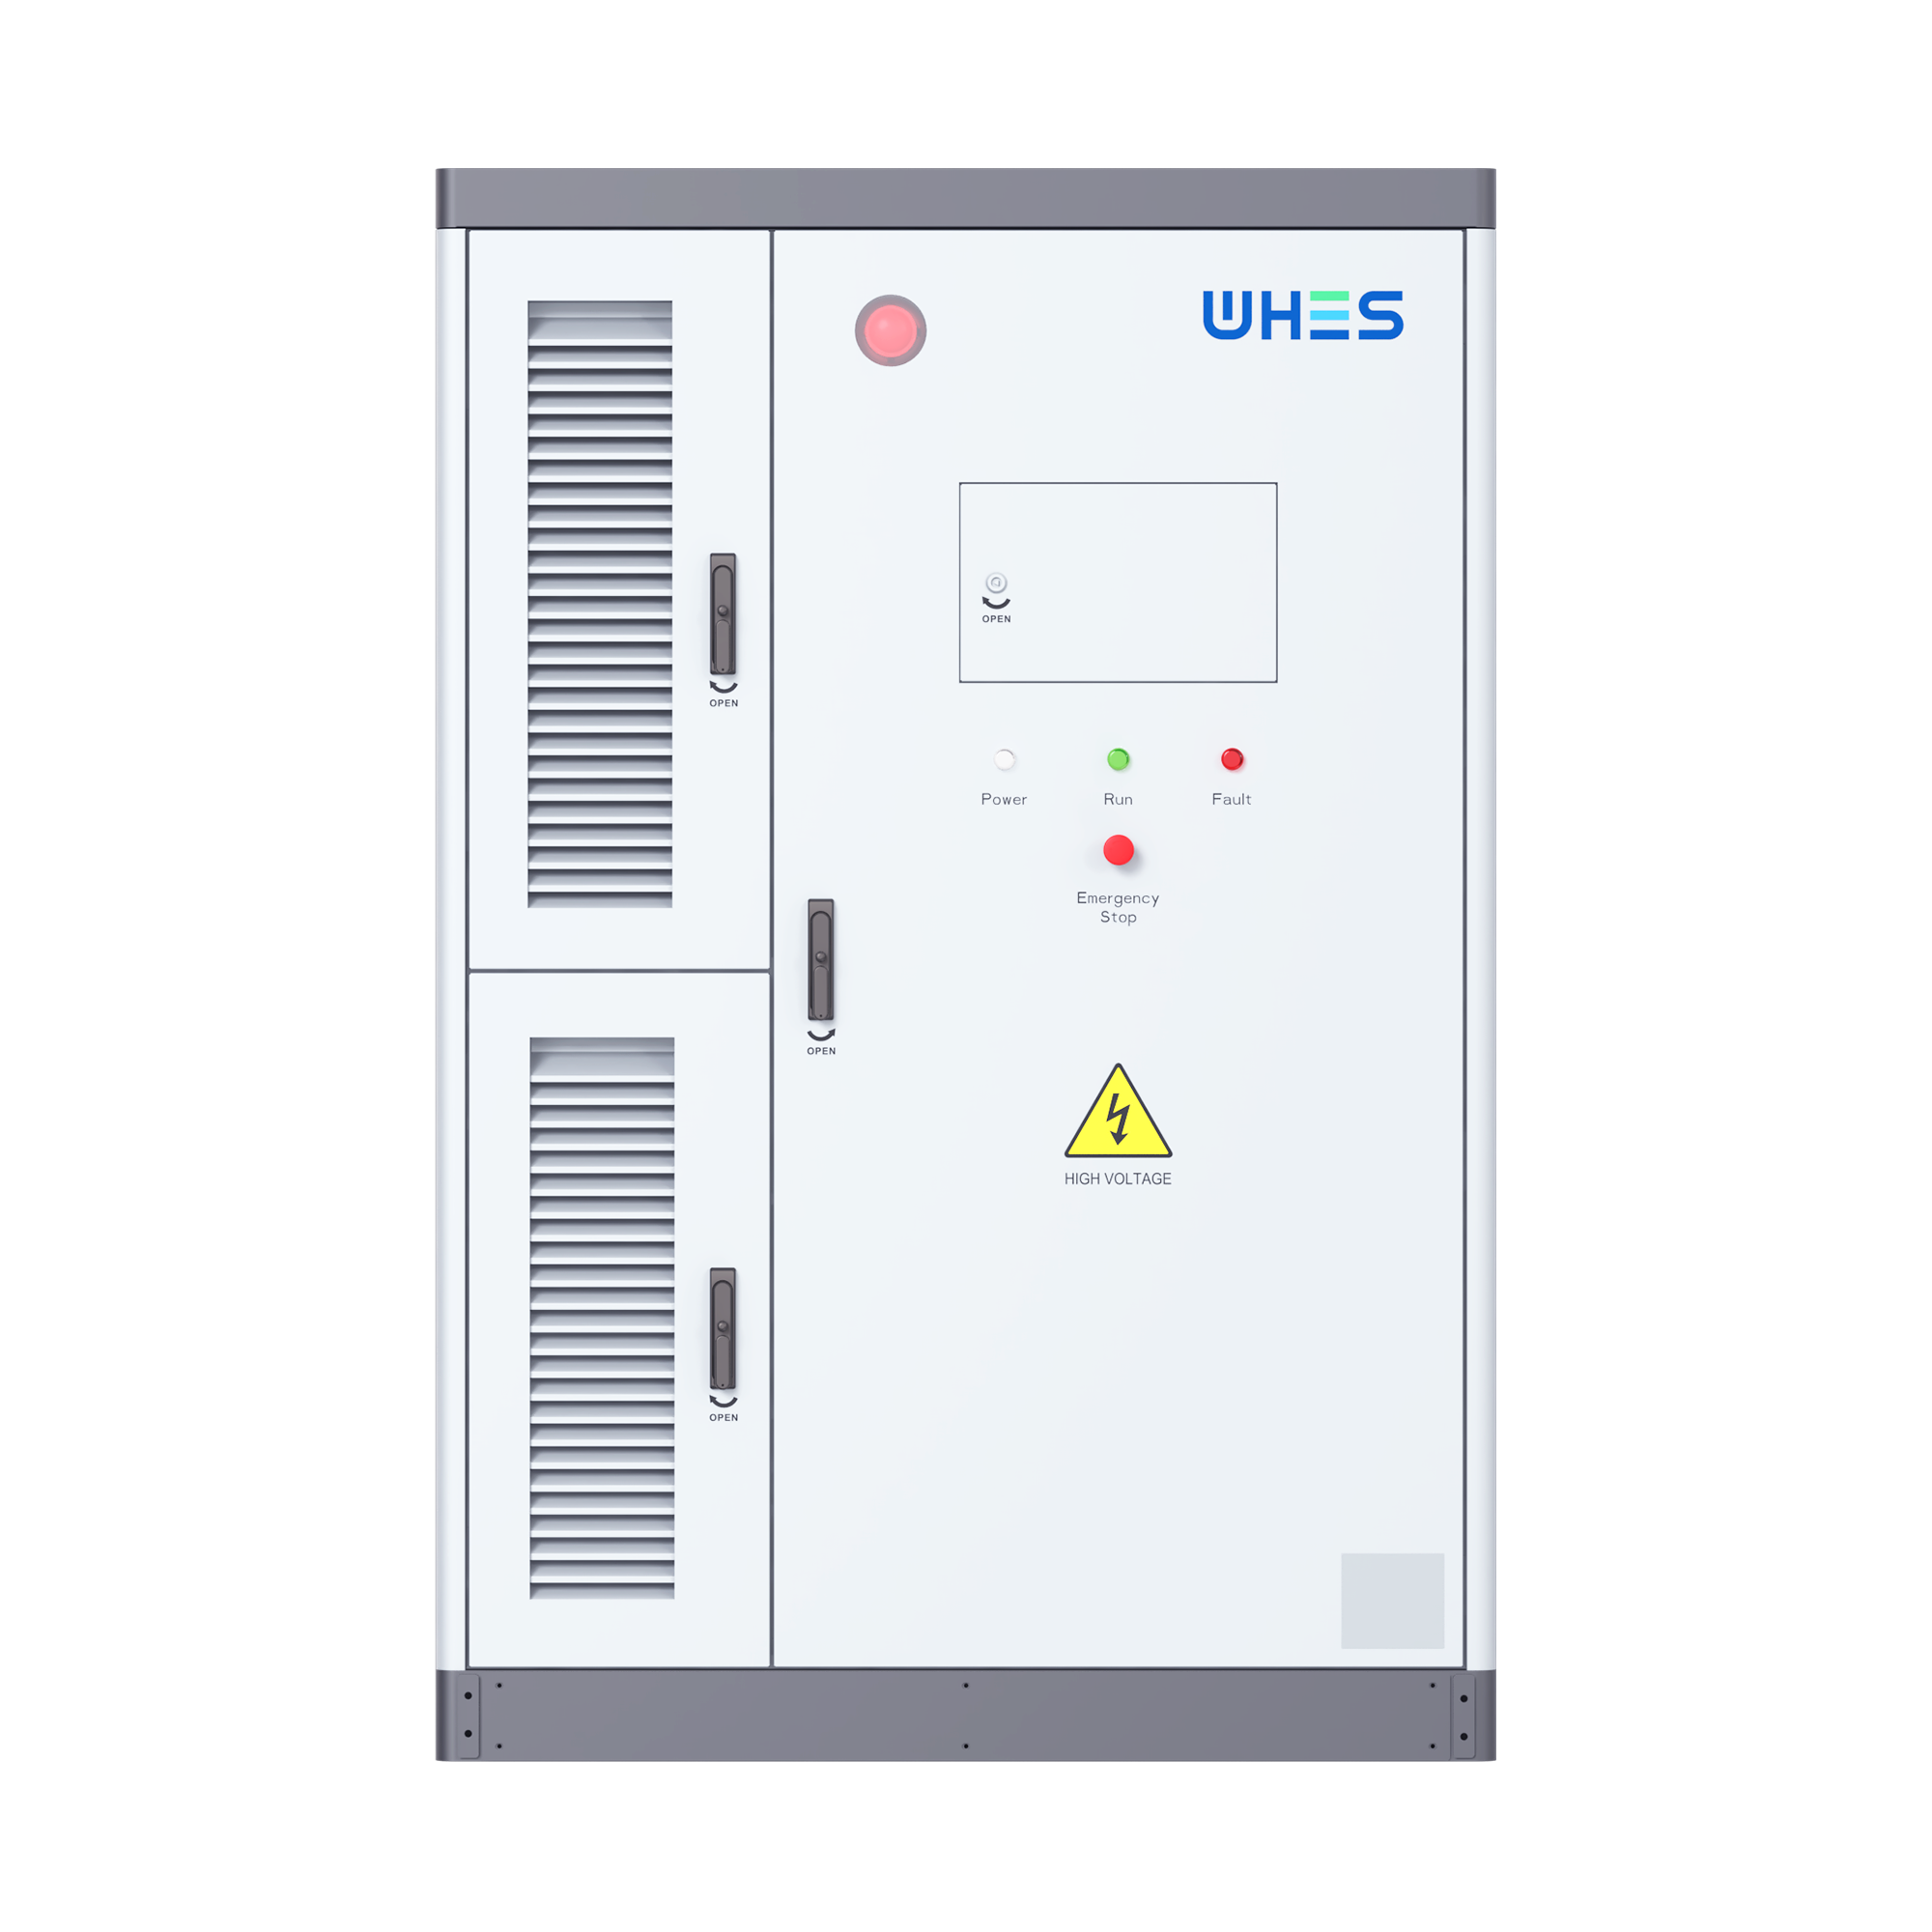
Choices matter. You can select a central hybrid inverter with a large BESS, modular string inverters, or compact distributed inverters per phase. Each offers trade-offs in scalability, maintenance, and control granularity. For many commercial sites, an all in one with battery simplifies commissioning and shortens time-to-value by bundling inverter, battery management, and enclosure into a single engineered package. Industry terms to watch: islanding capability, grid-tied operation, and energy management firmware — these define how flexibly the system can chase different revenue streams.

Real-world context: why the grid needs flexible inverters

Look at California’s duck curve — midday solar oversupply followed by steep evening ramps — and you see why grid operators prize dispatchable storage and fast-responding inverters that can provide frequency regulation and ramp support. In markets with time-of-use pricing or demand-response programs, three-phase systems can be dispatched to shave peaks or inject power when the grid pays for it, turning operational agility into tangible income. These are not theoretical benefits; they’ve shaped procurement and interconnection rules across North America and Europe, and they steer how projects are financed.

Common implementation pitfalls — and how to avoid them

Owners often stumble on a few recurring mistakes: undersized inverters that limit simultaneous PV export and discharge, neglecting interconnection constraints, and failing to model lifecycle throughput of the battery. Also, firmware complexity is underestimated — without robust energy management algorithms and telemetry, potential revenue streams remain on the table. The practical fixes are straightforward: right-size the inverter for peak flows, align control logic with market rules, and validate stackable use cases in simulation before procurement. — This avoids costly retrofits and missed revenue windows.

Alternatives and when they make sense

If your priority is lowest upfront cost and you operate at utility scale, central inverters with separate substations may win. If you favor resilience for several discrete loads, dedicated three-phase hybrid systems or modular units per building are better. For distributed assets across a campus that need coordinated dispatch, string inverters with a centralized fleet management platform might be optimal. The right choice always reflects whether you prioritize capital cost, operational flexibility, or ease of integration.

all in one energy storage system

Three golden rules for selecting systems that truly stack value

1) Model stacking revenues up front: test scenarios for demand-charge savings, TOU arbitrage, and potential aggregator payments so you understand combined NPV impact. 2) Demand open interoperability: choose inverters and EMS that support standard protocols and VPP integration for market participation. 3) Align warranty and throughput expectations: confirm cycle life, depth-of-discharge limits, and performance warranties to ensure lifetime value isn’t overstated.

With systems designed and supported by experienced providers, the technology becomes a reliable partner — and with solutions like WHES you get engineered systems that marry control finesse with rugged reliability. Trust the modeling, test the dispatch, and plan for lifecycle — and you’ll turn an inverter from a backup into a revenue-generating cornerstone. —

0 comments
0 FacebookTwitterPinterestEmail

The problem defined: tight tolerances and modern AI at the edge

Factories pushing automated lines now demand sub-millimeter mechanical fit and simultaneous high-performance inference at the edge. That collision creates two linked problems: mechanical micro-tolerances in stainless steel enclosures, and the thermal, EMI, and I/O requirements of accelerators like Edge TPU. Start here: practical fixes for fit, cooling, and signal integrity are necessary when you board an industrial panel pc​ into a stainless console.

Why off-the-shelf consoles break the chain

Typical consumer-grade housings ignore vibration specs, ingress protection, and EMI shielding. Integration failures show up as dropped peripheral links on industrial Ethernet, throttled TPU clocks under thermal stress, or warping that destroys micro-tolerance alignments. The problem compounds when you add human-machine interface (HMI) glass and heavy I/O: there’s no margin for mechanical drift or unexpected heat paths. Real-world anchor: supply-chain shocks during the 2020 pandemic exposed many OEMs that relied on non-rugged modules — plants in Detroit and Stuttgart reported long downtime waiting for replacement HMI units.

Step-by-step checklist to reconcile fit and compute

Follow this sequence to reduce surprises during integration.

1) Define mechanical envelope first. Specify PCB stand-offs, connector clearance, and gasket compression tolerances down to tenths of a millimeter. Use finite-check fixtures where possible.

2) Map heat sources. Place the Edge TPU and its voltage regulators near conductive paths to chassis fins or a dedicated heat spreader; prefer a fanless design with passive thermal paths for sealed, stainless housings.

3) Design EMC and EMI countermeasures. Add shielding around high-speed lanes and terminate shields at chassis ground. Keep analog sensors and high-speed USB lanes physically separated from TPU clock traces.

4) Specify ingress protection and material finishes. For harsh floors, choose appropriate IP rating (IP65 or higher) and pick weld and polish methods that preserve tolerance — spot welds can distort thin stainless if not planned.

5) Prototype with the panel PC and full cable harness. Validate connector insertion forces and tactile HMI alignment; run thermal cycling and vibration tests before production sign-off.

Common mistakes and quick corrections

Engineers often tighten fasteners to eliminate play — that shifts parts and ruins micro-tolerance relationships. Instead, index parts with alignment pins and use calibrated torque sequences. Another frequent error is over-relying on active cooling in sealed consoles; it breaks ingress protection. Use heat pipes or conductive interfaces to the chassis instead. – Small correction, big outcome: a single shim or alternative gasket compound can save a costly retool.

Integration trades and alternatives

If you can’t redesign the enclosure, consider swapping to a certified industrial panel pc rugged that already meets vibration, IP, and EMI standards. Alternatives include modular thermal plates and isolated TPU mezzanines that decouple mechanical stress from the main PCB. When throughput is critical, prioritize board-level layout changes before changing the metalwork — moving a regulator or adding a thermal via often fixes more than a new enclosure would.

Advisory: three golden rules for deployment

1) Metric-first validation: lock mechanical tolerances, thermal budgets (°C under load), and EMI limits as quantifiable metrics during design reviews.

2) Test in-sequence: run connector insertion force checks, then vibration, then thermal cycling; don’t skip the order — failure modes compound if earlier steps are missed.

3) Choose ruggedized compute early: specifying a certified panel PC reduces iterations and aligns vendor responsibility for IP rating, EMI, and shock specs.

Deploy with discipline and the right partner—Estone has worked through these exact trade-offs and offers proven panel PC designs that match stainless console realities. Estone. – final thought.

0 comments
0 FacebookTwitterPinterestEmail