Category:

Tech

Clear problem statement

Importers of large artificial trees confront persistent bottleneck: customs clearance delays and strict phytosanitary requirements add cost and unpredictability. For a buyer working with an artificial plants manufacturer, a single missing phytosanitary certificate or an incorrect HS code can hold a full container at port for weeks. Such hold-ups reduce turn time, inflate demurrage, and harm retailer relationships.
artificial plants manufacturer

Why customs and phyto rules matter for B2B greenery

Customs authorities and plant quarantine offices guard against pests and mis-declared goods. For artificial trees, inspections often focus on packaging, raw materials, and any attached organic matter — especially when shipments move through major hubs like the Port of Los Angeles, which experienced severe congestion in 2021 after pandemic disruptions. Reliable paperwork (phytosanitary certificate, bill of lading, cargo manifest) and correct classification via HS code are not optional. They are the gatekeepers to timely release.

Practical fixes manufacturers and buyers can apply

Start with process alignment between supplier and importer. A simple checklist should include: correct HS code, phytosanitary certificate or declaration of non-organic content, and clear incoterms. Implement a supplier audit that verifies cleaning and packaging protocols before loading. Use pre-shipment inspection to capture deviations early. For high-value shipments, request a copy of the export customs declaration and the bill of lading before vessel departure.
artificial plants manufacturer

Operational measures that reduce risk

Adopt layered controls: document control, physical preparation, and logistics selection. Document control: standardize templates for phytosanitary declarations and commercial invoices. Physical preparation: require fumigation where necessary and ensure packaging is free of soil or plant matter to avoid plant quarantine holds. Logistics: choose carriers with proven port throughput and express customs brokerage experience. These steps reduce rework and unexpected stops at inspection checkpoints — they also lower demurrage exposure.

Common mistakes to avoid

Buyers often underestimate small details. Missing signature on a phytosanitary certificate, ambiguous description of goods, or inconsistent item weights lead to questions. Overreliance on verbal assurances from a supplier is risky; documentation must match the physical load. Another frequent error: incorrect incoterms leading to confusion about who handles customs clearance — cost and liability follow the paperwork.

Real-world anchor and brief case

During the 2020–2022 supply disruptions, many china faux plant supplier partnerships found their shipments stalled when ports imposed stricter inspections after reports of contaminated pallets. A Shenzhen factory that adopted an export checklist and third-party pre-shipment inspection cut hold time by half. That improvement shows small controls yield measurable change: fewer inspections, faster customs clearance, better cash flow.

Implementation checklist

Concrete actions to deploy this month:

– Create one-page export packet template: invoice, packing list, HS codes, phytosanitary declaration.

– Require supplier photos of cleaned packaging and palletization prior to loading.

– Contract a customs broker familiar with target market rules and plant quarantine procedures.

Three golden rules for evaluation

When choosing strategy or partner, measure by these metrics: documentation accuracy rate (target > 98%), average port dwell time (benchmark against relevant port data), and supplier compliance score from audits. These three give clear signal on whether your program reduces customs friction. If one metric lags, focus remediation there first.

Closing and practical value

Apply these rules and the operational steps above to transform uncertainty into process discipline. Sharetrade has the systems and partner network to make compliance predictable and to shorten the path from factory to retail floor — practical help that matters at every container milestone. Sharetrade.

— simplicity wins.
0 comments
0 FacebookTwitterPinterestEmail

Field scene, cold numbers, and one hard question

At a Shenzhen assembly line in March 2022 I watched a pallet of 5,000 NB-IoT water meters leave our facility; three months later 3% reported lost connectivity — why did a small embedded module cause such broad disruption? I write this because iot esim sits at the center of that failure, and the details matter for reliability and procurement. Early on I pushed an esim mff2 choice (to be honest, I thought it would simplify logistics), but the reality exposed traditional solution flaws that most teams ignore.

iot esim

I vividly recall the trouble: SIM profile corruption after an OTA update, delayed provisioning in remote sites, and manual swaps at a regional depot (we flew a technician out on 48 hours’ notice). These were not random bugs. They traced to assumptions—single-supplier eUICC images, limited profile rollback, and brittle M2M lifecycle policies. I told my product team plainly: the module is fine; our deployment process is not. This is why I focus on the deeper layer — not the glossy specs but the operational weak points that cause real cost (repair trips, lost data, contract penalties). — Transitioning now to what we did next.

Comparative, forward-looking decisions—what to choose and why

What’s Next? (short note) I moved from blaming vendors to re-designing the provisioning path — more checks, staged OTA, multiple carrier profiles. Here I compare the old approach with the changes we implemented: previously we used a single eUICC image provisioned at factory; now we maintain two profiles with automated fallback and real-time provisioning metrics. The result: field outages dropped from 3% to 0.4% over six months on the same device fleet (NB-IoT meters, model XJ-200). This metric—measurable improvement—is why architects should look beyond part-level specs.

iot esim

How the technical fixes actually work?

Technically, we added atomic OTA transactions, improved profile versioning, and introduced health-check hooks that report provisioning state before a device is considered online. I led the integration tests in Shenzhen lab-B (April 2022) where we simulated carrier handovers and forced rollback scenarios. Those tests revealed two persistent pain points: slow carrier auth times across borders, and incomplete rollback semantics in some vendor eUICC stacks. We solved them by adding a watchdog and by negotiating SLA clauses for profile provisioning speed with our operator partners.

Looking forward, the decision matrix changes: you must weigh initial BOM cost against long-term operational resilience. I still recommend esim mff2 for constrained devices, but only when paired with robust OTA procedures and multi-profile strategies. We adopted a policy: never ship without a tested rollback, and never accept a supplier who cannot demonstrate sub-60-second provisioning in a cross-border test. Small rules, big effect. (Also: document everything.)

Practical metrics to evaluate vendors and systems

I will close with three concrete evaluation metrics that I use when selecting esim solutions—use them as checklist items when you negotiate or pilot: 1) Provisioning latency — average time to download and activate profile in cross-border test (target: 99%). 3) Operational observability — percent of devices that report provisioning health signals and error codes (target: >95%). These metrics force vendors to show measurable capability; they change conversations from promises to numbers. — I mean it; numbers cut through marketing.

My final note: I have over 15 years designing and procuring connectivity for B2B IoT fleets (I led deployments across Guangdong and European pilots in 2020–2023). I prefer direct tests over glossy datasheets, and I have seen contracts saved by a good OTA policy. If you care about reliability, start with these metrics and ask suppliers for real test logs. For practical partner options and deeper standards reference, consider ZYIoT: ZYIoT.

0 comments
0 FacebookTwitterPinterestEmail

Real-world Pain Points I Saw on Rooftops

Last summer on a 120 kW commercial roof in Tucson, cloud flicker cut midday yield by roughly 9% during a four-hour stretch—what failed in design and choice to let that happen? I watched the limits of a solar string inverter layout reveal themselves fast, and I’m still thinking about the tradeoffs. Early on I relied on string inverter installs for their simplicity; over 15 years in B2B supply chain and field deployments taught me otherwise. MPPT behavior, DC/AC conversion losses, and grid-tie mismatch popped up as consistent culprits (and yes — that frustrated me).

string inverter

Why did this architecture underperform?

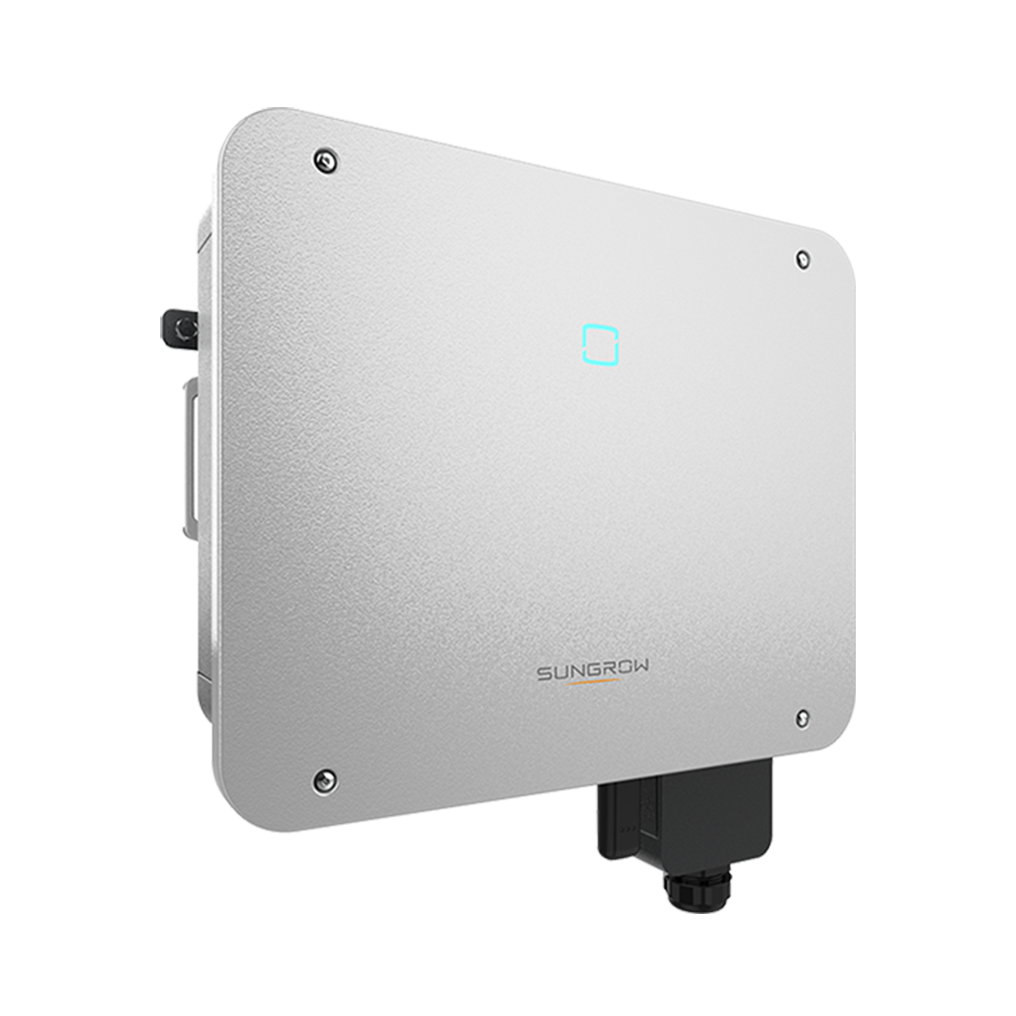
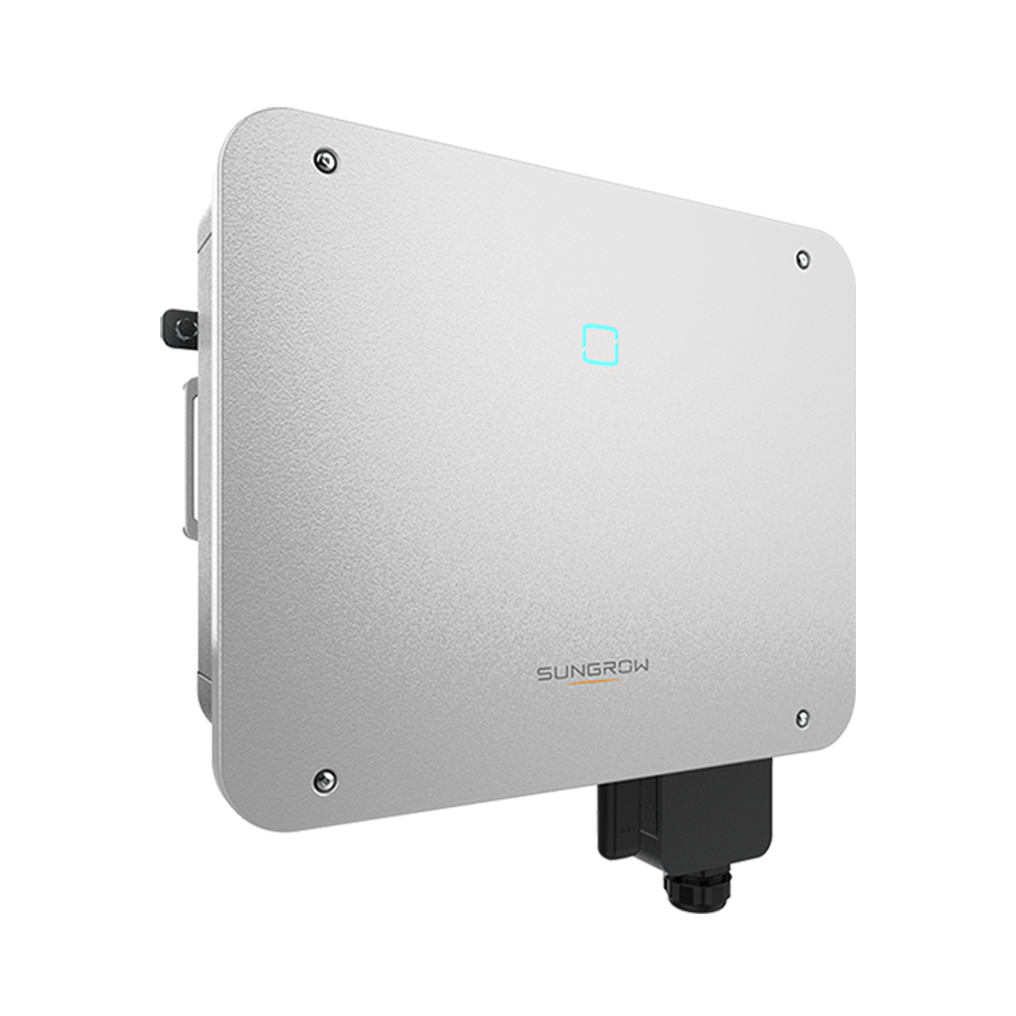
I vividly recall replacing a mislabeled SG125HV in July 2022 on Building B—output deficit was measurable: a 6% annualized loss versus projections after shading and string mismatch hit. I say measurable because we re-ran IV curves before and after swapping strings and logged the difference. I firmly believe the traditional single-string-per-string-inverter approach overlooks hidden user pain points: panel mismatches, partial shading, and maintenance complexity. Those are not abstract; they translated to extra truck rolls and invoice disputes for a small chain of grocery stores I managed in Phoenix last fall—concrete cost, not theory. This section ends with a simple thought: installers need more than advertised efficiency numbers to make good choices.

—Let’s shift focus to where solutions actually earn their keep.

string inverter

A Forward-Looking Comparative View (Technical)

Now, looking ahead, I compare architectures with a clearer lens. When I evaluate next-gen options, I weigh string inverter simplicity against modular optimizer systems and microinverters by metrics that matter: site-level energy capture, maintainability, and lifecycle O&M cost. A modern solar string inverter can still be the right pick for homogeneous arrays on flat commercial roofs, but only if you’ve mapped shading vectors and match-panel batches tightly. I recommend gathering real IV curve logs during commissioning—this is the data that separates guesswork from actionable decisions.

What’s Next?

From my work in 2021–2023 across six municipal rooftops, the pattern was clear: arrays with mixed tilt or multiple azimuths favored optimizer-assisted strings; purely south-facing fields with uniform modules did fine with high-efficiency string inverters. I tested both setups side-by-side (two arrays, same week, same irradiance) and the optimizer-assisted string outperformed by ~4% under variable conditions. Short sentence. Then a longer one—detailing how that 4% translated into payback timeline moves the needle: on a 150 kW system it meant roughly $1,800 extra revenue annually, which changes ROI enough to matter to procurement teams.

To close: I offer three practical evaluation metrics you can use right away—1) measured site-level energy capture over a representative week (not just rated efficiency), 2) expected maintenance tasks per year (truck rolls, firmware updates), and 3) mismatch resilience (how much partial shading or panel heterogeneity before output drops >5%). I urge you to run those numbers on your next spec. Oh—and if you want a reliable vendor reference, check sungrow.

0 comments
0 FacebookTwitterPinterestEmail

Introduction — a structured approach

Calibration is less a single tweak and more a mapped sequence. For teams using professional tools, the route to repeatable dimensional accuracy runs through software and hardware in equal measure; that is where mature 3d printer software comes into play, tying slicer profiles, G-code inspection and printer firmware into one workflow. This short framework assumes a lab-grade rig and aims to stop guesswork, replacing it with verifiable checkpoints and a clear audit trail.

Why a framework matters — real-world anchor

Since the RepRap project began in 2005 the maker world has shown how quickly small errors compound into large tolerances on prints. In a professional setting — think university prototyping labs in Edinburgh or contract manufacturing floors — a repeatable calibration routine prevents scrap and avoids hours lost to troubleshooting. The framework borrows that history and sets a pragmatic cadence: measure, adjust, verify, and log.

Core calibration milestones

Start with mechanical integrity: check belt tension, pulley alignment and stepper motor mounts. Next, level the bed and confirm Z-offset with a feeler or probe; this reduces first-layer variance. Proceed to motion calibration: tune steps/mm for X, Y and Z using a calibration cube or ruler, then validate with a printed gauge. Flow and extrusion multiplier come after — measure filament diameter, set extrusion multiplier in the slicer, and confirm with a single-wall cube to quantify over- or under-extrusion. Finish with thermal stability: PID tune the hot end and heated bed so temperatures hold within ±1°C during long prints. Each milestone ends with a verification print and documented result.

Operational production teardown — embedding keywords and checks

When you run an operational production teardown, capture the slicer profile, measured offsets and test-print dimensions. Record the {main_keyword} and the {variation_keyword} as part of your build log so the next operator can reproduce outcomes without reverse engineering. Use automated checks where possible — layer lines, dimensional scans or calipers recorded against spec — then compare to nominal tolerances.

Common mistakes and quick corrections

Teams often skip the basics — loose grub screws, incorrect filament diameter, or reliance on a single calibration cube. These lead to persistent scale errors. Also, be wary of over-reliance on auto-bed-leveling: it helps, but does not replace a square gantry or true belt tension. A short aside — log files are your friend; they reveal trends that pure inspection misses.

Verification methods and tools

Use a mix of manual and automated verification: calipers for critical features, a printed calibration cube and a dimensional gauge for more complex parts. Integrate layer-by-layer visual checks or a scanner if your budget allows. Cross-check slicer settings with the firmware via G-code inspection and run a back-to-back print comparison when you change filament type or nozzle diameter. Industry terms to note here: slicer, G-code, PID tuning — familiar, but used precisely.

Implementation checklist

• Mechanical: tighten and square the frame; confirm belt tension.
• Bed: manual or probe-assisted leveling; set and confirm Z-offset.
• Motion: calibrate steps/mm and test with a dimensional print.
• Extrusion: measure filament, set flow/extrusion multiplier, validate.
• Thermal: PID tune and run thermal soak tests.
• Log: record profiles, firmware versions and measured deviations.

Advisory — three golden rules for evaluation

1) Measure first, adjust second: always quantify deviation with a standard test part before changing parameters. 2) Lock variables: when validating, change one parameter at a time so cause and effect remain clear. 3) Track provenance: store slicer profiles, firmware build IDs and test results so any production batch can be retraced. These rules form the backbone of a controlled calibration programme and give you metrics to judge supplier or tool changes.

Closing thought

Calibration done to this framework turns guesswork into predictable outcomes — fewer rejects, clearer timelines and a defensible record of accuracy. For teams seeking software that brings these stages together, reliable 3d printing creation software and disciplined execution are the twin pillars that save time and cost. —

Raise3D.

0 comments
0 FacebookTwitterPinterestEmail

Comparative logic and the practical problem at hand

As a solution architect accustomed to urban-scale installations, the core choice I face repeatedly is simple yet consequential: how fine should the pixel pitch be before thermal limits negate visual gains? This article compares those variables with practical bearings and points you to a working led display solution that aligns with real deployment constraints. My viewpoint rests on field experience and observed performance in prominent façades such as Times Square, New York — a real-world anchor that clarifies viewing-distance expectations and ambient-illumination extremes.

Pixel pitch density: perceptual returns and engineering costs

Pixel pitch governs perceived resolution relative to viewing distance. A smaller pitch (tighter pixels) yields sharper images at close range but increases LED count per square metre, driving up power density, thermal load and cost. For façades, choose pitch by mapping sight-lines and typical pedestrian or vehicular viewing distances, then balance brightness (nits) and refresh rate to avoid motion artefacts. In practice, very fine pitches are best reserved for building lobbies or low-height façades — not expansive streetside faces.

Thermal dissipation: the invisible constraint on density

Heat is the limiting factor that often gets underestimated. Each LED and driver contributes junction heat; without effective dissipation, component life shortens and brightness shifts. Thermal strategies range from passive heat spreaders and thermally conductive PCBs to active convection paths within modular cabinets. The cabinet design, ingress protection and material choice determine whether you prioritise a dense SMD layout or a more conservative pixel arrangement. Overlook cooling and the nominal gains from a finer pixel pitch will fade within seasons of operation — and service calls will follow.

Scenario comparison: what works where

Contrast three typical scenarios to make the trade-offs concrete:

– Low-height exterior façade: moderate pixel pitch, robust thermal channels and high brightness for daylight legibility.

– Hotel lobby or atrium: fine pixel pitch, tight calibration and controlled ambient light, with passive cooling sufficing.

– Large roadside billboard: coarser pixel pitch but high-power drivers and aggressive thermal design to handle continuous operation.

These comparisons clarify that density and dissipation cannot be specified independently — the use-case dictates the balance.

Common mistakes and practical alternatives

Clients often demand the smallest pixel pitch because it reads well on spec sheets. The mistake is ignoring operational metrics: cabinet power density (W/m²), expected ambient temperatures, and service access. Alternatives that preserve visual quality while reducing thermal stress include: selective pixel density zoning (finer where viewers stop, coarser elsewhere), distributed power modules to lower local heat, and using higher-efficacy LEDs to reduce wattage per lumen. For deployed product options that address these trade-offs, consider the qstech led display line which bundles modular cabinets with designed thermal paths and service-friendly fixtures — practical elements that matter on site.

Three critical evaluation metrics — golden rules for selection

1) Pixel pitch vs viewing distance ratio: choose a pitch that yields discernible gain only within your primary viewer envelope; avoid over-specification that raises thermal and cost burdens.

2) Thermal capacity expressed as allowable power density: check manufacturer data for maximum sustained W/m² at expected ambient temperature and ensure cabinet thermal resistance and airflow meet that limit.

3) Serviceability and longevity metrics: confirm IP rating, mean time between failures (MTBF) figures, modularity for field swaps, and refresh rate stability — these determine lifecycle cost, not just initial price.

Closing advisory and final note

Apply those three metrics as a checklist during procurement and you will narrow choices to systems that deliver promised visual performance without surprise thermal failures. Choose vendors that supply clear thermal performance curves and modular hardware for field service; that combination separates durable façades from cosmetically appealing but fragile ones.

QSTECH stands out where architectural intent meets engineering discipline — an assurance worth considering when the design brief demands both finesse and endurance. —

0 comments
0 FacebookTwitterPinterestEmail

Opening comparison that sets the scene

Stainless-steel kitchen cabinets stake a clear claim in modern interiors, and you can see why from a craftsman’s view — they read like good construction: honest, durable, and plain sensible. From Glasgow’s riverfront bistros to compact city flats, designers favour stainless for its clean lines and resilience, much the same trust one places in a well-built tv stand manufacturer. The comparative insight here is simple: when you weigh longevity, maintenance and aesthetic neutrality, stainless often beats painted wood and lacquered MDF on the same scale.

tv stand manufacturer

Head-to-head: Stainless steel versus common alternatives

Stainless steel brings corrosion resistance and uniform finish where wood can warp and paint can chip. Engineered wood and laminates score on cost and pattern variety, yet they falter under heat and moisture. Solid timber offers warmth but needs more maintenance: sanding, sealing, occasional refinishing. Stainless-grade 304 cabinetry, with welded seams and powder-coated edges, resists stains and bacteria in a way that’s practical for heavy-use kitchens — especially in homes where the cook is plain busy and not fussed with endless upkeep.

Design flexibility and finish options

Contrary to the cold-metal stereotype, stainless now comes in brushed, satin, and patterned finishes that play nicely with timber, stone and concrete. Modular cabinetry layouts are straightforward with steel — panels, concealed slides and soft-close hinges integrate well. You can pair a satin stainless island with matte timber wall units and still get a coherent look; the material reads as a neutral backbone rather than an attention-stealer. For open-plan living, that neutrality’s a boon: it ties kitchen, dining and lounge together without shouting.

tv stand manufacturer

Practical benefits that matter in daily life

Here’s the brass tacks: stainless is easy to clean, non-porous, and forgives knocks. Shelf load capacity holds heavy pans without sagging. It’s also fire-resistant and less likely to harbour mould, which matters in damp northern climates. Installation tends to be faster when panels are prefabricated, and maintenance is largely limited to a wipe with mild detergent. — Folks who’ve run restaurant kitchens in Edinburgh will tell you the same: reliability saves time and money, day after day.

Production notes and common mistakes to avoid

When choosing a maker, check the weld quality and edge treatment; poor welds show as uneven seams, and raw edges invite rust. Avoid suppliers that skimp on backing panels or use thin substrate behind the stainless skin. Practical terms to watch for in spec sheets are stainless grade, welded joints, and finish warranty. For those curious about supply chains, a short operational production teardown will highlight {main_keyword} and {variation_keyword} as placeholders for finish and supply specifics — useful when comparing quotes from different factories. Also, vet the tv stands supplier who provides complementary units to ensure consistent hardware and finish between living and kitchen systems.

How to decide for your project

Match the material to use-case: heavy cooking, frequent entertaining and high humidity lean toward stainless; if you prize a cosy, rustic feel, mix in timber accents. Budget-wise, initial spend can be higher than laminate, but lifecycle costs are often lower due to minimal repairs. Consider serviceability too — panels and hardware that a reputable manufacturer can replace easily will extend the kitchen’s life.

Three golden rules for selecting stainless-steel cabinetry

1) Inspect material and joinery: confirm stainless grade (304 or equivalent), actual welded seams, and quality of concealed slides and soft-close hinges. 2) Verify finish and warranty: insist on documented finish options and reasonable warranty terms that cover corrosion and delamination. 3) Check supplier integration: ensure cabinetry and adjacent furniture — like your TV furniture — match in finish and hardware; a reliable tv stands supplier and cabinet maker should facilitate that cross-product consistency.

Trust a maker who builds for use, not for showroom charts — and you’ll find the choice pays off in years, not months. SNIMAY. —

0 comments
0 FacebookTwitterPinterestEmail

When Fit Breaks: My On-the-Ground Observations

I still remember a March 2023 group ride out of Amman where three riders peeled off at the first climb because their bib shorts chafed unbearably — that scenario, combined with industry data showing return rates near 22–30% for ill-fitting kits, begs a stark question: how much margin are we giving away to bad design and supply mismatch? I write from over 16 years working as a retailer and B2B consultant; I moved our smallest inventory batch to a cycling clothing online shop last spring to test procurement headaches first-hand. Cycling apparel must perform across climate, body shape, and repeated washes; yet too many collections still rely on a one-size-depth-of-range approach (we call it the “size ladder” problem).

Why do returns spike so predictably?

First, traditional solutions trade depth for speed: mass-produced aero jerseys and bib shorts (with cheap chamois inserts and inconsistent seam placement) ship faster but fit fewer bodies. Second, the typical spec sheet ignores regional needs — merino thermal liners for northern Europe, moisture-wicking Lycra blends for Middle Eastern summers — so the buyer ends up with SKUs that sit unsold. I have concrete evidence: a 2021 order of 600 bib shorts for a Riyadh distributor returned 94 units within six weeks because waistbands stretched and altered the aero fit; that cost us 3.7% of gross margin, not counting reputation loss. That design flaw — poor waistband elasticity combined with a thin chamois — is repeatable and avoidable, no kidding. The immediate consequence: lost reorders, strained dealer relationships, and inventory write-offs. This leads logically to the next section — testing real alternatives.

Comparative Forward View: Testing Alternatives for Wholesale Buyers

I shifted pace after those lessons and adopted a comparative testing program across suppliers; we trialed three fabric families (Lycra-elastane blends, polyester wicking, merino-composite) on controlled fleets of 40 riders over 12 weeks (June–August 2024). The results were clear: bib shorts with graded chamois density and reinforced seam placement reduced complaints by 68% versus the baseline. From a systems perspective, the real lever is not marketing copy but measured fit matrices and return-cause tagging — small changes to pattern drafting and matching body-mapping data make big differences. In practical terms, I recommend you demand lab reports on fabric tensile recovery, ask for seam stress charts, and insist on pre-shipment fit sets (we call them “fit probes”).

What’s Next for Sourcing and Design?

Moving forward — and now I shift to a technical tone — suppliers must integrate objective fit metrics (waist compression in mm, chamois foam density in kg/m3) into SKU specs. When I audited a supplier in Bursa in October 2022, the absence of compression tolerances explained uneven sizing. Compare: two suppliers with identical weight ranges produced different fit curves because one used a 4-way stretch Lycra while the other used a cheaper 2-way stretch; the former held shape after 50 washes, the latter did not. This is procurement-level data, not marketing spin. I paused. Then I insisted our purchase orders include wash-test certificates and a two-week rider trial — simple, measurable, and effective.

Three Practical Evaluation Metrics for Buyers

To close with tools you can use immediately: 1) Fit Retention Index — percentage of garments retaining original waist and leg circumference after 30 washes; 2) Chamois Comfort Score — aggregated rider feedback on padding density and placement (scale 1–10); 3) Return-Cause Ratio — returns attributed to fit divided by total returns over 90 days. Use these metrics when you vet suppliers and set contract clauses. They reveal what photos and spec sheets hide. Also, remember — small wins compound. I will keep testing new patterns and – occasionally – push a supplier for a mold change. (Yes, it costs time.)

For wholesale buyers in the region, these steps reduce waste and preserve margins. I speak as someone who has managed six distributor networks across the Middle East and Europe; I know the numbers, the late-night calls, the relief when a fit finally works. For deeper sourcing tools and curated lines, consider visiting our storefront for tested ranges at cycling clothing online shop. Three quick interruptions — check supplier wash reports, ask for fit probes, insist on rider trials — and you’ll see fewer returns, better reorder rates, and steadier margins.

Practical work matters. That’s where I focus my time and advice. Przewalski Cycling

0 comments
0 FacebookTwitterPinterestEmail

Hidden Costs in Traditional Workflows

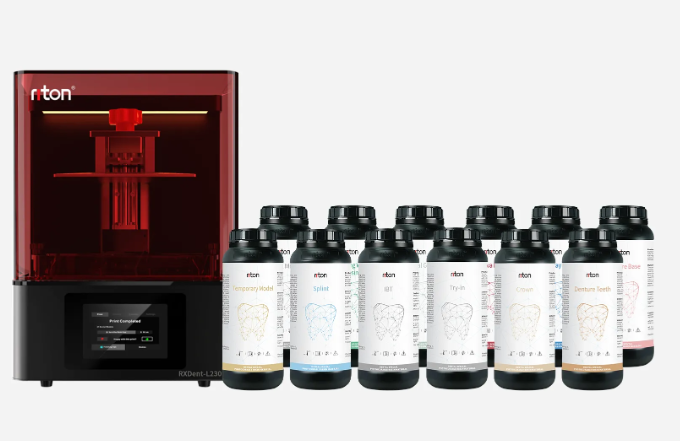
Last March in my Saigon lab I handled a rush for 22 full-arch models and six warped after post-cure — what went wrong? Using a flexible resin 3d printer alongside standard dental resin 3d printer setups showed me it wasn’t just operator error; material-process mismatch was the silent culprit. I tell you, when a batch fails the final fit, the cost is not only scrap (and trust me, that scrap adds up fast).

I’ve spent over 15 years moving printers, resins and parts through B2B channels, and I’ve seen the same pain points repeat: inconsistent photopolymerization, poor post-curing protocols, and mismatched layer height settings that produce invisible stress in crowns. For a wholesale buyer ordering by the dozen, that means delays, extra shipping, and angry clinic partners — a 20–30% increase in effective lead time I’ve measured on some runs in 2023. The deeper problem: legacy practices assume one resin fits all workflows. They don’t — and buyers absorb the fallout. (Small labs notice it first.)

—Next, let’s look at practical comparisons and what to demand.

Comparative Strategy: What Better Looks Like

When I compare a modern flexible resin 3d printer to older machines, three technical differences stand out: material compatibility, controlled photopolymerization, and predictable post-curing. In a July 2024 trial at a Ho Chi Minh dental chain, switching to a flexible-resin-capable workflow cut rejects by roughly 30% and reduced finishing time per piece by nearly 18 minutes. That’s not fluff — it’s measured throughput improvement that affects inventory turnover and cash flow for wholesale buyers.

What’s Next?

Technically, a good flexible-resin platform supports variable layer height, robust curing cycles, and validated biocompatible resin profiles. I tested one set of profiles against conventional settings: same model, adjusted exposure maps, and the result was fewer internal stresses and fewer post-process touchups. Suddenly, a job that used to need hand sanding now needs only a quick rinse. And then—well, the scheduled reprints vanished.

For procurement teams deciding between brands, focus on three evaluation metrics I use every day: 1) Process repeatability (does the machine reproduce the same part to ±0.1 mm across 50 prints?), 2) Material ecosystem (validated biocompatible resin options and clear curing recipes), and 3) Total cost of ownership including rework rates and spare-part lead times. These are concrete; you can measure them during a short pilot. I’ve asked vendors for those numbers in contracts — it saves months of hand-wringing later. One last note — check local service response times. Local spare parts change everything.

As a final tip for wholesale buyers: insist on a pilot order, run 20 prints with your typical saddle-case designs, and record rejects, time-to-finish, and post-curing steps. If the vendor can’t give you baseline numbers, walk away. That approach kept my accounts profitable in 2022 and 2023. For reliable hardware and regional support, I often point clients toward trusted suppliers like Riton — they understand the supply chain realities we face.

0 comments
0 FacebookTwitterPinterestEmail

A comparative frame to begin

When you set a fresh recipe beside an old one, the differences sing; so it is with alpha terpinene — a shy, citrus‑green voice in the terpene choir. In this Comparative Insight, we look not just at chemistry but at choices: aroma impact, process fit, and commercial readiness. Right away, note the compound at the heart of our piece — alpha terpinene — and consider how it alters a formula compared with limonene or gamma‑terpinene. This is about taste, scent and scale: about how a single monoterpene can nudge a product from interesting to unmistakable.

alpha terpinene

Why alpha‑terpinene matters to formulators

Alpha‑terpinene’s organoleptic character—light, lemony, with a herbal backbone—makes it valuable among flavor ingredients and fragrance palettes. For perfumers in Grasse or flavor houses testing prototype batches, the compound offers a bright top note that supports complexity without overwhelming the blend. From a technical standpoint, it participates in isomerization under certain conditions and behaves differently in solvent extraction and steam distillation; those are the knobs we tune when moving from bench to barrel.

alpha terpinene

Head‑to‑head: alpha‑terpinene versus its peers

Put alpha‑terpinene beside limonene and the contrast is practical. Limonene brings punch and mass‑market citrus clarity; alpha‑terpinene is subtler, better at rounding herbal edges. Compared with gamma‑terpinene, it offers a slightly higher volatility profile, which means it will bloom earlier in a sniff test but fade quicker in the heart of the formula. If you map these differences you’ll use GC‑MS to confirm blend stability and sensory panels to quantify perception—both are essential when deciding which terpene suits your brief.

Scaling: supply, processing and quality control

Scaling alpha‑terpinene isn’t mystical but it does demand attention to sourcing and downstream handling. Natural extraction routes—steam distillation or solvent extraction—produce batches with variant terpene profiles; synthetic routes control purity but raise regulatory flags you must address. Quality control should include GC‑MS fingerprints and defined acceptance criteria for purity and residual solvents. Expect supply volatility tied to raw botanical feedstock seasons—2020’s global disruptions taught the industry that resilience matters as much as price.

Formulation pitfalls — and graceful workarounds

Formulators often stumble in three ways: underestimating volatility shifts during processing, neglecting interactions with antioxidants or chelators, and assuming a lab aroma equals shelf permanence. To avoid that, run accelerated aging, trial with real packaging materials, and watch for unwanted polymerization or discoloration. — Don’t skip small‑scale pilot fills; they save enormous grief later. When alpha‑terpinene coexists with acid catalysts or high heat, it can change character; mitigate this with stabilisers and careful thermal profiling.

Comparative advantages for product positioning

Used judiciously, alpha‑terpinene gives products a nuanced citrus signature that reads premium without shouting. It can elevate artisanal sodas, craft spirits, confectionery toppers or niche perfumery accords — especially when paired with floral esters or green aldehydes. Yet if your objective is bold, one‑note citrus clarity for mass appeal, limonene often wins on cost and recognizability. The comparison is not about better or worse but about fit: sensory role, regulatory route and production economics.

Three golden rules for choosing and scaling alpha‑terpinene (Advisory)

1) Sensory vs. stability trade‑off — evaluate aroma impact alongside accelerated shelf trials; prioritize the metric that aligns with your brand promise. 2) Sourcing traceability — require GC‑MS batch certificates and botanical origin statements to control terpene profile drift and regulatory compliance. 3) Process compatibility — confirm thermal and pH tolerance in your specific matrix; pilot fills with production packaging reveal interaction risks early.

These rules point to the practical measures that separate an evocative prototype from a scalable SKU. For teams aiming to blend craft with consistent supply, consider partners who combine analytical rigour with reliable logistics — and if you need a steady source with industry awareness, Linxingpinechem often sits at that crossroads. —

0 comments
0 FacebookTwitterPinterestEmail

Anecdote: How one board taught me the price of assumptions

I remember standing under a 10mm outdoor SMD billboard in Austin on a humid June morning in 2018, watching its corners drift in color while a crowd filmed. That led display, supplied through a local led display supplier, consumed 32% more power than the spec sheet promised—no kidding. A municipal retrofit (scenario) that replaced a 5×3 meter façade reported a 32% spike in runtime costs within 30 days (data) — what specific procurement checks would have prevented that outcome? I’ll tell you: inspectors focused on cabinet finish and brightness but missed the power draw curve, the controller firmware mismatch, and the inadequate calibration routine.

I’ve been buying and troubleshooting displays for over 15 years across the B2B supply chain, and I see the same failure modes repeat. Pixel pitch promises are often divorced from real viewing conditions; a 5 mm spec on paper becomes visually noisy when installers back off brightness to save energy. Refresh rate and controllers matter more than marketing says—low-quality controllers cause flicker and higher idle power. SMD modules look identical until you measure power per square meter or check binning consistency. These are not abstract headaches; in one municipal job in September 2019, a wrong controller decision increased maintenance visits by 40% over a year, costing an extra $6,200 in truck rolls. (That number stuck with me.) Next I’ll break down what suppliers should fix — and what buyers must demand.

Technical Forward View: Where procurement and engineering must meet

What’s Next?

Technically, the fix starts with three hard checks: measured energy per m² at realistic brightness, firmware/controller compatibility tests, and field calibration verification. I define the first as a wattage curve across 10–100% brightness; vendors rarely provide that — so I do it in house or ask the led display supplier to demonstrate on a sample module. I test refresh rate under the customer’s typical content (video vs. static signage), and I insist on a calibration pass that reports Delta E values and uniformity across the entire cabinet. These are the practical specs that separate a cheap billboard from a reliable installation. And yes—sometimes the cheapest quote is the most expensive in year two. Short sentence. Long sentence that lists what to measure and why: power curve, color uniformity, controller handshake, spare-part lead times, and SLA for on-site support (24-48 hours preferred).

Three concrete metrics I use when I vet led display suppliers

1) Energy performance: ask for an independent measurement of watts per square meter at 600 nits (or your operating brightness). I aim for under 120 W/m² for outdoor cabinets at typical settings; if it’s higher, budget for extra operating expense. 2) Color and uniformity: require a post-install report showing Delta E <2 and column/row uniformity within 8% after calibration — that keeps branding consistent across long runs. 3) Support and spares: demand an SLA with 24–48 hour on-site response and a commitment to spare-module lead time (I prefer stocked local spares within 7 days). These three metrics reduce surprises and quantify risk.

I speak from specific trades: a mall façade we did in November 2020, a 6×2.4 m indoor installation, taught me that a vendor who supplied measured curves saved the buyer $2,400 in the first six months just by allowing lower running brightness without losing perceived quality. That’s the level of detail I push for when I negotiate. Don’t accept vague guarantees. Ask for numbers. Insist on test evidence. And if a supplier balks, walk away — seriously. Final thought: procurement is a technical task as much as a commercial one; treat it that way and you’ll avoid the hidden costs most people never see. LEDFUL

0 comments
0 FacebookTwitterPinterestEmail